Ammonium bicarbonate, a white crystalline powder widely used in industrial and agricultural applications, requires efficient and reliable material handling solutions for safe and effective transportation. Pneumatic conveying technology offers a sophisticated method to transport this chemical, addressing challenges such as dust control, material handling, and process integration. This article explores the principles, practical applications, and emerging trends in ammonium bicarbonate pneumatic conveying systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. from China.
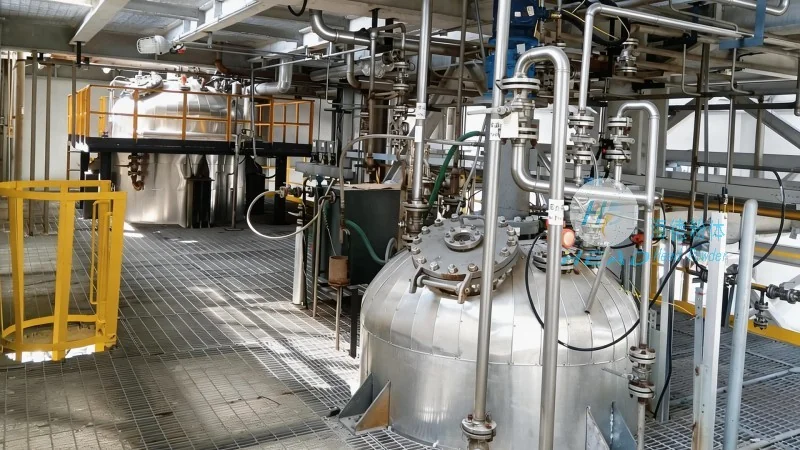
The core principle of pneumatic conveying involves the use of air or gas to transport solid materials through a pipeline system. For ammonium bicarbonate, which is a fine powder with specific physical properties, the system design must consider factors like particle size, density, and moisture content to ensure optimal performance. There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use high air velocities to suspend particles in the air stream, suitable for short-distance and low-pressure applications. Dense-phase systems, on the other hand, operate at lower velocities, allowing for more controlled and efficient transport, especially for sensitive materials like ammonium bicarbonate. The choice between these systems depends on the specific requirements of the process, including distance, material characteristics, and desired handling efficiency.
A typical ammonium bicarbonate pneumatic conveying system consists of several critical components that work in tandem to ensure smooth operation. These include a material feeder, which accurately controls the flow of the powder into the system; a conveying line, which transports the material from the source to the destination; a separator, which separates the material from the air stream at the receiving end; and a dust collector, which captures any residual particles to prevent environmental contamination. The system design also incorporates pressure vessels, air compressors, and control valves to regulate the air flow and pressure, ensuring consistent and reliable transport. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of ammonium bicarbonate handling, ensuring optimal performance and safety.
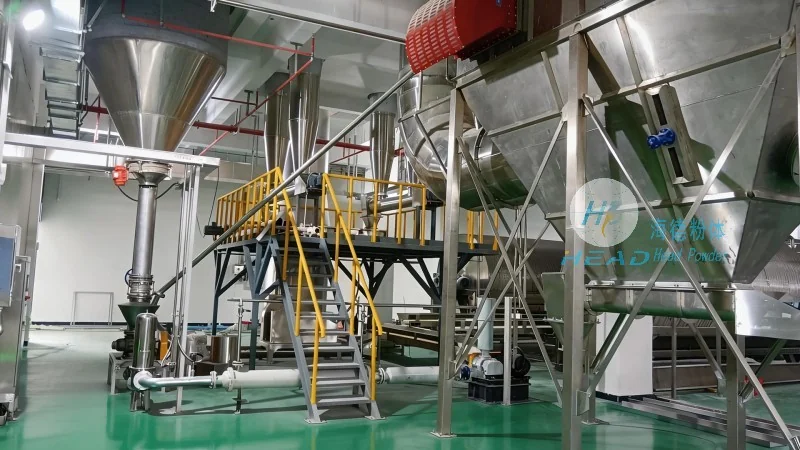
Ammonium bicarbonate pneumatic conveying systems find extensive applications across various industries, including chemical manufacturing, food processing, and agricultural production. In the chemical industry, these systems are used for transporting ammonium bicarbonate from storage silos to production lines, ensuring a continuous and controlled supply of raw material. The food industry utilizes pneumatic conveying for transporting ammonium bicarbonate in food processing facilities, where hygiene and material purity are paramount. In agriculture, the technology is employed for distributing ammonium bicarbonate as a fertilizer, enabling precise and efficient application to fields. The versatility of pneumatic conveying allows it to adapt to different operational conditions, making it a preferred choice for handling ammonium bicarbonate in diverse industrial and agricultural settings.
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages for handling ammonium bicarbonate. One of the key benefits is the ability to transport the material in a closed system, which minimizes dust exposure and prevents contamination, ensuring product purity and worker safety. The system also provides flexibility in terms of layout and integration, allowing for easy adaptation to existing production facilities. Additionally, pneumatic conveying can handle varying material flow rates and distances, making it suitable for both small-scale and large-scale operations. The energy efficiency of modern pneumatic conveying systems, combined with reduced maintenance requirements, further enhances their appeal as a cost-effective solution for ammonium bicarbonate handling.
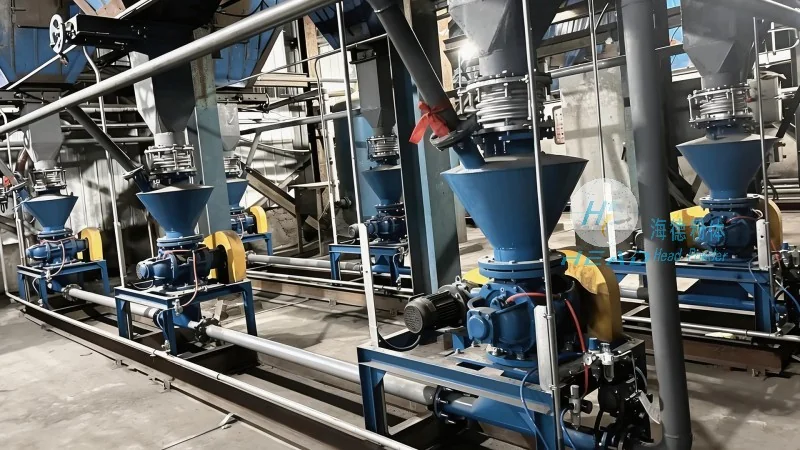
The field of ammonium bicarbonate pneumatic conveying is continuously evolving, driven by advancements in technology and increasing demand for efficient material handling solutions. One of the emerging trends is the integration of automation and control systems, which enhance the system's performance and reliability. Modern systems now feature advanced sensors and control panels that monitor key parameters such as pressure, flow rate, and material level, allowing for real-time adjustments and process optimization. Another trend is the adoption of energy-efficient air compressors and variable frequency drives, which reduce operational costs and environmental impact. Additionally, the development of new materials and coatings for conveying components, such as corrosion-resistant alloys and anti-static surfaces, improves the system's durability and longevity. Shandong HeadPowder Engineering Co., Ltd. stays at the forefront of these technological advancements, offering innovative solutions that meet the evolving needs of the ammonium bicarbonate industry.
Ammonium bicarbonate pneumatic conveying technology represents a reliable and efficient solution for handling this critical chemical, offering numerous benefits over traditional methods. The principles and components of these systems are designed to ensure safe, clean, and effective transport, while the emerging trends and innovations continue to enhance their performance and adaptability. As the demand for ammonium bicarbonate grows in various industries, the importance of advanced material handling solutions becomes increasingly significant. Shandong HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, plays a vital role in providing customized pneumatic conveying systems that meet the specific requirements of the ammonium bicarbonate market, contributing to the overall efficiency and sustainability of industrial and agricultural operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top