HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for handling borax materials. This article provides an in-depth exploration of the working principle and key features of such systems, highlighting their efficiency and reliability in industrial applications.
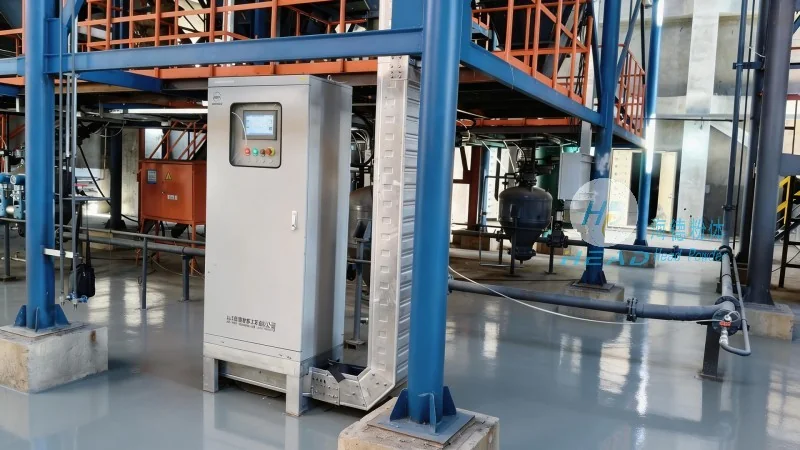
The core of a borax material pneumatic conveying system lies in its ability to transport bulk materials like borax through a pressurized or vacuum environment using air or other gases. The system typically consists of several key components, including a material hopper, a rotary feeder, a conveying pipeline, a dust separator, and a receiver. The process begins when borax is fed into the hopper from a storage silo. The rotary feeder then regulates the flow of material into the conveying pipeline, ensuring a consistent and controlled feed rate. As the material enters the pipeline, it is entrained by high-velocity air, which carries the particles through the system. The conveying pipeline may include bends, expansions, or contractions to navigate the path from the feeder to the receiver. At the receiving end, a dust separator or cyclone separates the borax from the air stream, allowing the material to be deposited into the target container while the air is filtered and recycled back into the system. This closed-loop operation minimizes material loss and ensures a clean, efficient transfer process.
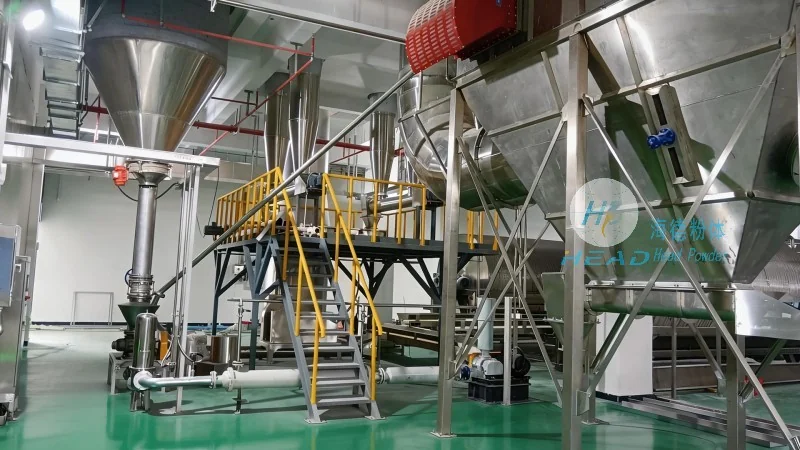
Borax material pneumatic conveying systems offer several distinct advantages that make them ideal for industrial applications. Firstly, they provide a dust-free and hygienic method of material handling, which is crucial for maintaining product quality and compliance with industry standards. Unlike traditional belt or bucket elevators, pneumatic systems eliminate the need for physical contact with the material, reducing the risk of contamination and ensuring a clean transfer process. Secondly, these systems offer high efficiency and flexibility in terms of material transport. They can handle a wide range of particle sizes and densities, making them suitable for various borax products, from fine powders to granules. The ability to adjust the air pressure and flow rate allows for precise control over the conveying speed, ensuring optimal performance under different operational conditions. Thirdly, the closed-loop design of the system enhances energy efficiency by recycling the air used for conveying. This reduces energy consumption and operating costs compared to open systems that require continuous air intake from the environment. Additionally, the system's compact design saves valuable floor space in industrial facilities, making it a practical solution for plants with limited space. Finally, the reliability and durability of the components, such as the rotary feeder and the conveying pipeline, ensure long-term operation with minimal maintenance requirements, contributing to overall cost savings and operational stability.
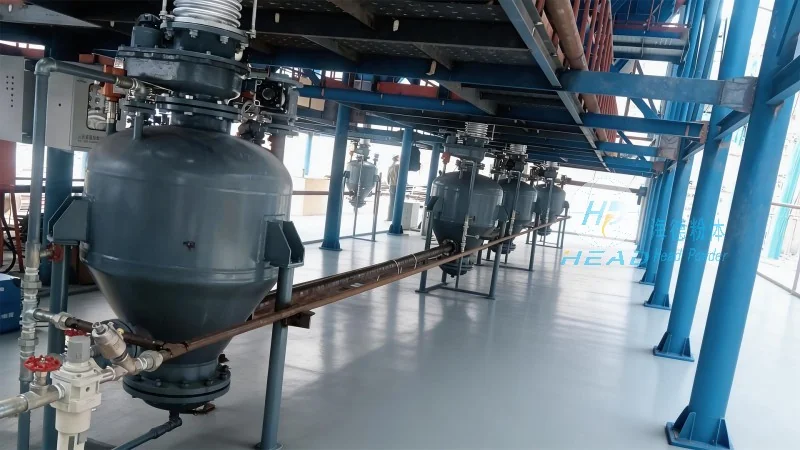
Borax material pneumatic conveying systems are widely used in various industries, including chemical manufacturing, food processing, and pharmaceuticals. In the chemical industry, they are essential for transporting borax used in the production of detergents, glass, and other industrial chemicals. The systems ensure that the material is handled safely and efficiently, preventing dust explosions and maintaining product purity. In food processing, the dust-free nature of the system is critical for maintaining food safety standards, as borax is often used as a food additive. The ability to handle fine powders without contamination makes it suitable for applications where product quality is paramount. In the pharmaceutical industry, the hygienic design of the system meets stringent regulatory requirements, ensuring that borax is transferred without any risk of cross-contamination. The benefits of these systems extend beyond just material handling, as they also contribute to improved workplace safety by eliminating manual handling of bulk materials and reducing the risk of accidents. Overall, the use of pneumatic conveying systems for borax materials enhances operational efficiency, reduces costs, and improves product quality, making it a preferred choice for modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top