For industrial operations dealing with bulk materials, efficient and reliable material handling systems are crucial. Among the various technologies available, gravity dust removal material handling equipment stands out as a cost-effective solution for transporting and cleaning particulate materials. This article explores the fundamental aspects of such equipment, focusing on its design principles and operational benefits, with insights from Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
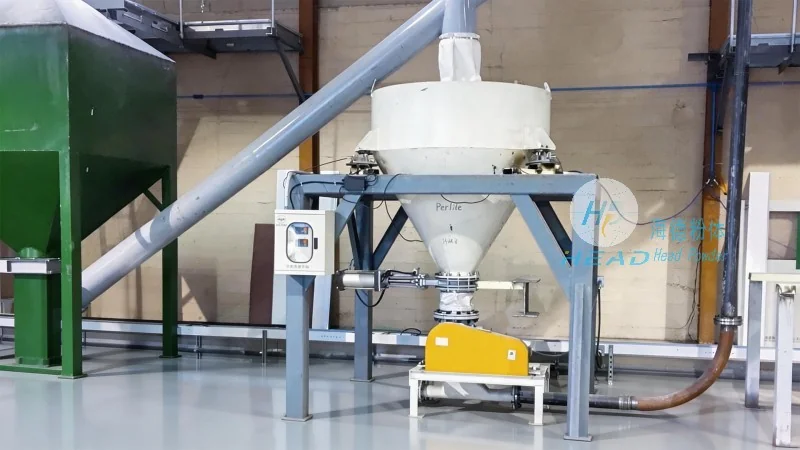
Gravity dust removal material handling equipment, often referred to as gravity feeders or pneumatic conveyors with dust filtration, is a system designed to transport dry bulk materials while simultaneously removing airborne dust and particulates. The primary goal is to ensure safe and clean material transfer, especially in industries like mining, construction, and chemical processing where dust control is a regulatory and safety priority. These systems typically integrate material transport with dust collection, making them an integral part of modern industrial processes.
The core components of a gravity dust removal system include a hopper for material storage, a conveyor or duct system for transporting material, and a dust filtration unit to capture and remove airborne particles. The hopper is designed to hold the bulk material, allowing it to flow under gravity into the conveyor. The conveyor may be a screw, belt, or pneumatic system, depending on the material characteristics and required transport distance. The dust filtration unit, often equipped with bag filters or cartridge filters, captures fine particles before releasing clean air back into the environment.
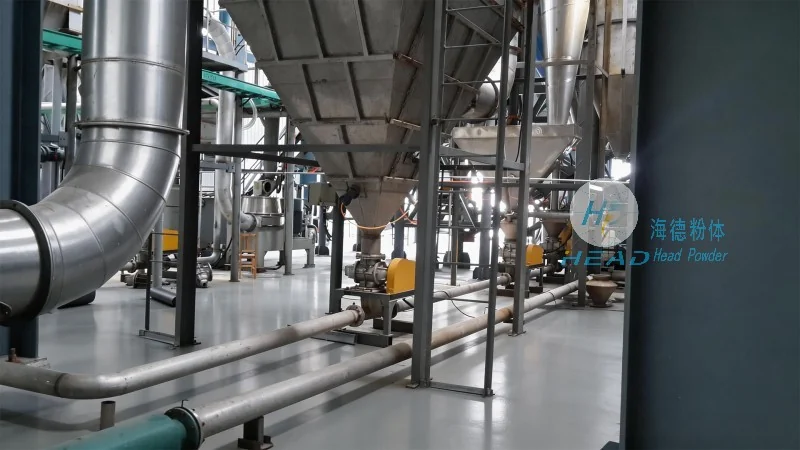
The design of gravity dust removal equipment is guided by several key principles to ensure optimal performance and efficiency. First, the system must maintain a consistent material flow rate, which is achieved through proper hopper design and material feeding mechanisms. The hopper's shape and size are critical; a conical or wedge-shaped hopper promotes uniform material flow and reduces the risk of blockages. Second, the conveyor system must be sized appropriately to handle the material's bulk density and flow characteristics. This includes selecting the right type of conveyor (e.g., screw, belt) and ensuring adequate slope or air pressure for pneumatic systems.
Third, the dust filtration unit is designed to meet specific air filtration requirements, typically based on the material's dust emission rate and regulatory standards. The filtration media, such as high-efficiency particulate air (HEPA) filters or fabric filters, is chosen to capture particles down to micrometer sizes, ensuring compliance with environmental and occupational health regulations. The system's design also considers energy efficiency, with features like variable speed drives and optimized airflow to minimize power consumption.
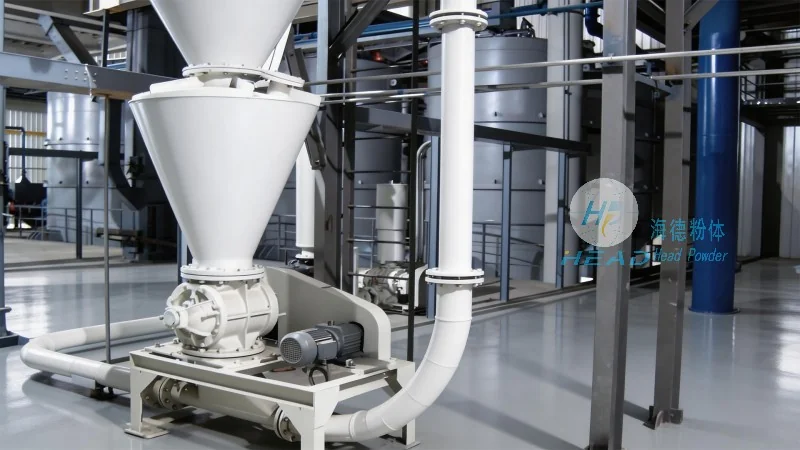
Gravity dust removal material handling equipment offers several advantages in industrial settings. It provides a clean and dust-free material transport process, reducing the risk of respiratory illnesses among workers and minimizing environmental contamination. The system is also relatively low-cost compared to other material handling solutions, making it an attractive option for small to medium-sized operations. Additionally, its simplicity in design and operation reduces maintenance requirements and downtime.
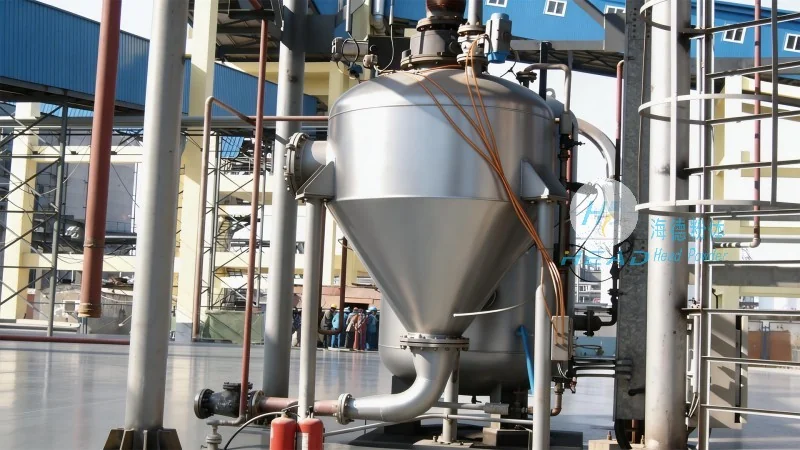
These systems are widely used in industries such as cement production, where raw materials are transported and processed with minimal dust generation. In the mining sector, gravity feeders are employed to move crushed ore and waste materials from storage bins to processing plants. Chemical and pharmaceutical industries also benefit from these systems, as they handle powders and granules while maintaining strict cleanliness standards.
Gravity dust removal material handling equipment is a sophisticated yet practical solution for bulk material transport and dust control. By integrating material handling with dust filtration, these systems enhance operational efficiency, ensure compliance with environmental regulations, and improve workplace safety. The design principles, including proper hopper design, efficient conveyor systems, and effective dust filtration, are crucial for achieving optimal performance. As industrial processes continue to evolve, the demand for such equipment is likely to grow, driven by the need for sustainable and efficient material handling solutions. Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of such advanced systems, providing tailored solutions to meet the diverse needs of industrial clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top