For industries dealing with rare earth powders, the efficient and reliable transportation of these materials is crucial. A rare earth powder conveying system is a specialized piece of equipment designed to handle the unique properties of rare earth powders, ensuring safe and effective movement from one point to another in industrial processes. This article explores the components and design principles of such systems, highlighting the importance of tailored solutions for handling these valuable materials.
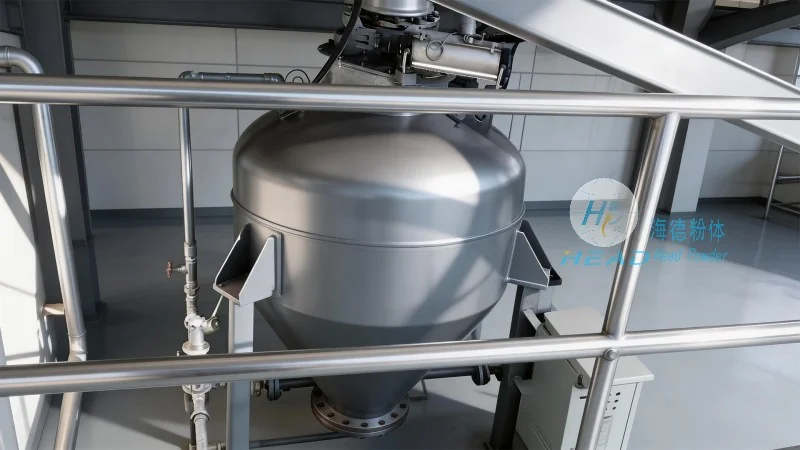
A rare earth powder conveying system is engineered to manage the flow of rare earth powders, which are often fine, abrasive, and can be sensitive to moisture or contamination. These systems are typically integrated into larger production lines, where they play a critical role in maintaining process efficiency and product quality. The system's design must account for the physical and chemical characteristics of rare earth powders, such as their particle size, density, and reactivity, to prevent issues like clogging, agglomeration, or material degradation during transport.
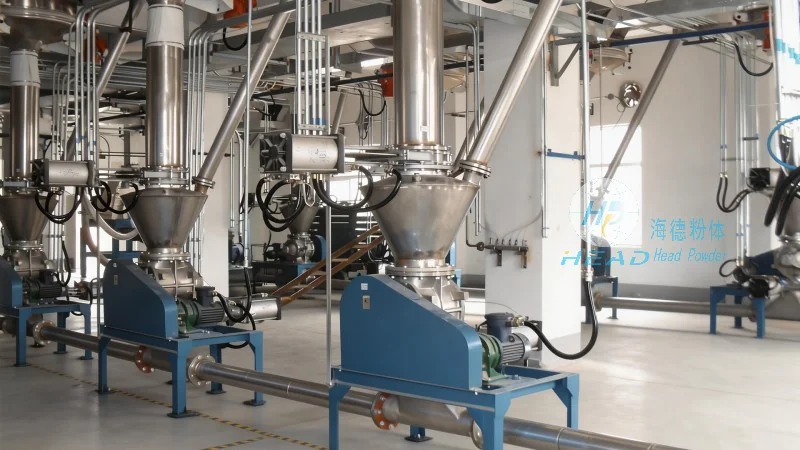
The core components of a rare earth powder conveying system include a hopper for material storage, a feeder to control the flow rate, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), and a control system to regulate operation. The hopper is designed to minimize material exposure to air and moisture, often with airtight seals and optional drying or dehumidification features. The feeder ensures a consistent and controlled discharge of powder, preventing overloading or underloading of the conveyor. The conveyor mechanism is selected based on the material's properties and the required transport distance. For example, screw conveyors are suitable for short distances and moderate flow rates, while pneumatic conveyors are ideal for longer distances and more delicate powders that require minimal mechanical contact.
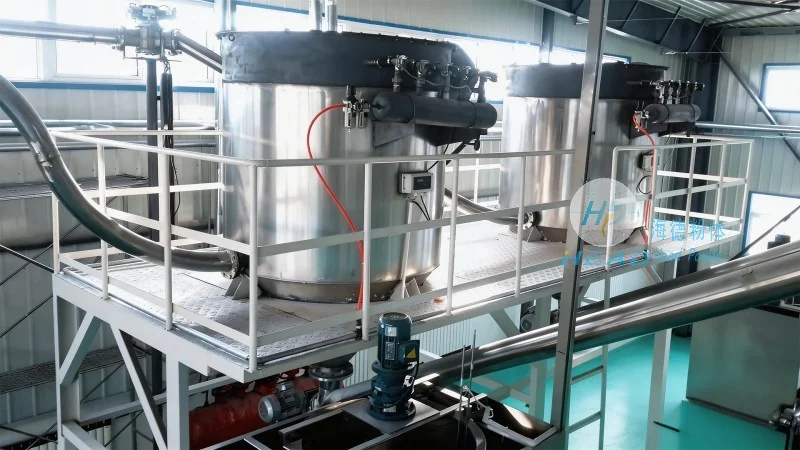
The design of a rare earth powder conveying system follows several key principles to ensure efficiency, safety, and durability. First, the system must minimize material degradation by reducing friction and impact during transport. This is achieved through smooth surfaces, gentle inclines, and low-speed operation where possible. Second, the system is designed to prevent clogging and blockages, which are common issues with fine powders. This involves using components with wide openings, anti-static features, and self-cleaning mechanisms. Third, the system is constructed from materials that are resistant to corrosion and wear, such as stainless steel or specialized alloys, to withstand the abrasive nature of rare earth powders. Additionally, the design incorporates safety features like overfill protection, emergency stop buttons, and monitoring systems to ensure safe operation and prevent accidents.
Given the diverse applications of rare earth powders in industries like electronics, magnets, and ceramics, rare earth powder conveying systems are often customized to meet specific process requirements. For instance, in the production of rare earth magnets, the system may need to handle powders with high magnetic properties, requiring specialized magnetic separation or shielding. In the ceramics industry, the system may need to transport powders with precise particle size distributions, necessitating adjustable feeders and fine-tuned conveyor speeds. The system's design also considers the scale of operation, from small laboratory-scale systems to large industrial-scale installations, ensuring scalability and adaptability.
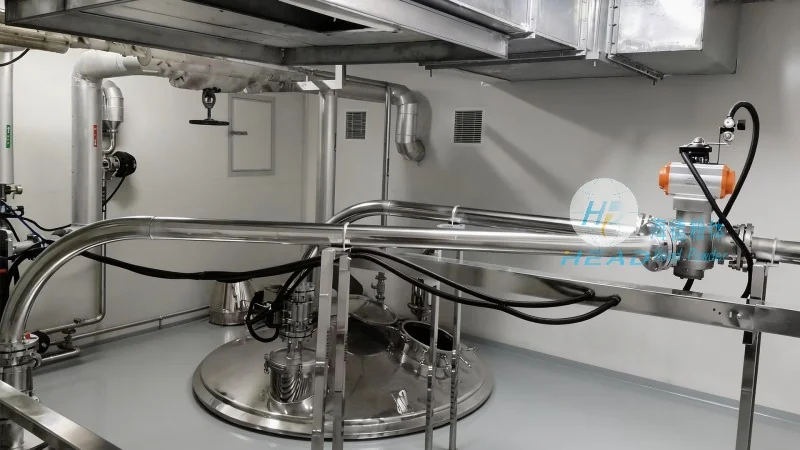
In conclusion, a rare earth powder conveying system is a critical component in the processing of rare earth materials, designed to handle their unique properties while ensuring efficient and safe transport. The design principles, including material selection, component integration, and safety features, are tailored to meet the specific needs of each application. For industries relying on rare earth powders, investing in a well-designed conveying system is essential for maintaining process efficiency, product quality, and operational safety. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing customized rare earth powder conveying systems that meet the highest standards of performance and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top