Bin pump powder handling equipment is a specialized industrial system designed for the efficient and reliable transport of bulk powders over long distances or vertical heights. This technology is widely used in various industries, including chemical, food, pharmaceutical, and mining, where the safe and precise movement of powders is critical. The bin pump, also known as a pressure-type pneumatic conveyor, operates by creating a pressure differential to move material from a storage bin to a discharge point. Understanding its design and functionality is essential for industries seeking to optimize their material handling processes.
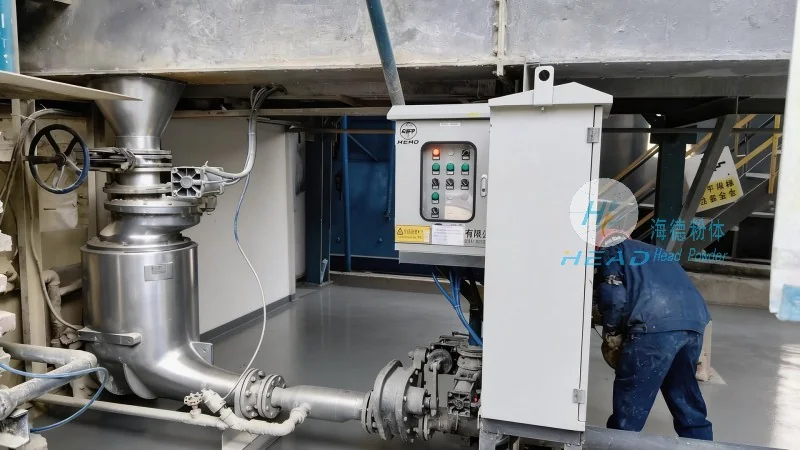
A bin pump is a type of pneumatic conveying system that uses compressed air or other gases to transport dry bulk materials. Unlike traditional vacuum or pressure conveyors, the bin pump operates under positive pressure, ensuring that the material is pushed through the system rather than pulled. The system typically consists of a hopper or storage bin, a pump unit, and a discharge outlet. The material is fed into the bin, and when the pump is activated, it creates a pressure that forces the powder to move through the pipeline to the desired location. This method is particularly effective for handling fine or cohesive powders that might be difficult to transport using other methods.
The bin pump system comprises several key components that work together to ensure efficient operation. The primary components include the storage bin or hopper, which holds the bulk material; the pump unit, which generates the pressure differential; the pipeline system, which conveys the material; and the discharge valve or outlet, which releases the material at the destination. The storage bin is usually equipped with a feeder or gate to control the flow of material into the pump. The pump unit may be a rotary lobe pump or a positive displacement pump, which is responsible for creating the pressure. The pipeline is typically made of stainless steel or other corrosion-resistant materials to handle various types of powders. The discharge outlet is designed to control the flow rate and prevent material buildup or blockages.
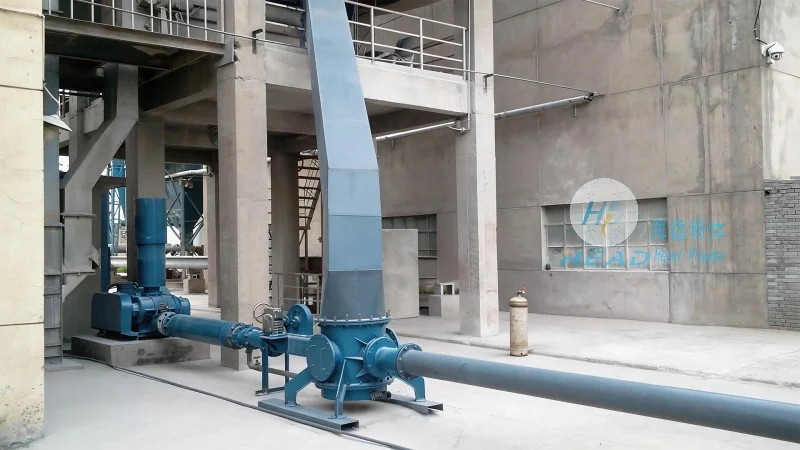
The design of a bin pump is based on fundamental principles of fluid dynamics and pressure control. The system operates by creating a pressure difference between the inlet and outlet of the pump. When the pump is activated, it draws material from the storage bin and forces it through the pipeline by increasing the pressure in the system. The pressure is maintained by the pump unit, which continuously moves the material forward. The operational mechanism involves several steps: first, the material is fed into the bin; second, the pump creates a pressure that pushes the material into the pipeline; third, the material travels through the pipeline to the discharge point; fourth, the material is released at the outlet. The system is typically controlled by a PLC (Programmable Logic Controller) or other automation equipment to ensure precise control over the flow rate and pressure. The design also considers factors such as material properties, pipeline length, and vertical height to ensure optimal performance.
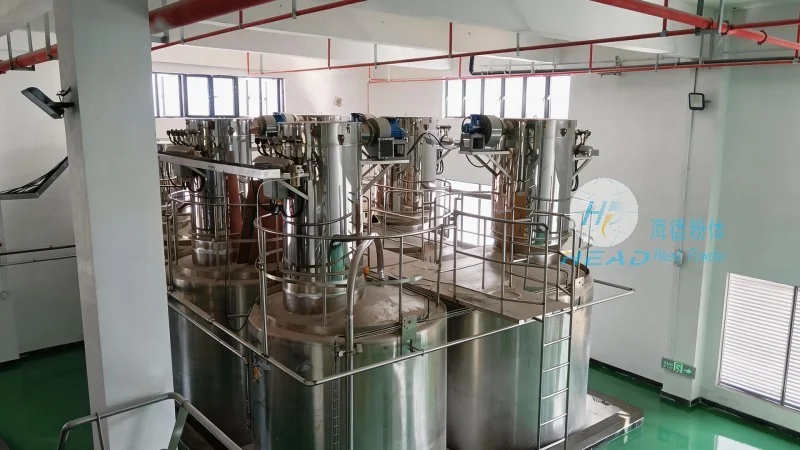
Bin pump technology offers several advantages over traditional material handling methods. One of the key benefits is its ability to transport powders over long distances or vertical heights without the need for multiple transfer points. This reduces the risk of material spillage and contamination, which is critical in industries such as food and pharmaceuticals. The positive pressure operation also prevents the ingress of air or moisture into the system, maintaining the quality of the material. Another advantage is the flexibility of the system, which can be easily modified to handle different types of powders or adjust the flow rate. The system is also relatively low maintenance, as it has fewer moving parts compared to other conveyor systems. Additionally, bin pumps can handle a wide range of material sizes and densities, making them suitable for various applications. The energy efficiency of the system is another advantage, as it uses less power compared to other methods of material transport.
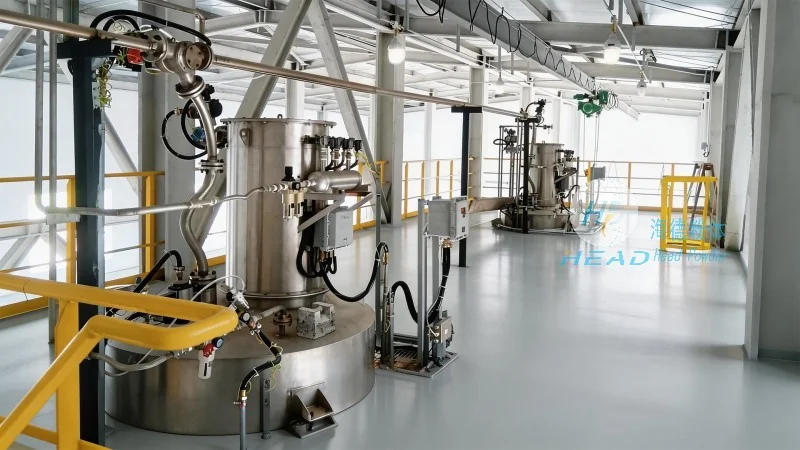
Bin pump powder handling equipment is used in a variety of industries and applications. In the chemical industry, it is used to transport raw materials such as powders and granules to processing units. In the food industry, it is used to transport ingredients such as flour, sugar, and spices to production lines. In the pharmaceutical industry, it is used to transport active ingredients and excipients to manufacturing facilities. In the mining industry, it is used to transport ore and other minerals from storage bins to processing plants. The system is also used in the agricultural industry to transport grain and other agricultural products. The bin pump is particularly useful in applications where the material needs to be transported over long distances or vertical heights, such as in large-scale industrial plants. The system is also used in applications where the material is sensitive to moisture or air, such as in the food and pharmaceutical industries.
Bin pump powder handling equipment is a reliable and efficient solution for the transport of bulk powders in various industries. The design and operational principles of the system ensure that it can handle a wide range of materials and applications. The system is also flexible and can be easily modified to meet the specific needs of different industries. The use of bin pump technology can help industries to optimize their material handling processes, reduce costs, and improve product quality. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of bin pump systems, provides high-quality and reliable equipment for various industries. With its expertise in the field, the company offers customized solutions to meet the specific needs of its clients. The company is committed to providing the best possible service and support to its customers, ensuring that they get the most out of their bin pump systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top