For agricultural and industrial operations dealing with corn, the efficient and reliable transport of this staple crop is crucial. A corn pneumatic conveying system offers a solution that minimizes manual labor, reduces handling time, and enhances overall productivity. This article explores what a corn pneumatic conveying system is and the fundamental design principles that make it effective.
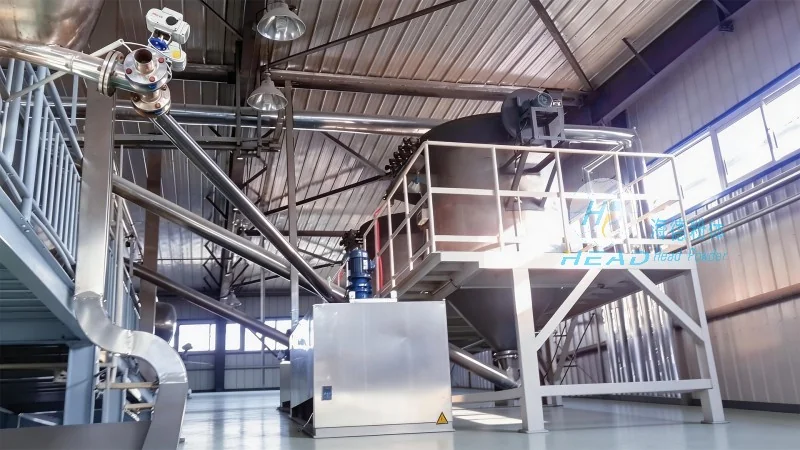
A corn pneumatic conveying system typically consists of several key components. The primary elements include a hopper or storage bin for corn storage, a conveying pipeline (usually made of metal or flexible tubing), a blower or air compressor to generate the air flow, and a discharge point where the corn is delivered. Some systems may also include a filter system to remove dust and debris from the air, ensuring a clean and safe operation. The hopper is designed to feed the corn into the system at a controlled rate, preventing blockages and maintaining consistent flow. The conveying pipeline is engineered to handle the specific characteristics of corn, such as its size, density, and moisture content, to ensure efficient transport. The blower provides the necessary air pressure to move the corn through the pipeline, while the discharge point allows for the controlled release of the material at the destination. In some advanced systems, additional components like a rotary valve or a surge bin may be included to regulate the flow and prevent backflow.
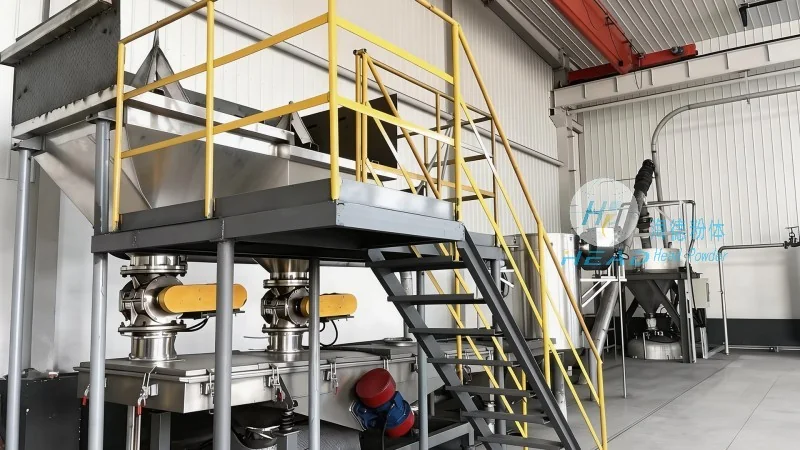
The design principles of a corn pneumatic conveying system are centered around the principles of fluidization and air flow dynamics. The system operates by creating a low-pressure zone in the conveying pipeline, which draws the corn particles into the air stream. This process, known as pneumatic transport, allows the corn to be moved through the system without direct contact with the pipeline walls, reducing wear and tear and minimizing product damage. The design of the hopper and feeding mechanism is critical to ensure a consistent and uniform flow of corn into the system. The hopper is often equipped with a gate or a rotary valve that controls the rate of corn discharge, preventing overloading or underloading of the conveying line. The blower's capacity and pressure are carefully selected based on the volume of corn to be transported and the length and diameter of the pipeline. The system's design also considers the corn's moisture content and particle size distribution, as these factors affect the air flow requirements and the risk of blockages. For example, wetter corn may require higher air pressure to maintain flow, while larger particles may need a larger pipeline diameter to prevent clogging. The discharge point is designed to handle the corn's characteristics, such as its density and flowability, to ensure a smooth and controlled release. In some systems, a surge bin or a buffer tank may be included to absorb fluctuations in the corn supply or demand, maintaining a steady flow to downstream processes.
Corn pneumatic conveying systems are widely used in various applications, from agricultural processing to industrial manufacturing. In agricultural settings, these systems are commonly used in corn storage facilities, grain elevators, and processing plants to transport corn from storage bins to processing equipment, such as mills or dryers. The systems are also used in feed mills to move corn from storage to mixing and packaging lines. In industrial applications, corn pneumatic conveying systems are employed in food processing plants, biofuel production facilities, and animal feed manufacturing operations. The benefits of using a corn pneumatic conveying system include increased efficiency, reduced labor costs, and improved product quality. By automating the transport process, the system minimizes the risk of human error and reduces the time required to move large quantities of corn. The pneumatic transport method also reduces product damage compared to traditional methods like bucket elevators or belt conveyors, which can cause bruising or cracking of the corn kernels. Additionally, the system can be easily integrated with other processing equipment, allowing for a seamless flow of materials from storage to processing. The design flexibility of corn pneumatic conveying systems allows them to be adapted to different production scales and operational requirements, making them suitable for both small-scale and large-scale operations.
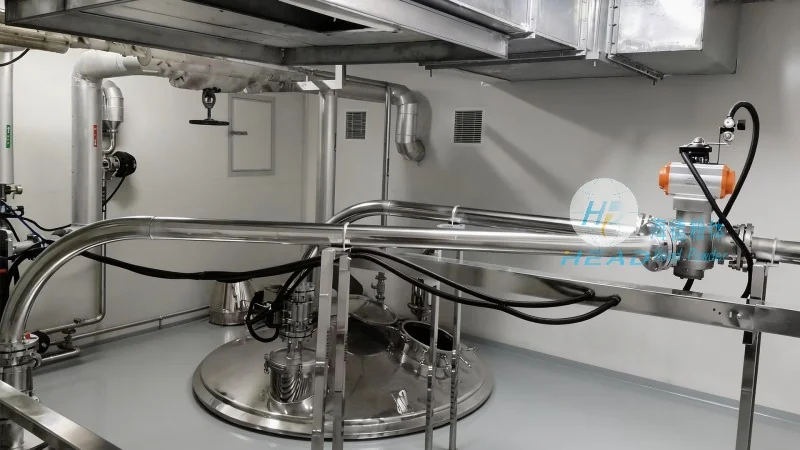
HeadPowder, a leading provider of engineering solutions for agricultural and industrial applications, specializes in the design, manufacturing, and installation of corn pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality, reliable systems that meet the specific needs of their clients. The company's headquarters is located in Shandong, China, where they have a team of skilled engineers and technicians dedicated to providing expert consultation and support. HeadPowder's systems are designed to be durable, efficient, and cost-effective, ensuring that clients can maximize their productivity while minimizing operational costs. The company's commitment to quality and customer satisfaction has made them a trusted partner for businesses in the corn processing industry. Whether you are a small-scale farmer or a large-scale industrial operation, HeadPowder offers tailored solutions to meet your corn transport needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top