HeadPowder, a leading engineering firm based in Shandong, China, specializes in advanced pneumatic conveying solutions tailored for the potash fertilizer industry. This article provides a comprehensive exploration of vacuum and positive pressure pneumatic conveying technologies, highlighting their operational principles, key advantages, and practical applications in the handling of potash fertilizers.
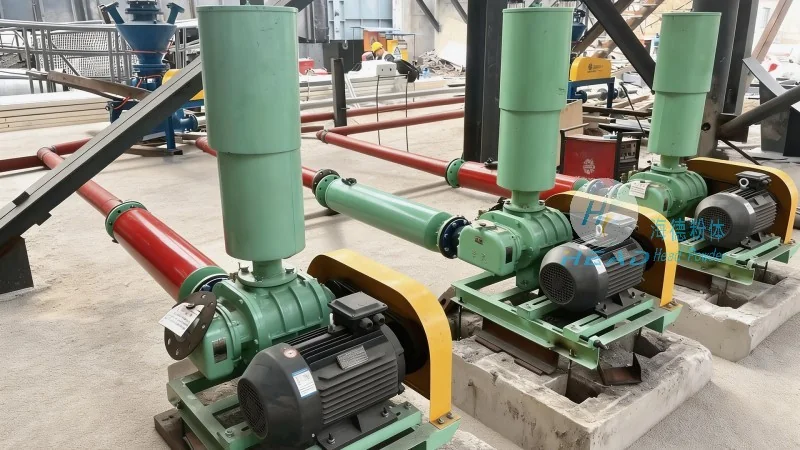
Potash fertilizers, such as potassium chloride (KCl) and potassium sulfate, are critical agricultural inputs that require efficient and reliable material handling to ensure optimal processing and distribution. Pneumatic conveying systems offer a non-contact, low-damage method for transporting these bulk materials, making them an ideal choice for modern fertilizer production facilities. The two primary types of pneumatic conveying systems—vacuum and positive pressure—each present distinct characteristics and operational capabilities that influence their suitability for specific potash fertilizer handling scenarios.
Vacuum pneumatic conveying systems operate by creating a negative pressure environment at the material inlet, drawing the potash fertilizer into the conveying line using a vacuum pump. This method is particularly effective for conveying materials from multiple source points or over relatively short distances, as it can handle powders with higher moisture content and finer particle sizes without significant degradation. The key components of a vacuum system include a vacuum pump, a filter unit to separate the material from the air, and a collection hopper. The system’s ability to handle powders with higher moisture levels makes it suitable for handling wet or sticky potash fertilizers, which can be challenging for other conveying methods.
One of the primary advantages of vacuum systems is their ability to handle materials from multiple source points, allowing for flexible material collection from silos, storage bins, or even outdoor stockpiles. This flexibility is crucial in fertilizer plants where materials may need to be sourced from various locations before processing. Additionally, vacuum systems are generally quieter and produce less dust compared to positive pressure systems, reducing operational noise and improving workplace safety. However, vacuum systems typically have a lower conveying capacity and are less effective over longer distances, as the pressure drop in the line can limit the efficiency of material transport.
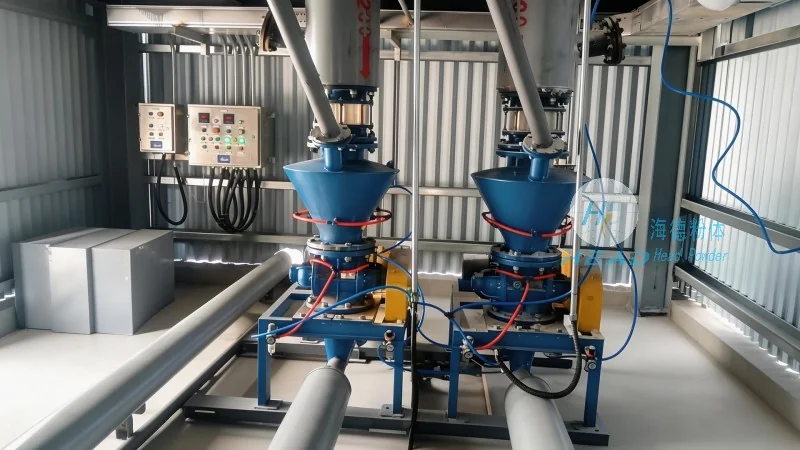
Positive pressure pneumatic conveying systems, in contrast, generate positive pressure at the material inlet using a blower or fan, pushing the potash fertilizer through the conveying line. This method is better suited for longer conveying distances and higher material throughput, as the positive pressure maintains a consistent flow of material through the system. The key components of a positive pressure system include a blower, a material feed hopper, and a filter unit at the discharge end. Positive pressure systems are particularly effective for handling dry, free-flowing potash fertilizers, as they can maintain a stable flow without the need for additional agitation or compaction.
A major benefit of positive pressure systems is their higher conveying capacity and ability to transport materials over longer distances without significant pressure loss. This makes them ideal for applications where the fertilizer needs to be moved from the production facility to storage silos or loading terminals. Additionally, positive pressure systems are more energy-efficient for long-distance transport, as the blower can maintain a consistent pressure throughout the line. However, positive pressure systems may generate more dust and noise compared to vacuum systems, and they are less effective for handling materials with higher moisture content or finer particle sizes, as the increased air velocity can cause material degradation.
When selecting a pneumatic conveying system for potash fertilizer handling, it is essential to consider the specific operational requirements of the facility. The choice between vacuum and positive pressure systems depends on factors such as the distance to be covered, the material characteristics (e.g., moisture content, particle size), the required conveying capacity, and the available space for system installation. Vacuum systems excel in applications requiring flexibility, low noise, and handling of wet or sticky materials, while positive pressure systems are preferred for high-capacity, long-distance transport of dry, free-flowing fertilizers.
For instance, a fertilizer plant that processes wet potash from multiple silos and needs to handle materials with higher moisture content would benefit from a vacuum system due to its ability to handle such materials without degradation. Conversely, a facility that needs to transport dry potash from the production line to a distant storage silo would likely opt for a positive pressure system to achieve higher capacity and longer transport distances. The selection process should also consider the initial investment costs and operational maintenance requirements, as both system types have distinct financial implications over their lifecycle.
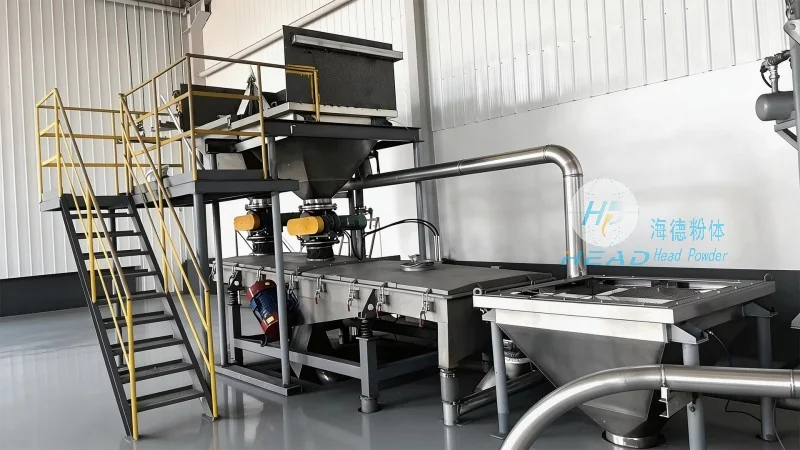
The application of pneumatic conveying systems in potash fertilizer handling varies based on the specific processing stages and operational needs. Vacuum systems are commonly used in the initial material collection phase, where raw potash is transferred from storage silos or outdoor stockpiles into processing hoppers. This stage often involves handling materials with higher moisture content and finer particle sizes, making vacuum systems the preferred choice due to their ability to maintain material integrity. Positive pressure systems, on the other hand, are widely used in the final stages of material transport, such as moving processed potash from the production line to storage silos or loading terminals, where higher capacity and longer distances are required.
HeadPowder, as a specialized engineering company, offers customized pneumatic conveying solutions tailored to the unique needs of potash fertilizer plants. Our expertise lies in designing systems that optimize material flow, minimize downtime, and enhance overall operational efficiency. By leveraging advanced engineering principles and industry best practices, we ensure that our clients receive systems that are not only effective but also cost-efficient and reliable. The implementation of these systems involves careful consideration of factors such as material properties, system layout, and operational constraints to achieve the best possible results.
Pneumatic conveying systems, both vacuum and positive pressure, play a vital role in the efficient handling of potash fertilizers. By understanding the operational principles and benefits of each system type, fertilizer producers can make informed decisions that enhance their processing capabilities and overall productivity. The choice between vacuum and positive pressure systems depends on specific operational requirements, but both offer significant advantages in terms of material integrity, operational flexibility, and efficiency. As the demand for potash fertilizers continues to grow, the adoption of advanced pneumatic conveying technologies will remain critical in ensuring that these essential agricultural inputs are handled safely and effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top