Efficient and reliable transport of raw materials is a critical factor in the cement production process. Among various methods, pneumatic conveying technology has emerged as a preferred solution for handling cement raw materials due to its advantages in terms of safety, hygiene, and operational flexibility. This article explores the application and optimization of pneumatic conveying systems in cement raw material transport design, highlighting key considerations and best practices.
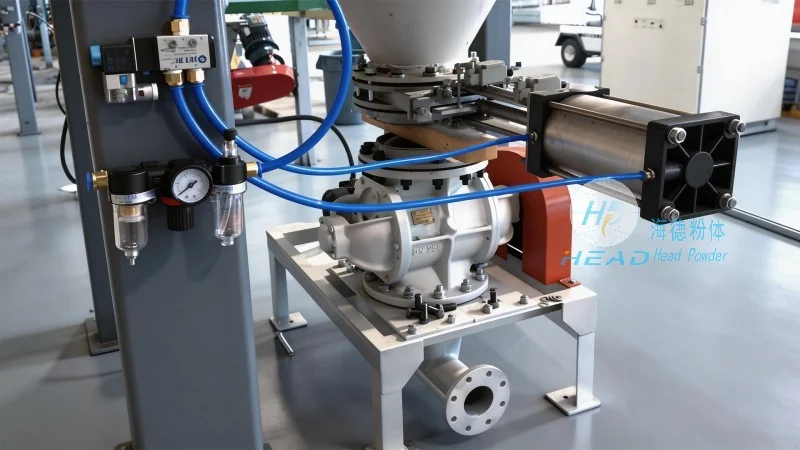
Pneumatic conveying, also known as air conveying, involves the transportation of bulk materials using a stream of air. This method can be categorized into two main types: dilute-phase and dense-phase conveying. Dilute-phase systems utilize low air-to-material ratios, making them suitable for long-distance and high-capacity transport. Dense-phase systems, on the other hand, use higher air-to-material ratios, which are ideal for handling sensitive or abrasive materials. The choice between these systems depends on the specific characteristics of the raw materials, such as particle size, moisture content, and flowability.
For cement plants, pneumatic conveying is widely used to transport raw materials from storage silos to the grinding mills. This technology ensures a continuous and controlled flow of materials, reducing the risk of blockages and improving overall plant efficiency. Additionally, pneumatic conveying systems can be integrated with other processing equipment, such as preheaters and kilns, to streamline the production process. The technology is particularly beneficial for transporting materials that are prone to dust and contamination, as it maintains a closed system that prevents environmental pollution.
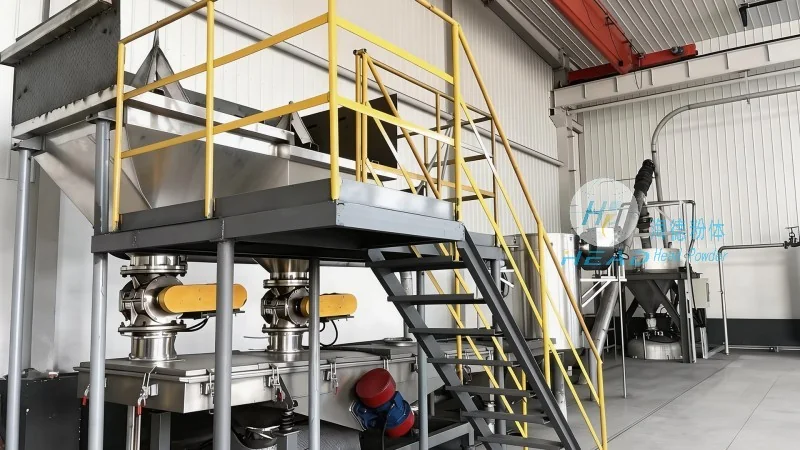
Optimizing pneumatic conveying systems is essential to maximize performance and minimize operational costs. Several strategies can be employed to achieve this goal. First, proper material selection and preparation are crucial. Ensuring that raw materials are properly dried and screened can improve their flowability and reduce the risk of system blockages. Second, system design and layout optimization play a significant role. Properly sizing the conveying lines, choosing the right type of airlocks and feeders, and ensuring adequate air pressure can enhance system efficiency. Third, regular maintenance and monitoring are necessary to detect and address issues promptly. Implementing advanced control systems and sensors can help in real-time monitoring of system performance and early detection of potential problems.
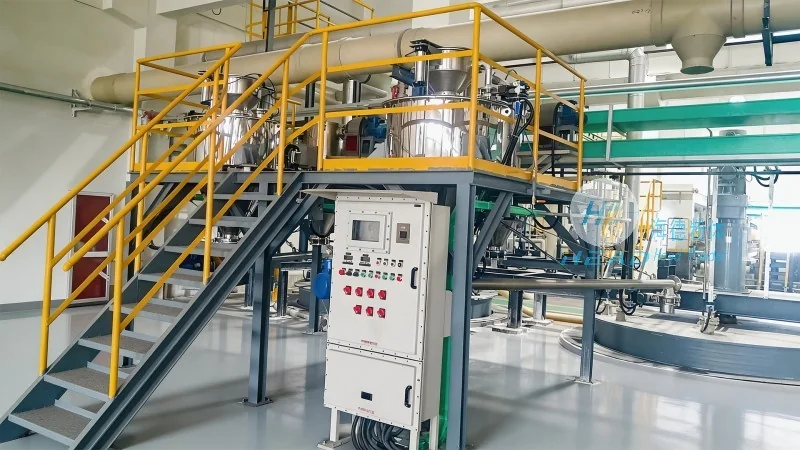
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in the cement industry, specializes in the design, installation, and optimization of pneumatic conveying systems. With years of experience and a team of skilled engineers, the company offers tailored solutions that meet the specific needs of cement plants. HeadPowder's expertise in material handling and process optimization ensures that their systems are not only efficient but also cost-effective and reliable. The company's commitment to quality and customer satisfaction has made it a trusted partner for many cement manufacturers in China and beyond.
In conclusion, pneumatic conveying technology offers significant benefits for the transport of cement raw materials. By understanding the principles of this technology and implementing optimization strategies, cement plants can enhance their operational efficiency, reduce costs, and improve product quality. Shandong HeadPowder Engineering Co., Ltd. stands ready to provide expert guidance and comprehensive solutions to help cement plants achieve their production goals through advanced pneumatic conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top