In the pharmaceutical industry, the selection of an appropriate material handling system is critical to maintaining product quality, ensuring operational efficiency, and adhering to stringent regulatory standards. Among the various technologies available, pneumatic conveying systems stand out as a preferred method for transporting powders and granules. Two primary approaches dominate this field: positive pressure conveying and negative pressure conveying. This article provides a detailed comparison of these two methods, highlighting their characteristics, advantages, and limitations, with a focus on their application in pharmaceutical manufacturing.
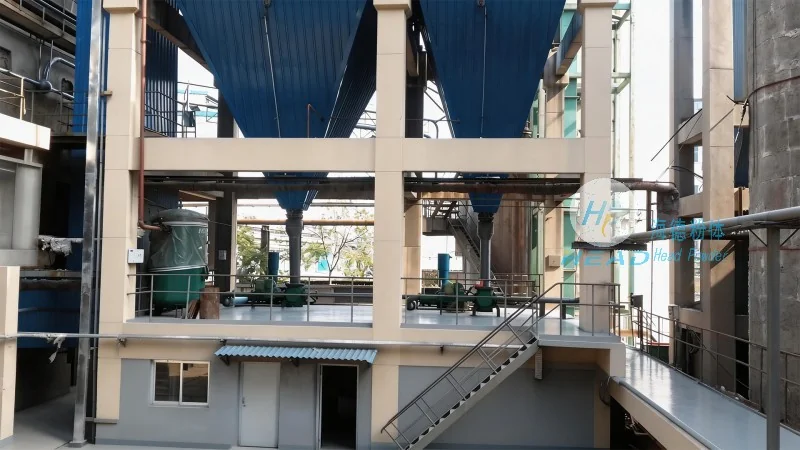
Pneumatic conveying systems utilize air or other gases to transport bulk materials through a pipeline. In pharmaceutical settings, these systems must meet high standards for cleanliness, containment, and product integrity. The choice between positive and negative pressure systems depends on factors such as the nature of the material being handled, the required level of containment, and the specific requirements of the manufacturing process.
Positive pressure conveying operates by maintaining a pressure within the system that is higher than the ambient environment. This pressure forces the material through the pipeline, ensuring that no external air enters the system. This feature makes positive pressure systems particularly suitable for handling materials that are hygroscopic (prone to moisture absorption), prone to caking, or sensitive to contamination from external air. The system's design typically includes sealed hoppers and ducts, which help prevent dust and particles from escaping into the surrounding environment.
One of the key advantages of positive pressure conveying is its ability to handle a wide range of materials, including fine powders and cohesive granules. The consistent pressure ensures smooth material flow, reducing the risk of blockages and improving overall system reliability. Additionally, positive pressure systems are often easier to integrate with existing production lines, as they can be connected directly to process equipment without the need for complex vacuum setups.
Conversely, negative pressure conveying maintains a pressure that is lower than the ambient environment. This creates a vacuum that draws the material into the system, pulling it through the pipeline. This method is commonly used for materials that are light, dusty, or prone to generating airborne particles. The vacuum helps to capture and transport these materials efficiently, minimizing the risk of dust dispersion into the workspace.
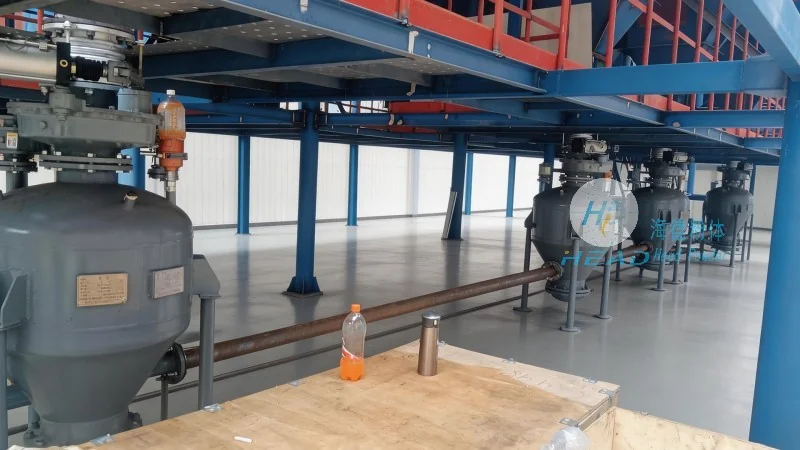
Negative pressure systems are particularly advantageous when dealing with materials that are sensitive to pressure changes or when the process requires a controlled suction environment. However, they may pose challenges related to air intake and potential contamination from external air, as the system is exposed to the surrounding atmosphere during operation.
When comparing positive and negative pressure conveying, several critical factors emerge. From a containment perspective, positive pressure systems are generally considered more effective at preventing product and environmental contamination, as they prevent external air from entering the system. Negative pressure systems, while effective at capturing material, may still allow some external air to enter, which could introduce contaminants or affect product quality.
In terms of energy consumption, positive pressure systems typically require more power to maintain the higher pressure, whereas negative pressure systems rely on vacuum pumps, which may be more energy-efficient for certain applications. The choice of system also impacts the design and maintenance requirements. Positive pressure systems often involve more robust sealing components to maintain pressure integrity, while negative pressure systems may require additional filtration to ensure air quality.
The selection of the appropriate pneumatic conveying method directly impacts the overall quality and safety of pharmaceutical products. For instance, in the production of sterile powders or active pharmaceutical ingredients (APIs), positive pressure systems are often preferred due to their superior containment capabilities. These systems help maintain a sterile environment by preventing the ingress of airborne contaminants and ensuring that the material remains under controlled conditions throughout the conveying process.
On the other hand, negative pressure systems may be more suitable for handling materials that are less sensitive to contamination and where the primary concern is dust control. However, even in such cases, the system must be designed to meet GMP (Good Manufacturing Practice) standards, ensuring that all components are easy to clean and maintain.
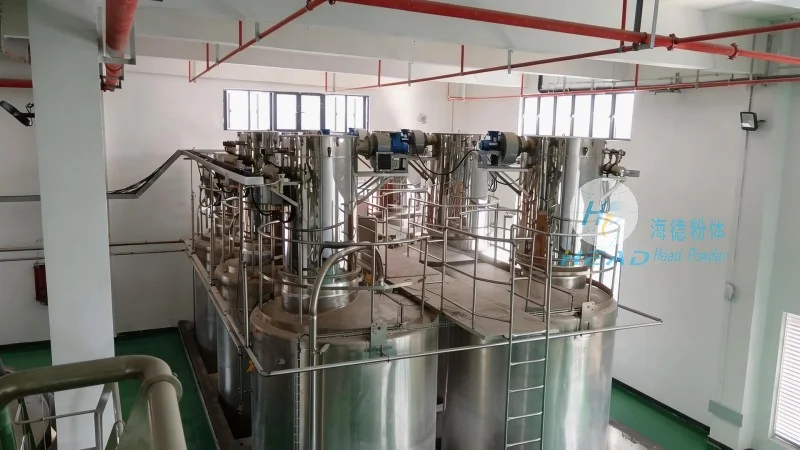
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of the pharmaceutical industry. With a focus on innovation and compliance, HeadPowder Engineering offers both positive and negative pressure conveying systems, as well as hybrid solutions that combine the benefits of both approaches.
The company's expertise lies in understanding the specific challenges faced by pharmaceutical manufacturers, such as maintaining product purity, ensuring operational efficiency, and adhering to regulatory requirements. By leveraging advanced engineering and material science, HeadPowder Engineering develops systems that are not only effective but also scalable and adaptable to changing production demands.
HeadPowder Engineering's solutions are designed to meet the stringent standards of the pharmaceutical industry, including compliance with GMP guidelines and regulatory requirements. The company's team of engineers works closely with clients to assess their material handling needs, providing customized designs that optimize performance while minimizing risks. Whether a client requires a positive pressure system for sensitive materials or a negative pressure system for dust control, HeadPowder Engineering offers comprehensive support from design and manufacturing to installation and maintenance.
With a commitment to quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner for pharmaceutical manufacturers seeking reliable and efficient material handling solutions. By combining technical expertise with a deep understanding of industry requirements, the company ensures that its products contribute to the safe and effective production of pharmaceuticals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top