HeadPowder, a leading manufacturer in the field of pneumatic conveying technology, specializes in providing efficient and reliable solutions for transporting food materials. This article delves into the operation process and working principle of their pneumatic conveying systems, highlighting the key components, operational steps, and the benefits of using such systems in the food industry.
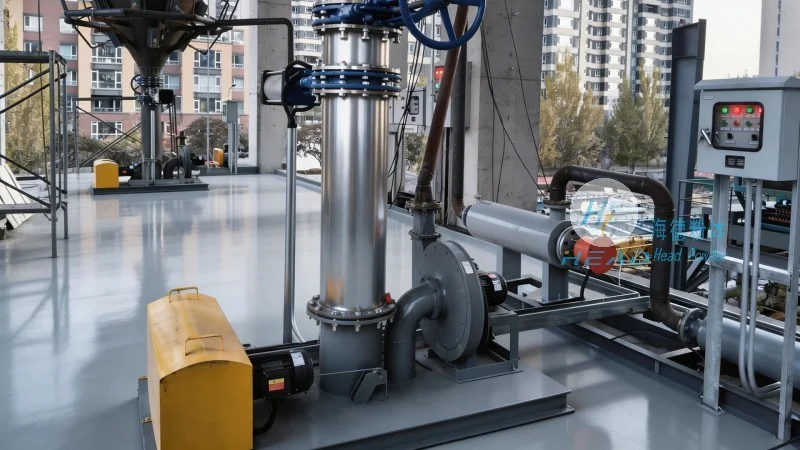
Pneumatic conveying systems are essential for the safe and hygienic transport of bulk food materials such as powders, granules, and fine particles. These systems utilize air or other gases to move materials through a pipeline network, ensuring minimal contamination and maintaining product integrity. HeadPowder's systems are designed with strict adherence to food safety standards, making them suitable for applications in pharmaceuticals, food processing, and other industries where product purity is paramount.
The core components of a pneumatic conveying system include the material feed hopper, the air compressor or blower, the conveying pipeline, the control valves, and the discharge hopper. Each component plays a critical role in the overall operation. The material feed hopper is responsible for storing and feeding the food material into the system. The air compressor or blower generates the necessary air pressure to move the material through the pipeline. The conveying pipeline, typically made of stainless steel or other food-grade materials, ensures the material is transported without contamination. The control valves regulate the flow of air and material, allowing for precise control over the conveying process. Finally, the discharge hopper collects the material at the end of the pipeline, ready for further processing or packaging.
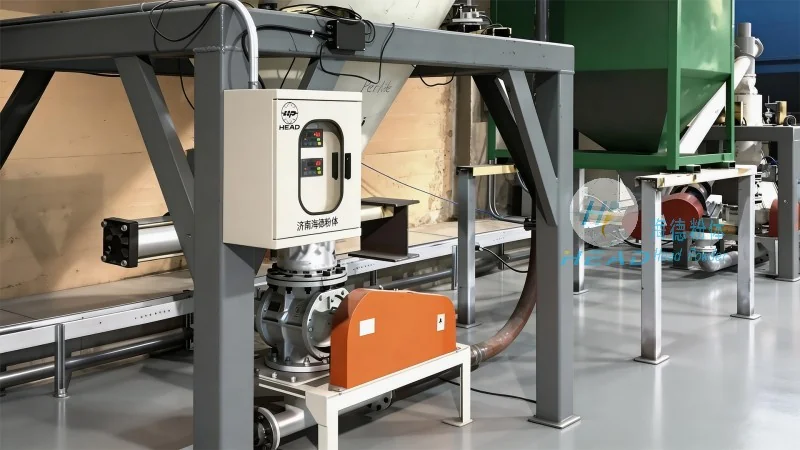
The operation of a pneumatic conveying system for food materials involves several sequential steps. First, the food material is loaded into the feed hopper. The system then starts by activating the air compressor, which generates the required air pressure. As the air flows through the pipeline, it picks up the material from the hopper and transports it to the discharge point. The control valves adjust the air flow rate to maintain a consistent conveying speed, ensuring the material reaches the destination without clogging or loss. Once the material is discharged, the system can be reset for the next batch. This process is automated and can be controlled remotely, enhancing operational efficiency and reducing labor costs.
The working principle of a pneumatic conveying system is based on the principle of fluidization and drag. When air is introduced into the conveying pipeline at a high velocity, it creates a low-pressure zone that draws the food material into the pipeline. The material is then carried along by the air stream, moving through the pipeline to the discharge point. The system can operate in either positive pressure or negative pressure modes. In positive pressure systems, the air is forced into the pipeline, pushing the material forward. In negative pressure systems, the air is drawn out of the pipeline, creating a vacuum that pulls the material along. HeadPowder's systems are designed to operate efficiently in both modes, adapting to different material characteristics and pipeline configurations.
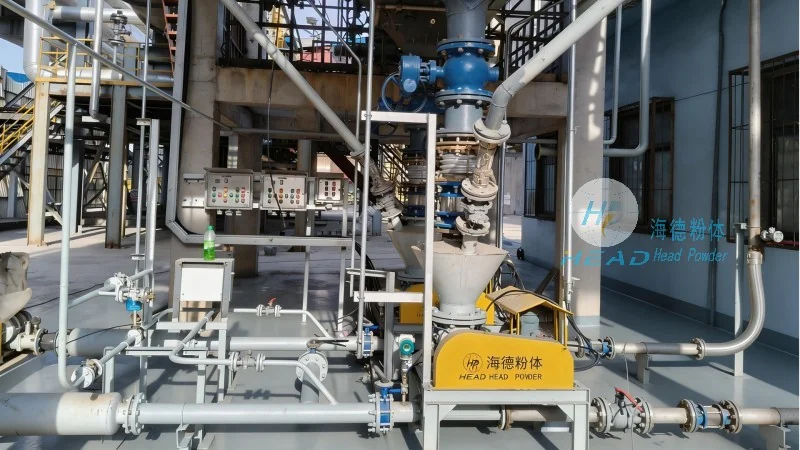
Implementing pneumatic conveying systems in the food industry offers numerous benefits. These systems provide a hygienic and dust-free environment, reducing the risk of contamination and improving product quality. They also offer high efficiency in material transport, with minimal downtime and maintenance requirements. Additionally, the systems are flexible and can be easily integrated into existing production lines, allowing for seamless operation. HeadPowder's pneumatic conveying systems are widely used in various food processing applications, including the transport of flour, sugar, coffee, and other powdered ingredients. They are also suitable for handling sensitive materials that require gentle handling to avoid degradation.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced pneumatic conveying systems for the food industry. Their systems are designed to meet the highest standards of efficiency, safety, and hygiene, ensuring reliable operation in demanding food processing environments. By understanding the operation process and working principle of these systems, food manufacturers can optimize their production processes, improve product quality, and enhance overall operational efficiency. With their expertise and commitment to quality, HeadPowder continues to be a leader in providing innovative solutions for the food industry's material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top