HeadPowder, a leading provider of industrial engineering solutions, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the handling of dust and fly ash. This technology has become increasingly vital in modern industrial processes, offering efficient and reliable methods to transport fine particulate materials. The following discussion explores the fundamental principles, practical applications, and emerging trends in this field, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. based in China.
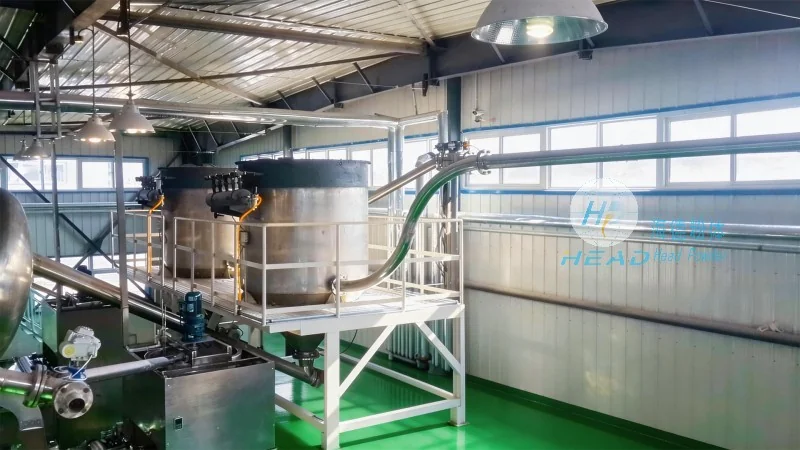
Pneumatic conveying systems operate by utilizing air or gas to transport bulk materials through a pipeline network. The core principle involves creating a pressure differential that propels the material from the source to the destination. There are two primary categories of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push material through the pipeline, while vacuum systems employ a vacuum to draw material into the system. For dust and fly ash, which are typically fine and abrasive, pressure systems are often preferred due to their ability to handle high material loads and maintain consistent flow rates. The system typically consists of a hopper, a conveyor line, and a receiver, with optional components such as rotary valves, filters, and dust collectors to ensure efficient operation and material containment.
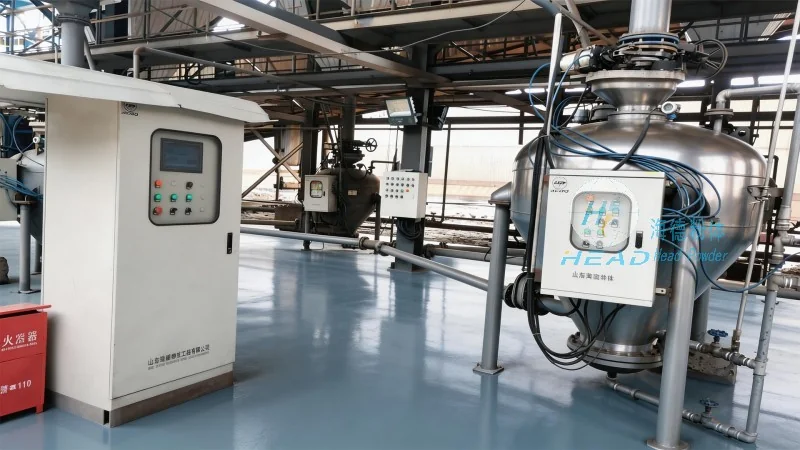
The application of pneumatic conveying technology in dust and fly ash management is widespread across various industries. In power plants, for instance, fly ash generated from coal combustion is commonly transported from the boiler to storage silos or disposal sites using pneumatic systems. This method ensures that the ash is moved without the need for manual handling, reducing labor costs and minimizing environmental risks. Similarly, in cement and construction industries, dust and fine powders are efficiently conveyed from production lines to processing units or storage areas. The technology also finds use in environmental remediation projects, where contaminated dust is transported for treatment and disposal. HeadPowder’s expertise lies in customizing these systems to meet specific operational requirements, ensuring optimal performance and compliance with safety and environmental regulations.
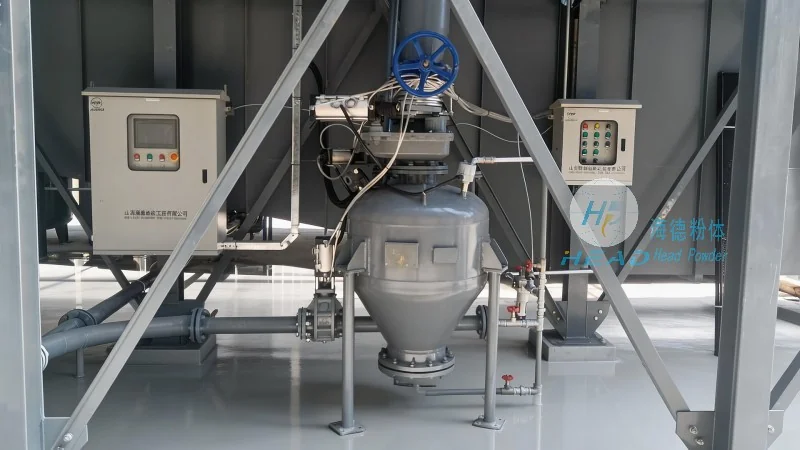
When considering pneumatic conveying systems for dust and fly ash, several key features and advantages stand out. First, the systems offer high efficiency in material transport, with the ability to handle large volumes of fine particulates over long distances. This is particularly beneficial for industries where material handling is a bottleneck. Second, pneumatic conveying minimizes material degradation and contamination, as the material remains enclosed within the pipeline, preventing exposure to external elements. Third, the technology is flexible and can be integrated with existing industrial infrastructure, allowing for seamless upgrades or modifications. Additionally, modern systems incorporate advanced control mechanisms, enabling real-time monitoring and adjustment of flow rates, pressure, and other parameters to optimize performance. These features make pneumatic conveying a preferred choice for industries seeking reliable, cost-effective, and environmentally friendly material handling solutions.
As industrial processes evolve, the pneumatic conveying technology for dust and fly ash continues to advance, driven by technological innovations and increasing demand for efficiency. One emerging trend is the integration of automation and digitalization in conveying systems. Modern systems now incorporate sensors, IoT devices, and advanced control software, enabling predictive maintenance, real-time data analysis, and remote monitoring. This not only enhances operational efficiency but also reduces downtime and maintenance costs. Another trend is the development of more energy-efficient systems, such as those utilizing variable frequency drives (VFDs) to optimize air consumption and reduce energy costs. Additionally, there is a growing focus on sustainable practices, with companies like Shandong HeadPowder Engineering Co., Ltd. investing in eco-friendly materials and energy-saving technologies to minimize the environmental impact of their operations. The future of pneumatic conveying for dust and fly ash is likely to see further advancements in system design, materials, and control technologies, ensuring that these systems remain at the forefront of industrial material handling solutions.
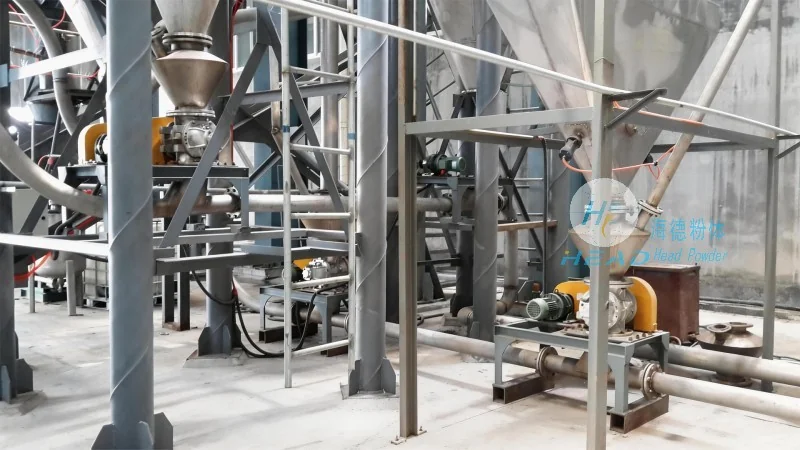
Pneumatic conveying technology for dust and fly ash represents a critical advancement in industrial material handling, offering efficient, reliable, and environmentally friendly solutions. With its ability to handle fine particulates over long distances and integrate seamlessly with existing processes, this technology has become indispensable in various industries. Shandong HeadPowder Engineering Co., Ltd., with its expertise in designing and implementing advanced pneumatic conveying systems, continues to play a vital role in meeting the evolving needs of the industry. As technology advances, the future of this field holds promising developments that will further enhance the efficiency and sustainability of material handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top