When designing a pneumatic conveying system for polyethylene pellets, several critical factors must be considered to ensure efficiency, reliability, and safety. The process of transporting polyethylene pellets via air involves selecting appropriate equipment, understanding material properties, and implementing proper system controls. This article outlines key design considerations that can help engineers and facility managers optimize their polyethylene pellet pneumatic conveying systems.
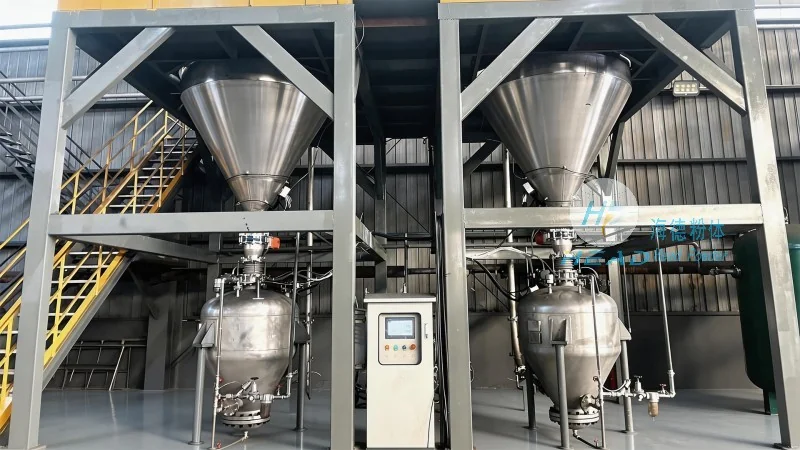
Polyethylene pellets are commonly used in various industrial applications due to their versatility and ease of processing. These pellets typically have a uniform size and density, but their behavior in a pneumatic system can vary based on moisture content, temperature, and particle size distribution. It is essential to characterize the polyethylene pellets before system design to ensure the chosen conveying method is suitable. For instance, dry polyethylene pellets are generally more manageable than wet or contaminated pellets, which may require additional drying or cleaning steps before conveyance.
The core components of a polyethylene pellet pneumatic conveying system include the hopper, feeder, air compressor, pipeline, and receiver. Each component plays a vital role in the overall system performance. The hopper must be designed to store the pellets efficiently, with proper aeration to prevent bridging or caking. The feeder, often a rotary valve or screw feeder, controls the flow rate of pellets into the system, ensuring consistent material delivery. The air compressor provides the necessary pressure and volume to move the pellets through the pipeline, and the pipeline design must account for pressure drop, material velocity, and potential blockages. The receiver is where the polyethylene pellets are deposited, and it should be equipped with a venting system to manage air pressure and prevent dust accumulation.
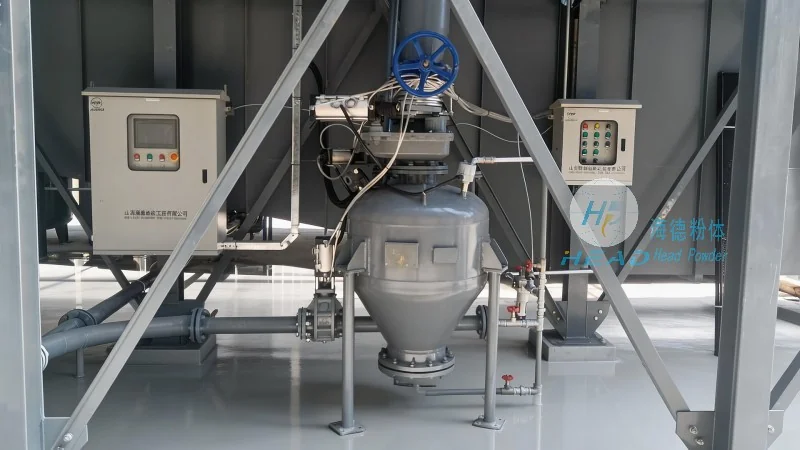
Effective flow control is crucial for maintaining the stability of the pneumatic conveying system. The choice of feeder type and its adjustment settings directly impact the system's performance. For polyethylene pellets, a rotary valve with adjustable speed or a vibratory feeder may be used to regulate the material flow. Additionally, the system should include pressure sensors and flow meters to monitor real-time conditions and detect any abnormalities, such as clogs or low material levels. Proper maintenance of these components is essential to prevent downtime and ensure consistent operation.
Accurately sizing the pneumatic conveying system is critical to meet production demands without overdesigning or underdesigning the equipment. Engineers must consider the required conveying capacity, which is typically measured in pounds per hour or cubic meters per hour. The system's capacity should be based on the maximum production rate of the polyethylene pellets and any future expansion plans. The air compressor's capacity must match the system's demand, and the pipeline diameter and length should be optimized to minimize pressure loss and energy consumption. Proper capacity planning ensures the system operates efficiently and cost-effectively over its lifespan.
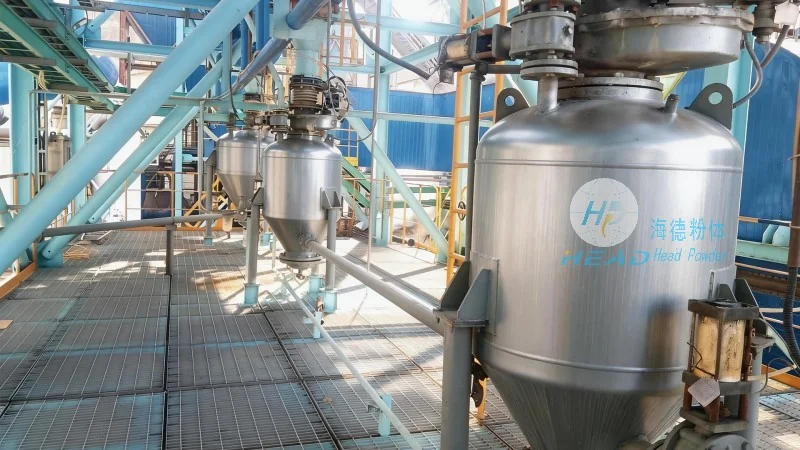
Modern pneumatic conveying systems for polyethylene pellets should prioritize energy efficiency and environmental compliance. The selection of an energy-efficient air compressor, such as a variable-speed model, can reduce operational costs and lower the system's carbon footprint. Additionally, the system should incorporate dust collection and filtration systems to minimize air pollution and comply with local regulations. Proper sealing of the pipeline and components can also prevent air leaks, which contribute to energy waste and reduced system performance. Implementing these measures not only improves the system's sustainability but also enhances its long-term economic viability.
The successful operation of a polyethylene pellet pneumatic conveying system depends on proper installation and regular maintenance. During installation, all components should be aligned correctly, and the pipeline should be checked for leaks or damage. The system should be tested with a small amount of material to verify its performance before full-scale operation. Regular maintenance, including cleaning of the hopper, feeder, and receiver, as well as inspection of the air compressor and filters, is essential to prevent clogs and ensure consistent operation. By following these best practices, facility managers can extend the system's lifespan and minimize unexpected downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top