Wheat pneumatic conveying systems are critical components in modern grain handling operations, ensuring efficient and reliable transport of wheat from storage to processing facilities. Proper design and implementation of these systems are essential to maximize operational efficiency, minimize downtime, and maintain the quality of the wheat. This article outlines key design considerations for wheat pneumatic conveying systems, providing insights into the technical and practical aspects that engineers and facility managers should consider.
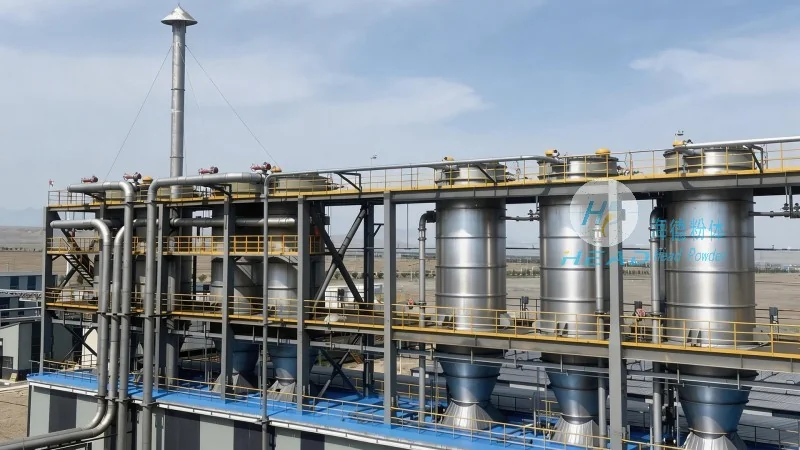
When designing a wheat pneumatic conveying system, the first step is to select the appropriate system type based on the specific requirements of the application. The two primary types are pressure and vacuum systems. Pressure systems use positive pressure to push the material through the pipeline, while vacuum systems use negative pressure to pull the material. For wheat, which is a relatively light and free-flowing material, pressure systems are often preferred due to their ability to handle higher capacities and longer distances. The choice of system type depends on factors such as the distance between the source and destination, the required flow rate, and the available space for the system components.
The pressure or vacuum level in a pneumatic conveying system directly impacts its performance and efficiency. For wheat, typical operating pressures range from 0.5 to 2.0 bar for pressure systems, while vacuum systems may operate at negative pressures of -0.5 to -1.0 bar. Higher pressures allow for greater throughput and longer conveying distances, but they also increase energy consumption and require more robust equipment. It is important to balance these factors to achieve optimal performance. The selection of pressure levels should be based on the specific characteristics of the wheat, such as its bulk density, moisture content, and particle size distribution. For example, wheat with higher moisture content may require higher pressure to prevent clogging or blockages in the pipeline.
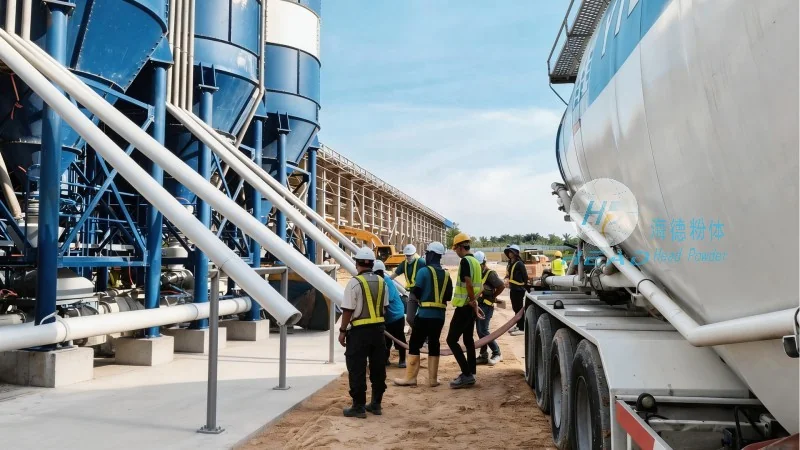
The design of the conveying pipeline is a critical factor in the performance of a wheat pneumatic conveying system. The pipeline should be sized appropriately to handle the expected flow rate and pressure. The diameter of the pipeline is typically determined by the required flow rate and the velocity of the air-wheat mixture. A common rule of thumb is to maintain a conveying velocity of 20-30 meters per second to prevent material deposition and ensure smooth flow. The pipeline layout should be designed to minimize bends and changes in direction, as these can cause pressure losses and increase the risk of blockages. Additionally, the pipeline should be equipped with appropriate fittings, such as elbows, tees, and reducers, to facilitate changes in direction and size. The use of smooth, corrosion-resistant materials, such as stainless steel or PVC, is recommended to prevent material buildup and ensure long-term performance.
Key equipment components in a wheat pneumatic conveying system include the feeder, the conveying line, the receiver, and the air source. The feeder is responsible for feeding the wheat into the pipeline at a consistent rate. For wheat, a rotary valve or a screw feeder is commonly used, as they can handle the material's free-flowing characteristics and provide accurate control of the flow rate. The conveying line, as discussed earlier, should be sized and laid out properly to ensure efficient transport. The receiver is the final component of the system, where the wheat is discharged. It should be designed to handle the pressure and flow rate of the system and prevent material spillage. The air source, typically a blower or a fan, provides the necessary pressure or vacuum to move the wheat through the pipeline. The selection of the air source should be based on the required pressure and flow rate, as well as the efficiency and reliability of the equipment.
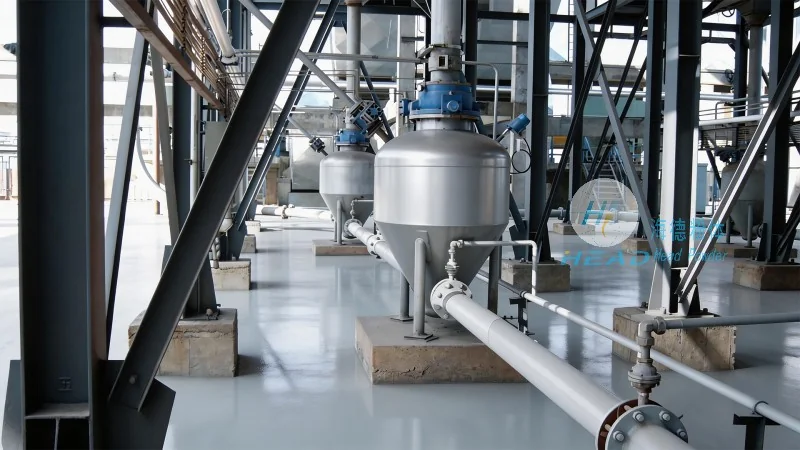
Proper maintenance of the wheat pneumatic conveying system is essential to ensure its long-term performance and reliability. Regular cleaning of the pipeline and equipment is necessary to prevent material buildup and blockages. This can be done using a combination of air blasts and mechanical cleaning tools. The system should also be inspected regularly for signs of wear and tear, such as leaks or corrosion. Any issues should be addressed promptly to prevent further damage. Additionally, the system should be equipped with appropriate safety features, such as pressure relief valves and emergency shut-off valves, to protect operators and the equipment from potential hazards.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of grain handling equipment, specializes in the design and fabrication of wheat pneumatic conveying systems. With years of experience in the industry, the company has developed a range of high-quality systems tailored to the specific needs of wheat processing facilities. The company's systems are designed to meet the highest standards of efficiency, reliability, and safety. For example, one of their recent projects involved the installation of a pressure pneumatic conveying system for a large wheat processing plant in China. The system was designed to transport 500 tons of wheat per hour over a distance of 200 meters. The system was installed and commissioned successfully, achieving the required flow rate and maintaining the quality of the wheat throughout the process. The company's expertise in system design and fabrication has helped many clients improve their operational efficiency and reduce their costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top