Gravity dust removal and pneumatic conveying systems represent a critical technology in modern industrial processes, particularly for handling fine particulate materials efficiently. These systems are designed to capture dust and particulate matter from air streams while simultaneously transporting the material to designated locations. The integration of gravity dust removal with pneumatic conveying ensures both environmental compliance and operational efficiency, making it a preferred choice for industries such as cement, chemical, and food processing.
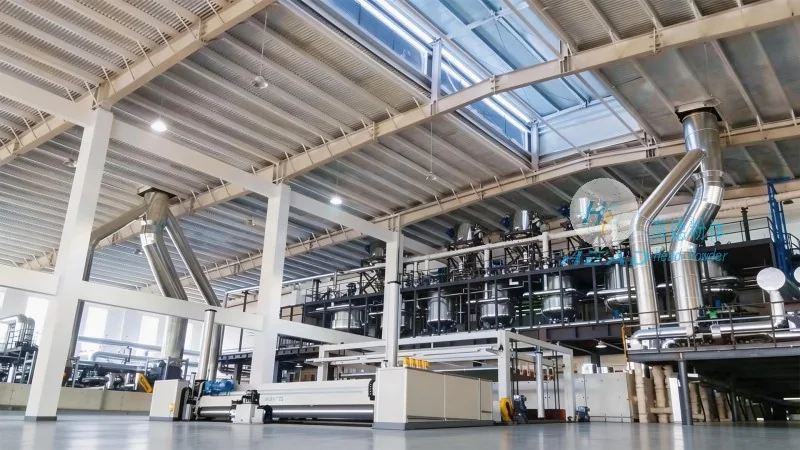
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China, specializing in the design, manufacturing, and installation of advanced dust removal and material handling systems. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for clients seeking reliable solutions for their industrial dust and material transport needs. The company's expertise lies in customizing systems to meet specific operational requirements, ensuring optimal performance and durability.
The gravity dust removal and pneumatic conveying system typically consists of several key components that work in tandem to achieve effective dust capture and material transport. The primary component is the gravity dust collector, which uses gravity and filtration to separate dust particles from the air stream. This collector is often equipped with high-efficiency filters or baghouses to ensure minimal emissions and compliance with environmental regulations. The collected dust is then transferred to a storage or processing unit, while the cleaned air is released back into the environment.
Next, the pneumatic conveying system utilizes air pressure to transport the collected dust or other bulk materials. This system can be either positive pressure (where air is forced through the material) or negative pressure (where air is drawn through the material). The choice of system type depends on factors such as material properties, distance, and required flow rates. HeadPowder designs systems that optimize the conveying efficiency by selecting appropriate air velocities, pipe diameters, and material feed mechanisms.
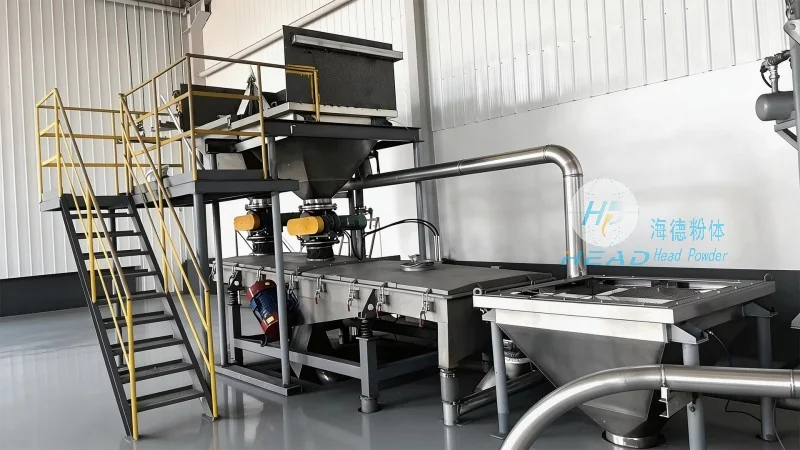
HeadPowder employs a systematic approach to designing gravity dust removal and pneumatic conveying systems, ensuring that each project is tailored to the client's unique needs. The design process begins with a thorough analysis of the material characteristics, including particle size, moisture content, and abrasiveness. This analysis helps in selecting the most suitable gravity dust removal equipment, such as cyclone separators or cartridge filters, and the appropriate pneumatic conveying method, such as dilute phase or dense phase transport.
The system design also considers operational parameters like the required conveying capacity, the distance between the dust source and the destination, and the ambient conditions. HeadPowder uses advanced computational fluid dynamics (CFD) and material flow modeling to simulate the system performance, allowing for adjustments to optimize efficiency and reduce energy consumption. The final design includes detailed specifications for all components, including the gravity dust collector, air handling units, conveying pipes, and material feeders.
Adopting a gravity dust removal and pneumatic conveying system offers numerous benefits for industrial operations. Firstly, it significantly reduces air pollution by capturing dust particles before they are released into the environment, thereby meeting or exceeding regulatory standards. This not only protects the environment but also enhances the company's reputation and compliance status. Secondly, the system improves workplace safety by eliminating the need for manual handling of dust-laden materials, reducing the risk of respiratory illnesses and other health hazards.
Thirdly, the pneumatic conveying system enhances operational efficiency by automating the material transport process. This reduces labor costs and minimizes material loss during handling. The system also allows for precise control over material flow rates, ensuring consistent production processes. Additionally, the integration of gravity dust removal with pneumatic conveying reduces the need for separate dust collection and material handling equipment, leading to space savings and lower overall operational costs.
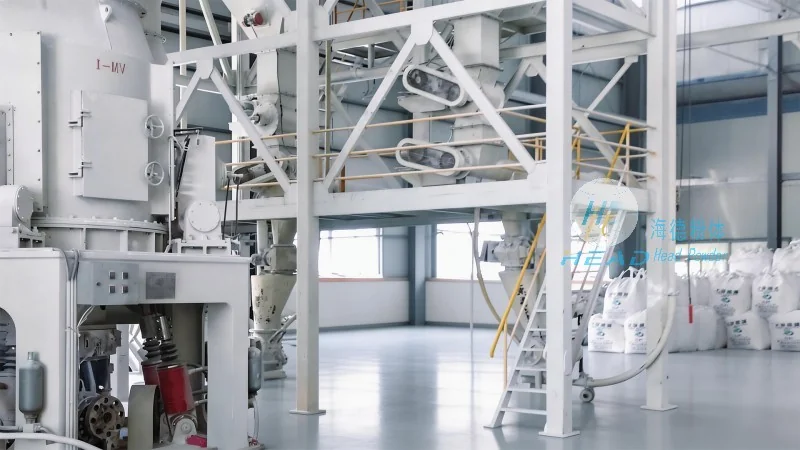
HeadPowder has successfully implemented gravity dust removal and pneumatic conveying systems in various industries, demonstrating the versatility and effectiveness of their solutions. For instance, in a cement manufacturing plant, the system was designed to capture fine cement dust from the production line and transport it to a storage silo. The gravity dust collector efficiently separated the dust from the air stream, while the pneumatic conveying system delivered the material to the silo without any spillage or loss. The client reported a 90% reduction in dust emissions and a 20% increase in material handling efficiency.
In another application, a chemical processing facility used the system to handle hazardous powders, such as silica or titanium dioxide. The gravity dust removal component was equipped with high-efficiency filters to ensure that no harmful particles were released into the air. The pneumatic conveying system was designed with explosion-proof features to handle the hazardous materials safely. The system's performance met all safety and regulatory requirements, and the client was satisfied with the reliable operation and reduced maintenance costs.
Gravity dust removal and pneumatic conveying systems are essential for modern industrial operations, providing a sustainable and efficient solution for dust and material handling. HeadPowder, with its expertise and commitment to quality, continues to lead in the development of advanced systems that meet the evolving needs of industries. By focusing on customization, innovation, and compliance, HeadPowder ensures that its clients receive systems that not only perform effectively but also contribute to long-term operational success and environmental responsibility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top