Quartz stone, a widely used material in various industries such as construction, electronics, and manufacturing, often requires efficient and reliable transportation methods for its powder and granular forms. Pneumatic conveying, a technology that utilizes air flow to move bulk materials, has emerged as a key solution for handling quartz stone and similar powders. This article explores the principles and applications of quartz stone pneumatic conveying, focusing on how to achieve efficient material transport through air flow systems.
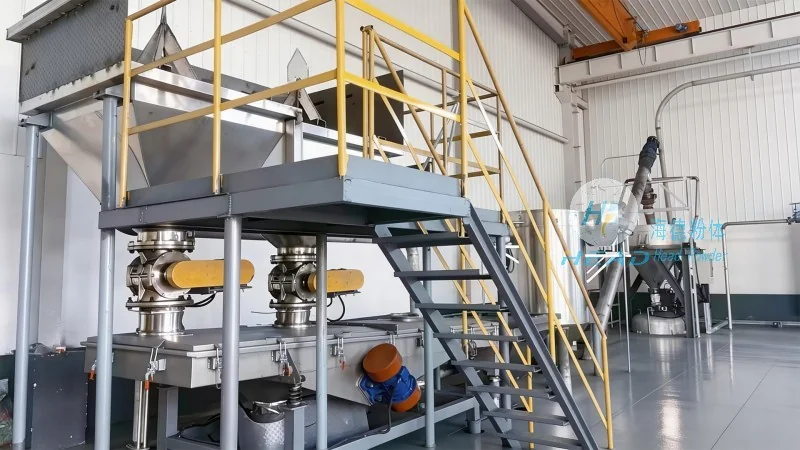
Pneumatic conveying systems are designed to transport dry bulk materials like quartz stone powder and granules using pressurized or vacuum air streams. Unlike traditional mechanical conveyors, which rely on belts, buckets, or screws, pneumatic systems use air to move materials through pipes, offering advantages such as cleanliness, flexibility, and the ability to handle fine powders without contamination. For quartz stone, which is often used in applications requiring high purity and consistency, pneumatic conveying ensures that the material remains free from external contaminants during transport.
A typical quartz stone pneumatic conveying system consists of several essential components that work together to ensure efficient material transport. The primary components include the air source (usually a blower or compressor), the conveying line (pipes made of materials like stainless steel or plastic to prevent material degradation), the material feeders (hoppers or rotary valves that control the flow of quartz stone into the system), and the discharge equipment (such as cyclones or filters that separate the material from the air stream). Additionally, control systems and monitoring devices are often integrated to regulate pressure, flow rates, and material levels, ensuring optimal performance.
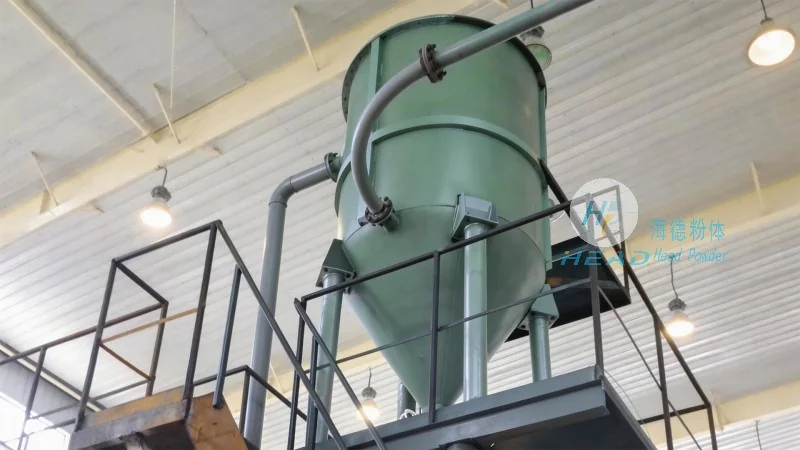
The efficiency of quartz stone pneumatic conveying depends heavily on the proper management of air flow. The velocity of the air stream must be sufficient to lift and transport the quartz stone particles through the pipes without causing excessive wear or degradation. For fine quartz powders, higher air velocities are often required to prevent clogging or particle separation. Conversely, for larger granules, lower velocities may be sufficient while maintaining a stable flow. The system also needs to balance pressure and vacuum levels to ensure that the material is moved without excessive energy consumption or damage to the quartz stone particles. Advanced systems may use variable frequency drives (VFDs) to adjust air flow rates dynamically, optimizing energy use and transport efficiency based on the material's characteristics and the system's load.
Quartz stone pneumatic conveying is widely used in various stages of quartz stone processing, from raw material handling to finished product packaging. In mining operations, pneumatic systems can transport crushed quartz stone from storage silos to processing plants, reducing the need for manual handling and improving safety. During the grinding and polishing stages, pneumatic conveying is used to move fine quartz powders to mixing and blending equipment, ensuring uniform material distribution. In the final stages, the system can transport finished quartz products to packaging lines, maintaining product purity and reducing downtime. The benefits of using pneumatic conveying for quartz stone include improved material quality control, reduced labor costs, enhanced safety by eliminating manual handling of powders, and increased production efficiency through automated transport processes.
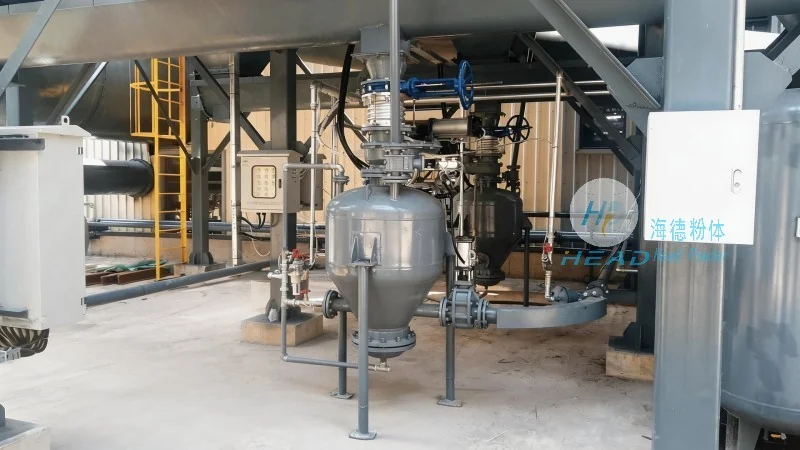
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing custom pneumatic conveying systems tailored to the specific needs of quartz stone applications. With operations based in Shandong, China, HeadPowder leverages its expertise in material science and engineering to develop systems that maximize efficiency and minimize downtime. For example, a recent project involved supplying a pneumatic conveying system to a quartz stone manufacturer that required the transport of fine quartz powders from grinding mills to a mixing plant. The system, equipped with high-efficiency cyclones and VFD-controlled blowers, achieved a transport efficiency of over 95%, significantly reducing material loss and improving overall production throughput. HeadPowder's solutions also emphasize durability and maintenance, using corrosion-resistant materials and robust components to ensure long-term performance in demanding quartz stone processing environments.
Pneumatic conveying represents a sophisticated and efficient method for handling quartz stone and other fine powders, offering significant advantages over traditional mechanical transport systems. By leveraging air flow to move materials through sealed pipes, these systems ensure cleanliness, safety, and high material purity, which are critical for applications in construction, electronics, and manufacturing. As the demand for high-quality quartz stone products continues to grow, the importance of efficient material handling technologies like pneumatic conveying will only increase. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing tailored solutions that meet the evolving needs of the quartz stone industry, helping manufacturers optimize their operations and maintain a competitive edge in the market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top