HeadPowder, a leading engineering firm based in Shandong, China, specializes in innovative material handling solutions. The company's expertise lies in developing advanced pneumatic conveying systems tailored for the organic fertilizer industry. This article explores the benefits and applications of granule pneumatic conveying systems designed to efficiently transport organic fertilizer over extended distances.
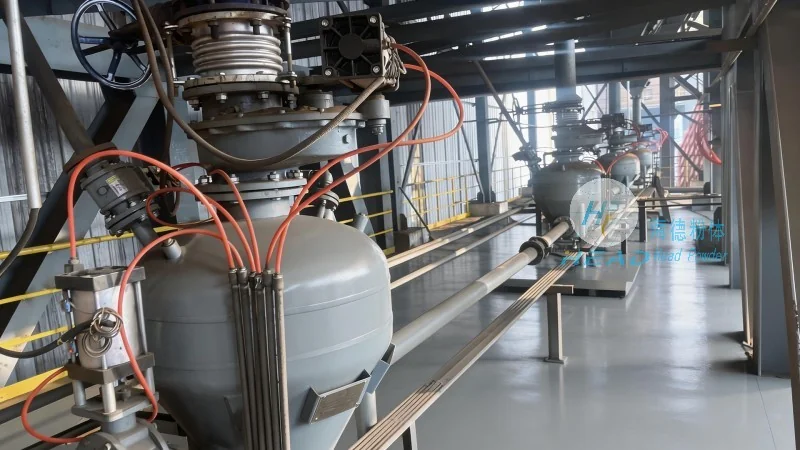
Pneumatic conveying systems utilize air or gas to transport bulk materials like organic fertilizer granules. Unlike traditional methods such as belt conveyors or trucks, pneumatic conveying offers a flexible and efficient solution for moving materials over long distances without the need for complex infrastructure. The technology is particularly suitable for organic fertilizers due to its ability to handle fine or irregularly shaped particles while maintaining low dust emissions and minimal product degradation.
HeadPowder's granule pneumatic conveying systems are engineered to overcome the limitations of traditional material transport methods. These systems are designed to handle organic fertilizer granules with diameters ranging from 1mm to 10mm, ensuring optimal performance across various particle sizes. The technology incorporates advanced air flow control mechanisms that maintain consistent material flow rates, reducing the risk of blockages and ensuring reliable operation. Additionally, the systems are equipped with dust suppression features, such as cyclone separators and filtration units, to minimize environmental impact and comply with industrial regulations.
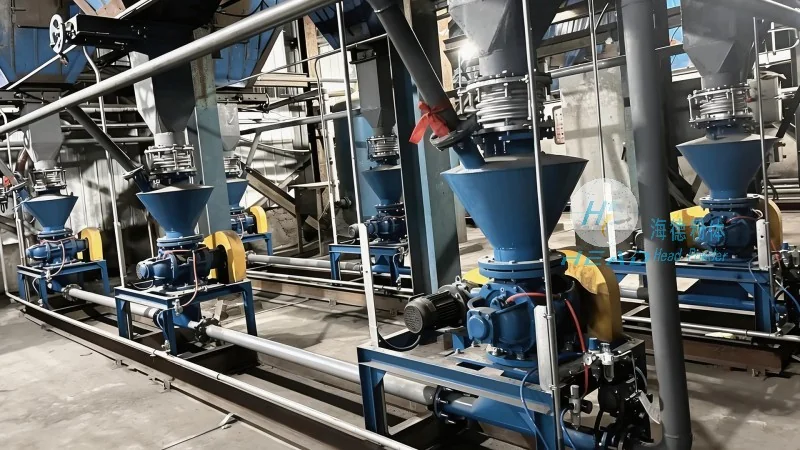
One of the primary advantages of pneumatic conveying is its ability to transport organic fertilizer over distances exceeding 100 meters without compromising material quality. Traditional methods often face challenges such as material degradation, dust generation, and operational inefficiencies over longer distances. Pneumatic systems, however, maintain the integrity of the fertilizer by using controlled air pressure and flow rates, ensuring that the product remains free from contamination and retains its nutritional value. This makes it an ideal solution for farms and processing facilities located in remote areas or requiring large-scale material movement.
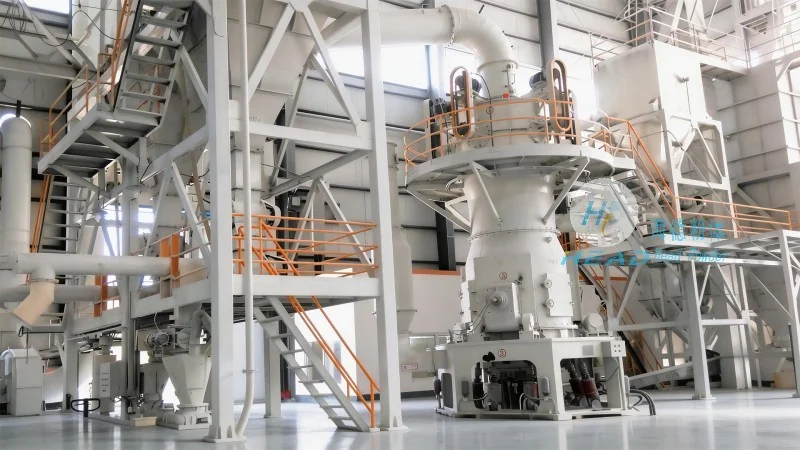
The granule pneumatic conveying systems developed by HeadPowder are widely used in the organic fertilizer production and distribution chain. These systems are commonly employed in the following applications:
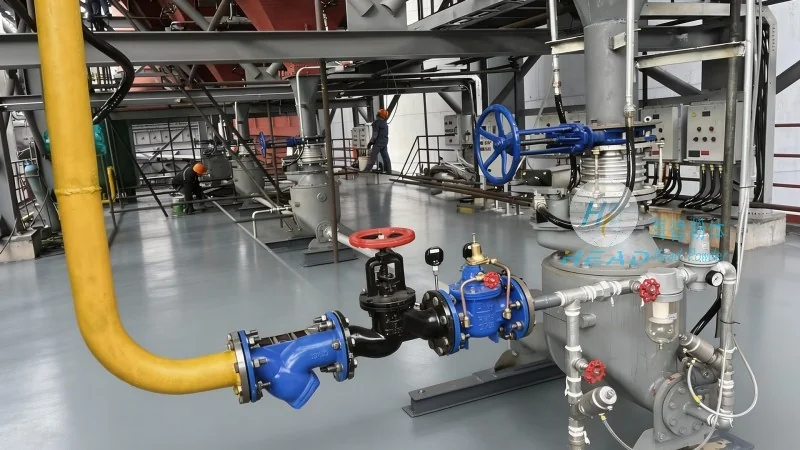
HeadPowder understands that each client's needs are unique. Therefore, the company offers customized pneumatic conveying solutions tailored to specific operational requirements. Whether a client needs a system for small-scale farm operations or a large-scale industrial facility, HeadPowder can design and implement a solution that meets their needs. The systems are scalable, allowing for easy expansion as the client's production or operational needs grow. This flexibility ensures that the investment in a pneumatic conveying system provides long-term value and adaptability.
HeadPowder's granule pneumatic conveying systems represent a significant advancement in material handling technology for the organic fertilizer industry. By overcoming distance limitations and providing efficient, reliable, and environmentally friendly transport solutions, these systems enhance operational efficiency and product quality. As the demand for organic fertilizers continues to grow, the adoption of advanced pneumatic conveying systems will play a crucial role in meeting the industry's needs. HeadPowder remains committed to delivering innovative solutions that help clients achieve their operational goals while maintaining the highest standards of quality and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top