When it comes to managing the transportation of ammonium bicarbonate in industrial processes, selecting the appropriate pneumatic conveying system is crucial for efficiency, safety, and cost-effectiveness. Ammonium bicarbonate is a chemical compound widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. The proper handling of this material requires specialized equipment that can handle its unique properties, such as its hygroscopic nature and potential for dust generation. This article will guide you through the key considerations and factors to evaluate when choosing a pneumatic conveying system for your ammonium bicarbonate handling operations.
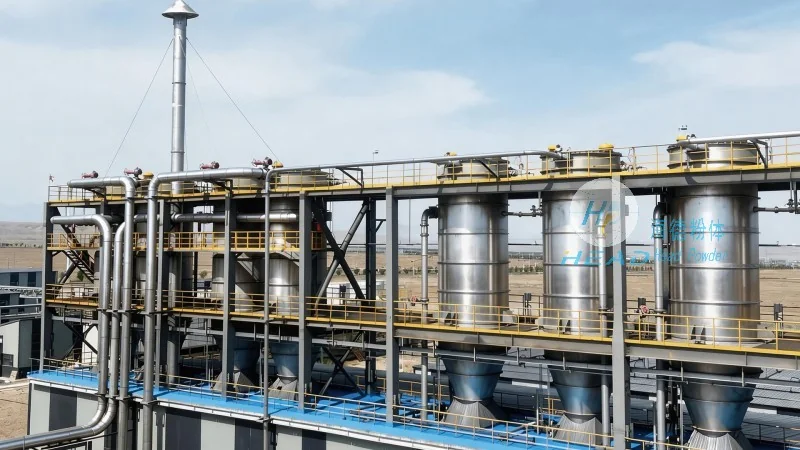
Ammonium bicarbonate (NH₄HCO₃) is a white crystalline powder that is highly soluble in water and has a tendency to absorb moisture from the air. This hygroscopic characteristic makes it challenging to handle, as it can clump or cake if not managed properly. Pneumatic conveying systems offer a solution by transporting the material in a closed system using air or gas as the conveying medium. This method minimizes exposure to the environment, reduces dust contamination, and ensures consistent material flow. For ammonium bicarbonate, a system that can handle the material's sensitivity to moisture and its potential for dust generation is essential. The right system will maintain the material's quality and prevent degradation during transport.
Several critical factors must be evaluated when selecting a pneumatic conveying system for ammonium bicarbonate. These factors include the material's physical properties, the required conveying distance and capacity, the system's energy efficiency, and the overall operational environment. The first consideration is the material's characteristics. Ammonium bicarbonate is a fine powder with a relatively low bulk density, which affects the conveying velocity and pressure requirements. The system must be designed to handle the material's flowability and prevent blockages or clogging. Second, the conveying distance and throughput are important. The system should be capable of transporting the material from the storage or production area to the processing or packaging units without excessive pressure loss or energy consumption. Third, energy efficiency is a key factor for long-term operational costs. A well-designed system will minimize energy usage while maintaining the required conveying performance. Finally, the operational environment, including ambient temperature and humidity, should be considered, as these factors can impact the material's properties and the system's performance.
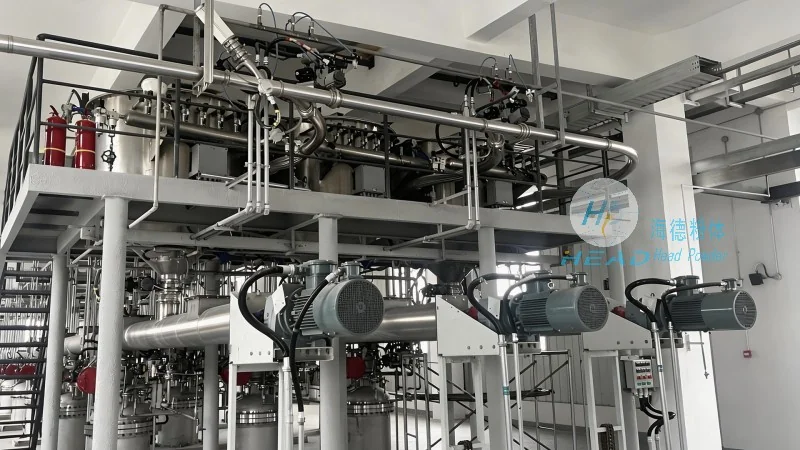
There are several types of pneumatic conveying systems available, each with its own advantages and limitations. The most common types include positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems use a blower or compressor to generate air pressure and push the material through the system. These systems are suitable for short to medium conveying distances and can handle a wide range of materials, including ammonium bicarbonate. Negative pressure systems, on the other hand, use a vacuum to draw the material into the system. This type is ideal for applications where dust control is a priority, as the material is contained within the system and does not escape into the environment. Hybrid systems combine elements of both positive and negative pressure systems, offering flexibility in conveying different materials over varying distances. For ammonium bicarbonate, a positive pressure system is often preferred due to its ability to handle the material's hygroscopic nature and prevent moisture absorption during transport. However, the choice of system ultimately depends on the specific application requirements and operational constraints.
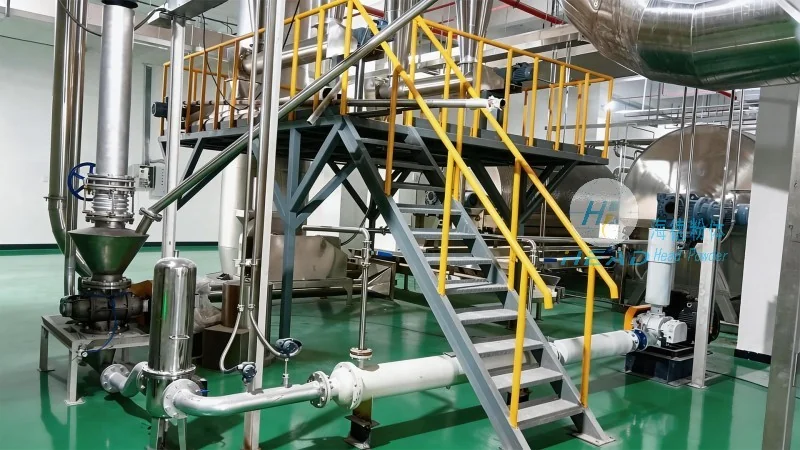
When selecting a pneumatic conveying system, it is essential to evaluate the key components and their performance characteristics. The system components include the feeder, the conveying line, the receiver, and the air handling equipment. The feeder is responsible for feeding the material into the system at a consistent rate, which is critical for maintaining a stable flow. For ammonium bicarbonate, a rotary valve or a screw feeder is commonly used to ensure a uniform material feed. The conveying line is typically made of stainless steel or other corrosion-resistant materials to prevent the material from reacting with the equipment and to maintain hygiene standards. The receiver is where the material is deposited, and it should be designed to prevent dust leakage and maintain material quality. The air handling equipment, including the blower or vacuum pump, must be capable of providing the necessary pressure or vacuum to transport the material efficiently. The performance of the system is also influenced by the material's flow properties, such as its angle of repose and compressibility. These properties affect the pressure drop along the conveying line and the required air velocity. A well-designed system will optimize these parameters to achieve the desired conveying capacity and efficiency.
Integration of the pneumatic conveying system with existing processes is another important consideration. The system should be compatible with the current infrastructure, including storage tanks, processing equipment, and packaging lines. This ensures smooth operation and minimal disruption to the production schedule. Additionally, the system's maintenance requirements should be evaluated. Ammonium bicarbonate can be abrasive and may cause wear on the system components over time. Regular maintenance, such as cleaning the conveying line and replacing worn parts, is necessary to ensure the system's longevity and performance. The system should be designed with easy access to components for maintenance and cleaning, which reduces downtime and operational costs. Furthermore, the system's safety features, such as dust explosion prevention and overpressure protection, should be considered, as ammonium bicarbonate is a combustible dust in certain conditions. A properly designed system will incorporate these safety measures to protect personnel and equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top