Managing rare earth crystal powders in industrial operations requires specialized equipment to ensure efficient, safe, and reliable material transport. The selection of a pneumatic conveying system is a critical decision that impacts overall process efficiency, product quality, and operational costs. This article provides a comprehensive guide to help you navigate the options and choose the most appropriate system for your specific rare earth crystal powder handling workflow.
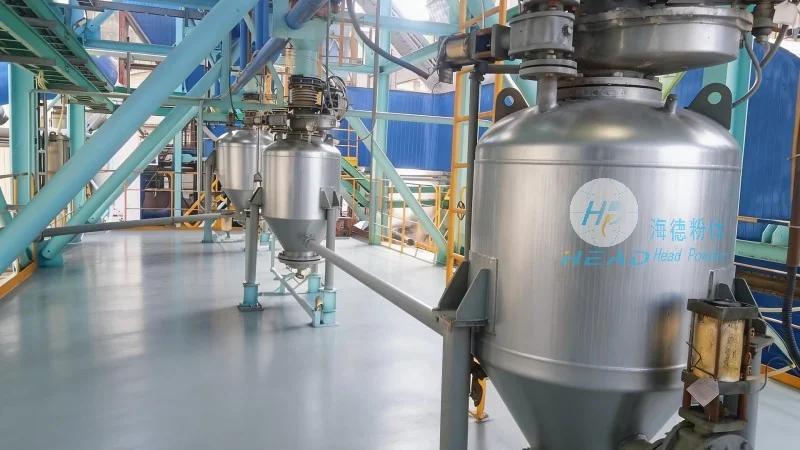
Rare earth crystal powders are often characterized by their fine particle size, high density, and potential for static charge accumulation. These properties make traditional bulk handling methods less suitable and may lead to issues such as clogging, dust generation, and material degradation. Pneumatic conveying systems offer a solution by using air pressure to transport powders through pipelines, minimizing contact with equipment and reducing the risk of contamination. The right system can also help maintain the powder's physical and chemical properties, which is essential for downstream processing applications.
Several factors must be evaluated when selecting a pneumatic conveying system for rare earth crystal powders. First, consider the powder's physical characteristics, including particle size distribution, moisture content, and flowability. These properties influence the system's design, such as the required air velocity and pressure. Second, assess the process requirements, including the distance and height of material transport, as well as the desired throughput capacity. Third, evaluate the operational environment, including space constraints, noise levels, and safety regulations. Finally, consider the long-term cost implications, including energy consumption, maintenance requirements, and system lifespan.
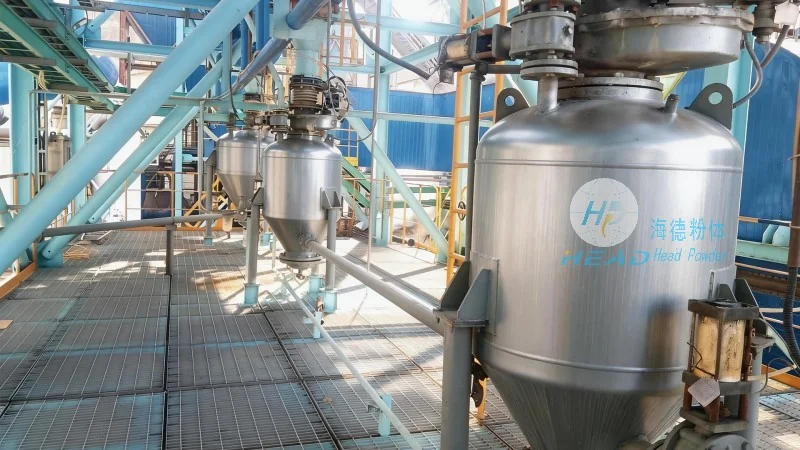
There are primarily two types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems use compressed air to push the powder through the pipeline, while negative pressure systems use vacuum to draw the powder. Each type has its advantages and is suitable for different applications. Positive pressure systems are generally more suitable for long-distance or high-rise transport, as they can maintain consistent pressure and flow. Negative pressure systems are better for short-distance transport or when the powder needs to be isolated from the environment to prevent dust emissions. For rare earth crystal powders, positive pressure systems are often preferred due to their ability to handle high concentrations of powder and maintain consistent flow rates.
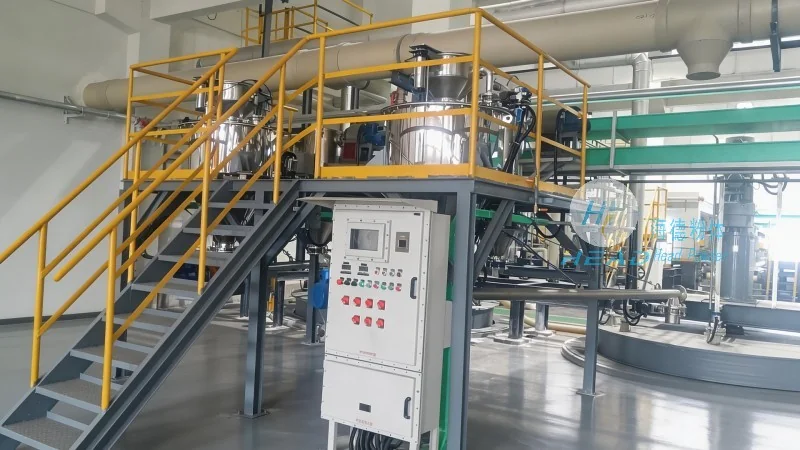
HeadPowder Engineering specializes in providing customized pneumatic conveying solutions that integrate seamlessly with existing rare earth crystal powder handling processes. Our team works closely with clients to understand their specific requirements and design systems that meet their operational needs. This includes selecting the appropriate equipment, such as rotary valves, feeders, and receivers, and ensuring compatibility with existing infrastructure. Customization may also involve incorporating features like dust collection systems, material drying units, or temperature control mechanisms to further enhance the system's performance and safety.
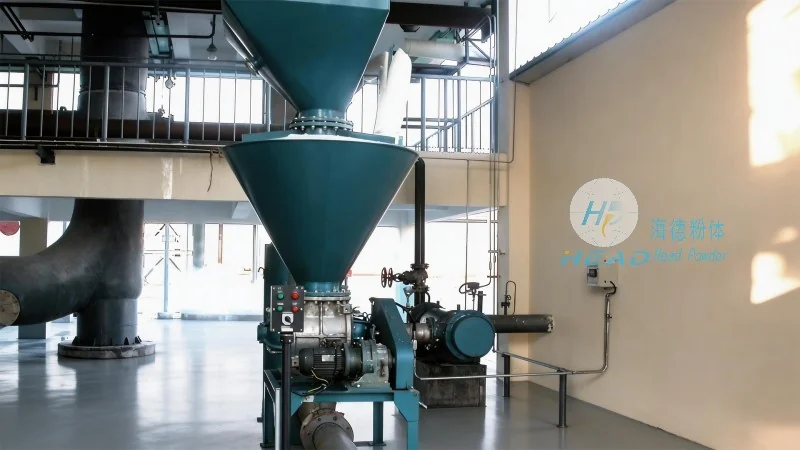
Reliability is a top priority when selecting a pneumatic conveying system for rare earth crystal powders. HeadPowder Engineering uses high-quality components and materials that are resistant to corrosion and wear, ensuring long-term performance. Regular maintenance is also essential to keep the system operating at optimal levels. Our team provides comprehensive maintenance services, including routine inspections, component replacement, and troubleshooting, to minimize downtime and maximize system efficiency. By choosing a well-designed and properly maintained system, you can ensure consistent performance and reduce the risk of material loss or equipment failure.
Selecting the right pneumatic conveying system for your rare earth crystal powder handling process is a critical decision that requires careful consideration of various factors. By understanding the powder's properties, process requirements, and available options, you can choose a system that enhances efficiency, safety, and product quality. HeadPowder Engineering, based in Shandong, China, offers customized solutions tailored to the unique needs of rare earth crystal powder handling. Our team of experts is ready to assist you in selecting the most appropriate pneumatic conveying system and ensuring optimal performance for your operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top