For industries dealing with glucose handling, selecting the appropriate pneumatic conveying system is a critical decision that impacts operational efficiency, product quality, and overall process reliability. The right system ensures that glucose is transported safely and efficiently from storage to processing units, minimizing downtime and reducing the risk of contamination. This guide will walk you through the key considerations and factors to evaluate when choosing a pneumatic conveying system tailored to your glucose handling process.
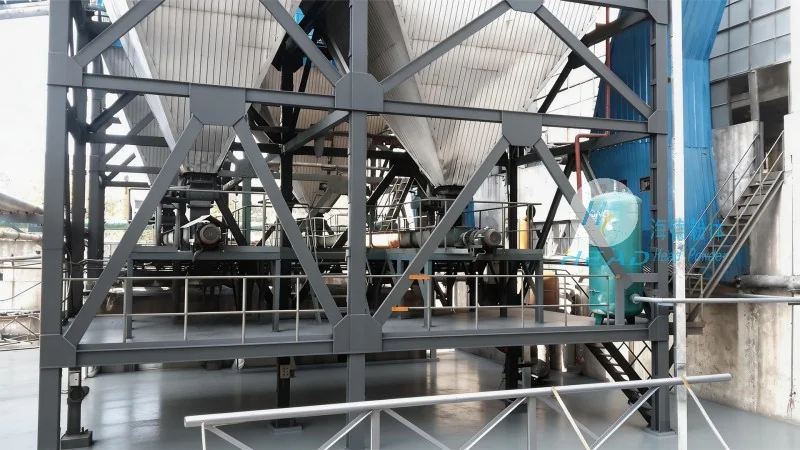
Glucose, a vital ingredient in various food, pharmaceutical, and industrial applications, requires specialized handling to maintain its purity and integrity. Traditional conveying methods like belt conveyors or bucket elevators may not be suitable for fine powders or granules, as they can lead to product degradation, dust generation, and increased maintenance costs. Pneumatic conveying systems offer a solution by using air to transport materials in a closed or open loop, providing a hygienic, dust-free, and controlled environment. This method is particularly advantageous for glucose, which is sensitive to moisture and contamination, as it minimizes exposure to external elements and maintains product quality throughout the transfer process.
When evaluating pneumatic conveying systems for glucose handling, several factors must be considered to ensure optimal performance and compatibility with your specific process requirements. The first step is to assess the material characteristics of the glucose, including its particle size, density, flowability, and moisture content. These properties will determine the most suitable conveying method—such as pressure or vacuum systems—and the type of equipment needed, such as rotary valves, filters, and cyclones. Additionally, the system must be designed to handle the volume and flow rate required by your production scale, ensuring that it can meet the throughput demands without causing bottlenecks or excessive energy consumption.
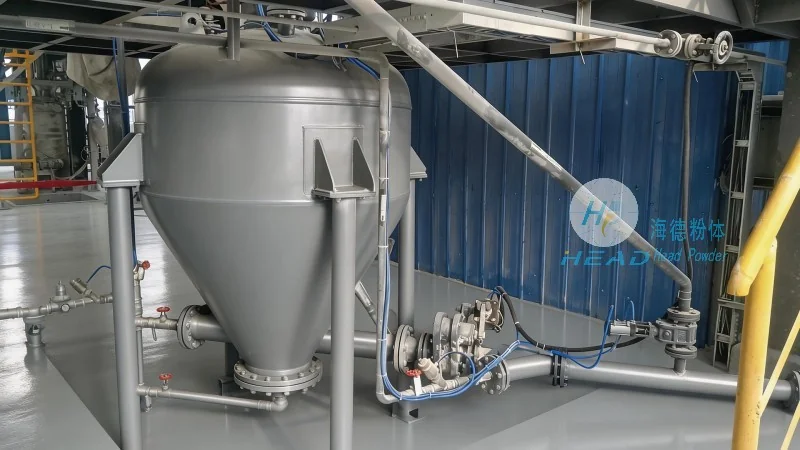
Another critical factor is the system's ability to maintain product purity and prevent cross-contamination. For glucose, which is often used in food and pharmaceutical applications, hygiene is paramount. The chosen system should feature components that are easy to clean and maintain, such as stainless steel construction, CIP (Clean-in-Place) compatible parts, and sealed connections. This ensures that the conveying process does not introduce contaminants or introduce moisture, which could affect the glucose's quality and shelf life. Furthermore, the system's energy efficiency and operational costs should be evaluated, as pneumatic conveying can be more energy-intensive than other methods, but modern designs aim to optimize performance and reduce long-term expenses.
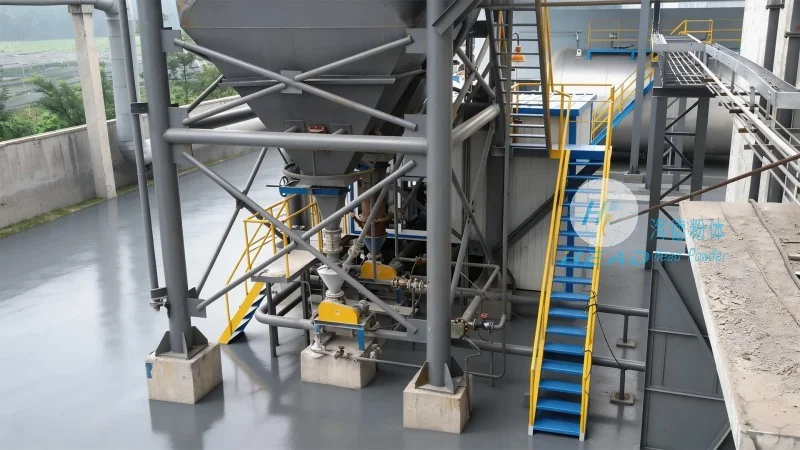
Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized pneumatic conveying systems tailored to the unique needs of glucose handling processes. With years of experience in the industry, HeadPowder understands the challenges associated with transporting fine powders like glucose and offers solutions that address these challenges effectively. The company's team of engineers works closely with clients to assess their specific requirements, from material properties to production scale, and designs systems that meet both functional and regulatory standards. HeadPowder's systems are built with high-quality materials, such as stainless steel and food-grade components, ensuring durability and compliance with industry regulations. The company also provides comprehensive support, including installation, commissioning, and maintenance services, to ensure that the system operates at peak performance throughout its lifecycle.
Every glucose handling process is unique, and a one-size-fits-all approach to pneumatic conveying is not effective. HeadPowder recognizes this and offers customized solutions that integrate seamlessly with existing infrastructure. Whether you need a system for bulk storage, transfer, or processing, the company can design a solution that aligns with your production workflow. The customization process involves detailed analysis of the process flow, material handling requirements, and operational constraints to develop a system that maximizes efficiency and minimizes downtime. HeadPowder's engineers use advanced design software to model the system and simulate its performance, ensuring that the final solution meets all performance criteria before installation. This approach helps to avoid costly errors and ensures that the system is optimized for the specific needs of your glucose handling process.
Reliability is a top priority when selecting a pneumatic conveying system for glucose handling, as downtime can result in significant financial losses and product waste. HeadPowder's systems are designed with reliability in mind, using robust components and proven technologies that have been tested in various industrial applications. The company's commitment to quality is reflected in its use of high-quality materials and rigorous quality control processes. Each system is manufactured in accordance with industry standards and undergoes thorough testing before delivery to ensure that it meets the required performance specifications. Additionally, HeadPowder provides ongoing maintenance and support services to help clients maintain the system's performance over time. This includes regular inspections, component replacement, and troubleshooting to prevent unexpected failures and extend the system's lifespan. By choosing a system from HeadPowder, you can be confident that your glucose handling process will be supported by a reliable and efficient conveying solution that meets your long-term operational needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top