When it comes to managing the transportation of potash fertilizer, selecting the appropriate pneumatic conveying system is crucial for ensuring efficiency, safety, and cost-effectiveness in your processing operations. Potash, a key component in modern agriculture, requires specialized handling equipment to maintain its quality and prevent material degradation during transport. This article will guide you through the essential considerations and factors to evaluate when choosing a pneumatic conveying system tailored to your potash fertilizer handling process, with insights from industry experts at Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for bulk material handling.
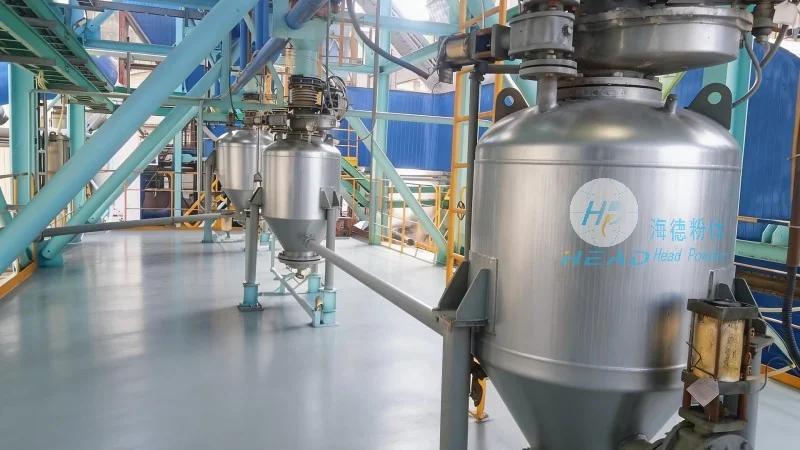
Potash fertilizer, primarily composed of potassium chloride (KCl), is a critical nutrient for enhancing crop yields and soil fertility. Its handling demands careful attention due to its granular or powder form, which can be prone to dust generation and segregation if not managed properly. Pneumatic conveying systems offer a non-contact, enclosed method of transporting bulk materials like potash, minimizing contamination risks and preserving product integrity. Unlike traditional belt or bucket elevators, these systems use air pressure to move material through pipelines, reducing the need for manual handling and improving operational safety.
Choosing the right pneumatic conveying system for potash fertilizer involves evaluating several critical factors that directly impact system performance and longevity. The first consideration is the type of system: positive pressure, negative pressure, or a combination of both. Positive pressure systems, where air is forced through the material, are ideal for applications requiring high material flow rates and long-distance transport, as they can handle larger volumes with less pressure drop. Negative pressure systems, on the other hand, draw material into the system using suction, which is suitable for short distances and applications where dust control is paramount. For potash fertilizer, which often requires both high throughput and strict dust containment, a hybrid or positive pressure system may be the optimal choice.
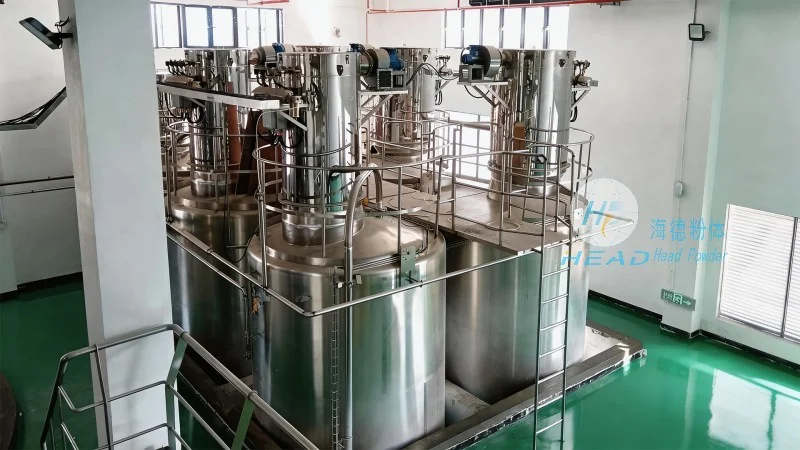
Another critical factor is the material's characteristics, including its bulk density, flowability, and moisture content. Potash fertilizer typically has a bulk density ranging from 0.8 to 1.2 tons per cubic meter, and its flowability can vary based on particle size and moisture levels. Systems must be designed to accommodate these variations to prevent blockages or uneven flow. For example, a system with adjustable air velocity and pressure control can adapt to different potash formulations, ensuring consistent performance. Additionally, the system's capacity and scalability are essential, as potash processing facilities may expand over time. A modular design that allows for easy expansion without disrupting existing operations is a significant advantage.
Potash fertilizer handling presents unique challenges, such as dust generation, material segregation, and the need for precise dosing. Pneumatic conveying systems address these challenges through advanced features like dust collection systems, which capture and filter air emissions, ensuring compliance with environmental regulations. The enclosed pipeline design also prevents cross-contamination between different potash batches, maintaining product purity. Furthermore, modern systems incorporate sensors and automation controls to monitor flow rates, pressure, and material levels in real-time, enabling proactive maintenance and reducing downtime. For instance, a system equipped with a variable frequency drive (VFD) can adjust air pressure dynamically based on the material's flow characteristics, optimizing energy consumption while maintaining performance.
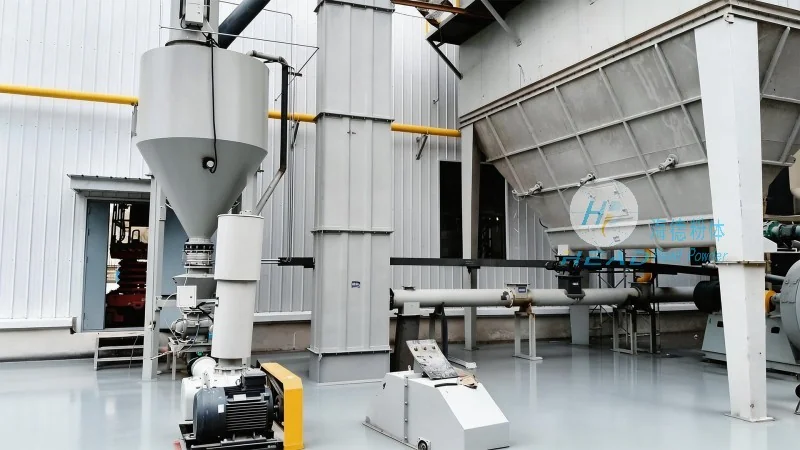
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in providing customized pneumatic conveying solutions for potash fertilizer and other bulk materials. With years of experience in the engineering sector, the company understands the unique demands of potash processing and offers tailored systems that meet specific operational requirements. Their expertise lies in designing systems that balance efficiency, reliability, and cost-effectiveness, ensuring that clients achieve optimal performance in their fertilizer handling processes. The company's team of engineers works closely with clients to assess their current infrastructure, material characteristics, and production goals, developing solutions that address both immediate needs and long-term growth. By leveraging advanced technology and industry best practices, HeadPowder delivers systems that enhance productivity, reduce operational costs, and improve overall safety in potash fertilizer handling operations.
Selecting the right pneumatic conveying system for your potash fertilizer handling process is a strategic decision that impacts the efficiency and sustainability of your operations. By considering factors such as system type, material characteristics, capacity, and environmental compliance, you can choose a solution that meets your current and future needs. Working with experienced providers like Shandong HeadPowder Engineering Co., Ltd. ensures that you receive expert guidance and customized solutions tailored to your specific requirements. Ultimately, investing in the right pneumatic conveying system not only improves the handling of potash fertilizer but also contributes to the overall success and competitiveness of your agricultural or fertilizer processing business.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top