When it comes to transporting compound fertilizers, the choice of material handling technology plays a crucial role in determining operational efficiency, safety, and environmental impact. Pneumatic conveying systems have emerged as a leading solution for industries dealing with bulk solid materials, offering a range of benefits that traditional methods cannot match. This article explores the advantages of using pneumatic conveying for compound fertilizers, highlighting how it contributes to sustainable and high-performance material transport.
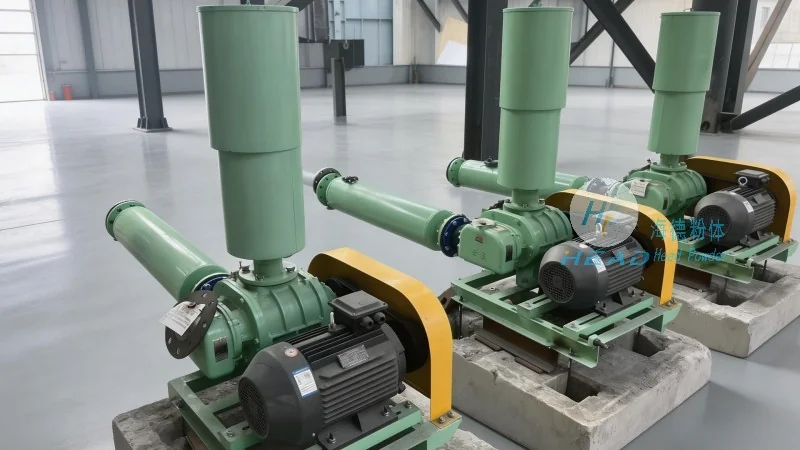
Efficiency in material transport is a primary concern for manufacturers and distributors of compound fertilizers. Pneumatic conveying systems excel in this regard by enabling rapid and continuous movement of bulk materials. Unlike mechanical conveying methods that may suffer from downtime due to maintenance or blockages, pneumatic systems operate with minimal interruptions, ensuring a steady flow of product. This not only boosts production throughput but also reduces labor costs associated with manual handling or frequent system adjustments.
Furthermore, the environmental benefits of pneumatic conveying are significant. By eliminating the need for conveyor belts, buckets, or other mechanical components that can generate dust or require lubrication, these systems minimize pollution and health hazards. The enclosed nature of pneumatic conveying also prevents dust from escaping into the environment, aligning with modern environmental regulations and sustainability goals. For companies operating in regions with strict environmental standards, this feature is particularly valuable, as it helps maintain compliance while reducing operational risks.
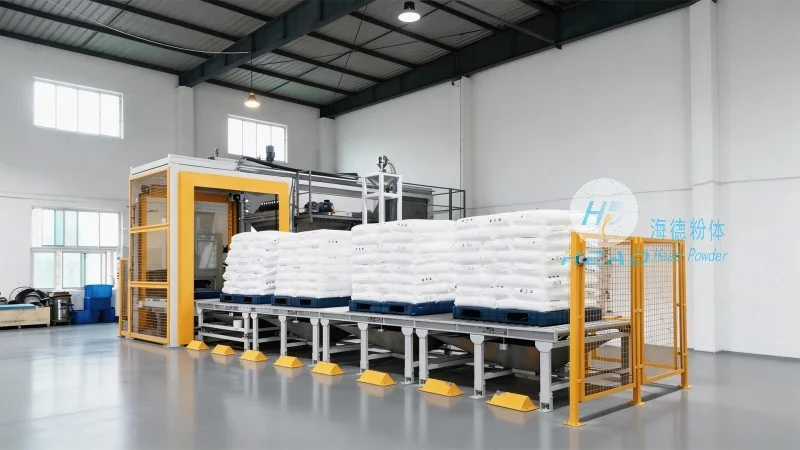
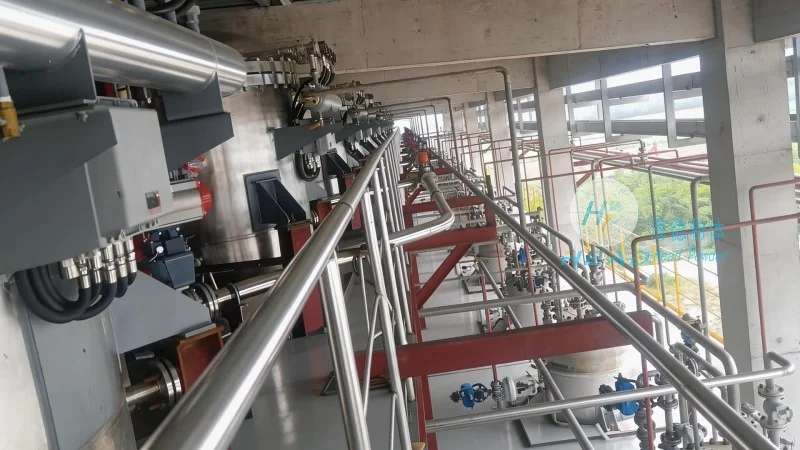
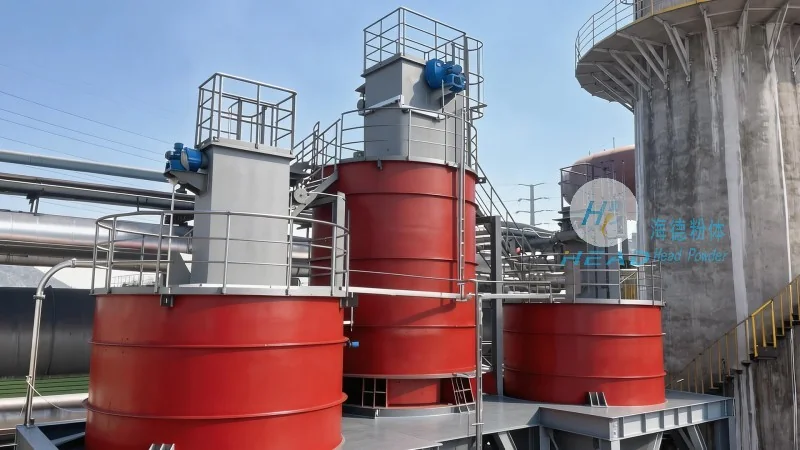
Understanding the mechanics of pneumatic conveying is essential for appreciating its effectiveness in handling compound fertilizers. At its core, a pneumatic conveying system uses air pressure to move material through a pipeline. The process typically involves a hopper or storage silo where the fertilizer is stored, a blower or compressor that generates the air flow, and a pipeline network that transports the material to its destination. The system can be designed as either positive pressure (where air pushes the material) or negative pressure (where air pulls the material), depending on the specific application and distance requirements.
For compound fertilizers, which often consist of a mix of granules, powders, and other additives, the flexibility of pneumatic conveying is a key advantage. The system can handle a wide range of particle sizes and compositions without causing segregation or degradation of the product. This is particularly important in maintaining the quality of the fertilizer, as improper handling can lead to clumping or loss of nutrients. The enclosed system also prevents moisture absorption or contamination from external sources, ensuring that the product remains in optimal condition throughout the transport process.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions tailored to the needs of the compound fertilizer industry. With years of experience and a deep understanding of the challenges faced by manufacturers, HeadPowder specializes in designing, manufacturing, and installing pneumatic conveying systems that meet the highest standards of efficiency and reliability. The company's commitment to innovation and customer satisfaction has made it a trusted name in the industry, serving clients across China and beyond.
HeadPowder's team of experts works closely with clients to assess their specific requirements, from production capacity to space constraints and environmental considerations. By leveraging cutting-edge technology and robust engineering, the company develops customized solutions that optimize material flow, reduce energy consumption, and enhance overall operational performance. Whether it's a new plant setup or an upgrade to an existing system, HeadPowder offers comprehensive support, including design, installation, and after-sales service, ensuring that clients receive a solution that is both effective and durable.
HeadPowder's headquarters is located in Shandong, China, a region known for its strong industrial base and expertise in chemical and agricultural equipment manufacturing. The company's facilities are equipped with state-of-the-art equipment and skilled technicians, enabling it to deliver high-quality products and services efficiently. By choosing HeadPowder, clients gain access to a partner with a proven track record of success, backed by a team dedicated to excellence and customer success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top