HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing advanced material handling solutions. Among their offerings is the airflow conveying system designed specifically for oat flour, a technology that combines efficiency with environmental sustainability. This article explores the benefits, applications, and technical aspects of using air-based systems for transporting oat flour, highlighting how such solutions can enhance operational performance while minimizing ecological impact.
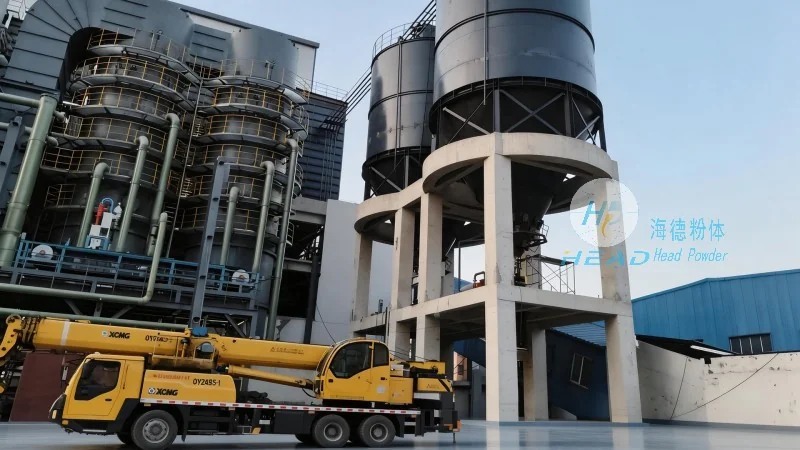
The airflow conveying system for oat flour operates on the principle of pneumatic transport, where a stream of air is used to move the material through a pipeline. Unlike traditional mechanical conveying methods, which rely on belts, screws, or buckets, air-based systems utilize compressed air to create a low-pressure or high-pressure environment that propels the oat flour particles. This method is particularly effective for handling fine powders like oat flour, as it minimizes product degradation and prevents contamination. The system typically consists of a hopper, a rotary valve, a pipeline network, and a receiver, all working in tandem to ensure a continuous and controlled flow of the material.
One of the primary advantages of the airflow conveying solution for oat flour is its high efficiency in material transport. The system can handle large volumes of oat flour with minimal energy consumption compared to traditional methods. The pneumatic transport mechanism allows for a uniform flow rate, reducing the risk of blockages or uneven distribution that often occur with mechanical conveyors. Additionally, the air-based system enables faster start-up and shutdown times, making it ideal for dynamic production environments where demand fluctuates. HeadPowder’s engineering expertise ensures that the system is optimized for the specific characteristics of oat flour, such as its particle size and moisture content, to maximize throughput and minimize downtime.
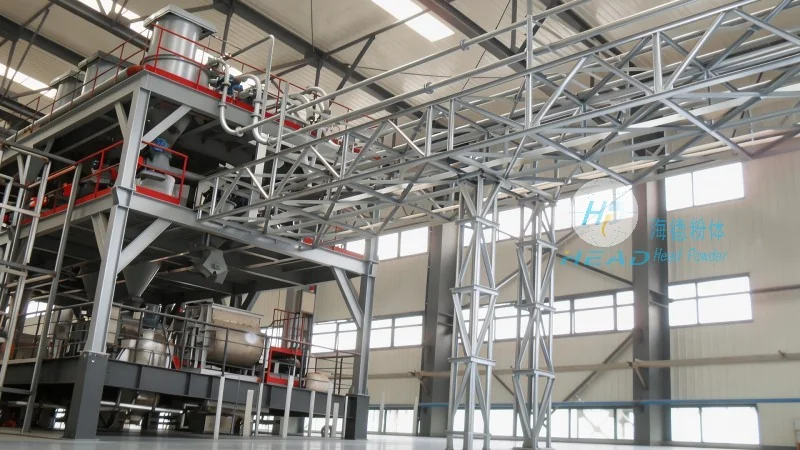
Environmental considerations are a key focus for HeadPowder’s airflow conveying solutions. By eliminating the need for mechanical components that generate friction and wear, the system reduces energy consumption and operational costs. The use of compressed air as the primary motive force also minimizes the generation of noise and dust, contributing to a cleaner working environment. Furthermore, the system’s design incorporates features like dust collection and air filtration, which help to control emissions and maintain compliance with environmental regulations. For oat flour processing facilities, this translates into a reduced carbon footprint and a more sustainable operation, aligning with global trends toward eco-friendly industrial practices.
The airflow conveying system is versatile and can be applied in various stages of oat flour processing. It is commonly used for transporting raw oat flour from storage silos to processing units, as well as for moving finished products to packaging lines. The system is also suitable for handling intermediate products, such as milled or ground oat flour, where precision and minimal product loss are critical. HeadPowder has successfully implemented these systems in both small-scale and large-scale oat flour production facilities, demonstrating its adaptability to different production capacities. The technology is particularly beneficial for facilities that require a hygienic and dust-free environment, as the enclosed pipeline system prevents contamination from external sources.
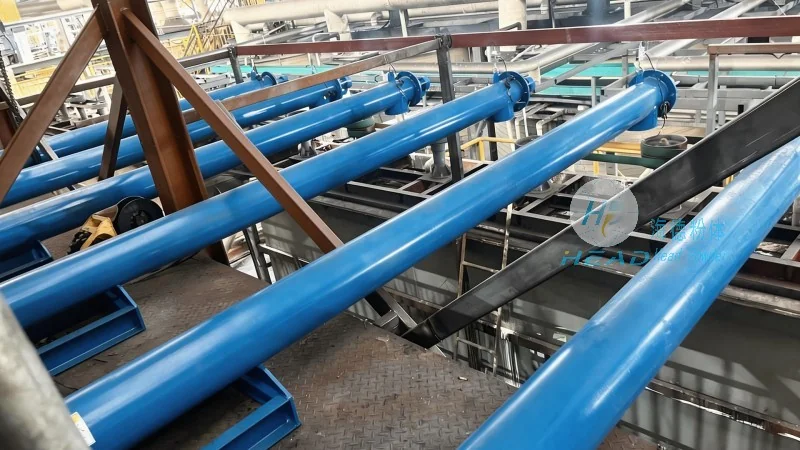
HeadPowder offers customizable airflow conveying solutions tailored to the specific needs of oat flour processing facilities. The system can be designed with different pressure levels, pipeline diameters, and material handling capacities to suit the production scale. For example, low-pressure systems are suitable for short-distance transport, while high-pressure systems are ideal for longer distances or when dealing with more challenging materials. The company’s engineers work closely with clients to assess their operational requirements and recommend the most appropriate configuration. Additionally, the system can be integrated with other processing equipment, such as mixers or classifiers, to create a seamless material handling workflow. HeadPowder’s commitment to quality and innovation ensures that their airflow conveying solutions are not only efficient but also durable and reliable, providing long-term value to their clients.
In conclusion, the airflow conveying system for oat flour represents a cutting-edge solution that combines efficiency, sustainability, and reliability. HeadPowder, with its headquarters in Shandong, China, has established itself as a trusted provider of such advanced material handling technologies. By leveraging pneumatic transport principles, the system offers significant advantages over traditional methods, including reduced energy consumption, minimized product degradation, and enhanced environmental performance. The company’s expertise in engineering and customization ensures that clients receive tailored solutions that meet their specific operational needs. As the demand for sustainable and efficient processing technologies grows, HeadPowder’s airflow conveying solutions for oat flour are poised to play a vital role in the future of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top