When it comes to efficiently transporting dry sand materials, the design of a pneumatic conveying system is crucial for ensuring optimal performance, reliability, and cost-effectiveness. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in creating tailored solutions that meet the unique needs of various industrial applications. This article provides a comprehensive guide on how to design a reasonable dry sand pneumatic conveying system, incorporating key considerations and best practices to achieve successful implementation.
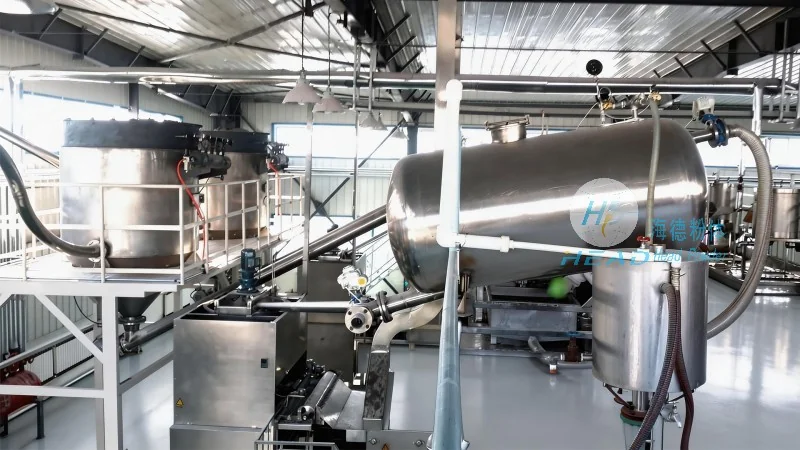
Before diving into the design process, it is essential to grasp the fundamental principles of pneumatic conveying for dry sand. Pneumatic conveying systems utilize air or gas to transport bulk materials through a network of pipes. For dry sand, which typically has a relatively low moisture content and moderate particle size, the system design must account for factors such as material density, flowability, and the presence of any cohesive properties. The choice between positive pressure, negative pressure, or a combination of both depends on the specific material characteristics and the distance the sand needs to be transported.
Designing an effective dry sand pneumatic conveying system involves several critical considerations that directly impact system performance and longevity. First, the selection of the appropriate conveying method is paramount. Positive pressure systems, where air is blown into the system to push the material, are commonly used for dry sand due to their ability to handle abrasive materials and maintain consistent flow rates. Negative pressure systems, on the other hand, draw material into the system using suction, which is often preferred for applications requiring minimal dust generation. The decision between these methods should be based on the material's properties, the distance to be covered, and the environmental requirements of the operation.
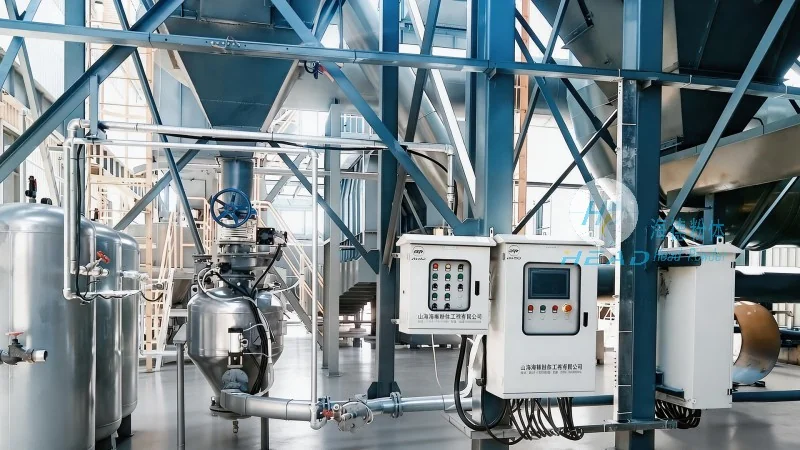
Second, the design of the pipeline network is a critical aspect. The diameter and length of the pipes must be carefully calculated to ensure adequate air velocity to prevent material settling or blockages. For dry sand, a typical air velocity of 20-30 meters per second is recommended to maintain a consistent flow. The use of bends, elbows, and other fittings must be minimized to reduce pressure losses and prevent material accumulation. Additionally, the material of the pipes—such as stainless steel or PVC—should be selected based on the sand's corrosiveness and the system's operating pressure.
A pneumatic conveying system for dry sand consists of several key components, each playing a vital role in the overall operation. The primary components include the material feeder, which ensures a consistent flow of dry sand into the system; the air compressor or blower, which provides the necessary pressure or suction; the conveying line, which transports the material; and the receiver or discharge unit, where the sand is collected. The material feeder is typically a screw feeder or a rotary valve, designed to handle dry sand without causing blockages or excessive wear. The air compressor must be capable of delivering the required air volume and pressure, with considerations for energy efficiency and noise levels. The conveying line must be properly sized and supported to prevent sagging or vibration, which could lead to material degradation or system failure.
Accurate calculation of air requirements is essential for the efficient operation of a dry sand pneumatic conveying system. The air volume needed depends on the material's flow rate, the system's length, and the air velocity chosen. A general rule of thumb is to use an air velocity of 20-30 m/s for dry sand, which translates to an air volume of approximately 0.5-1.0 cubic meters per second per ton of material. The pressure level, whether positive or negative, must be sufficient to overcome the resistance of the pipeline and any elevation changes. For positive pressure systems, the pressure is typically maintained at 0.5-1.0 bar above atmospheric pressure, while negative pressure systems may operate at -0.2 to -0.5 bar. Proper calculation of these parameters ensures that the system operates within its optimal range, minimizing energy consumption and maximizing material throughput.
Blockages are a common issue in pneumatic conveying systems, especially when handling dry sand. To prevent this, several design strategies are employed. First, the use of a filter and cyclone separator is crucial to remove any dust or fine particles that could accumulate and cause blockages. The filter must be regularly maintained to ensure it operates effectively. Second, the system should be equipped with a pressure relief valve to prevent over-pressurization and potential damage to components. Additionally, the inclusion of a venturi or other flow-enhancing devices can help maintain consistent air velocity and prevent material settling. Regular maintenance and monitoring of the system's pressure and flow rates are also essential to identify and address any potential issues before they escalate into blockages or system failures.
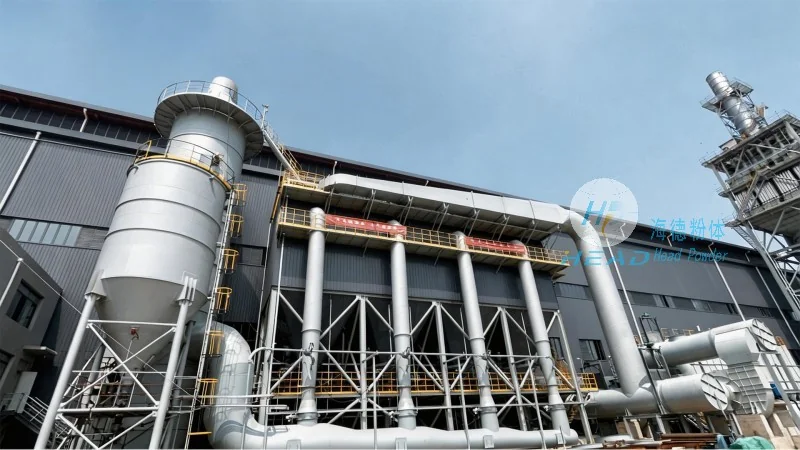
When designing a dry sand pneumatic conveying system, environmental and safety considerations are paramount. The system should be designed to minimize dust emissions, which can pose health risks and environmental hazards. This can be achieved through the use of sealed components, such as the material feeder and discharge unit, and the incorporation of dust collection systems. Additionally, the system must comply with local regulations regarding noise levels and material handling. Safety features, such as emergency shut-off valves and pressure relief devices, should be included to protect operators and prevent accidents. The selection of materials for the system components, such as stainless steel for the pipes and fittings, can also enhance durability and reduce the risk of corrosion or contamination.
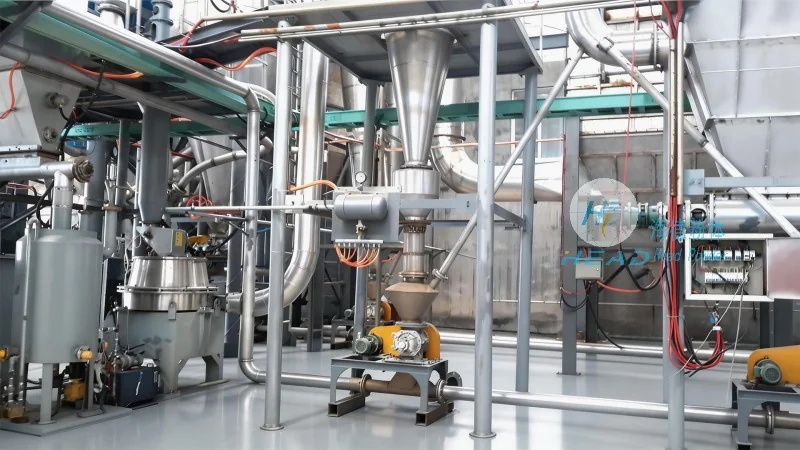
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented numerous dry sand pneumatic conveying systems for various industrial applications. One notable case involved a construction materials company that needed to transport dry sand from a storage silo to a mixing plant over a distance of 100 meters. The system was designed as a positive pressure system with a stainless steel pipeline network and a rotary valve feeder. The air compressor was sized to deliver 0.8 cubic meters per second of air at 0.8 bar pressure. The system was able to maintain a consistent flow rate of 5 tons per hour, with minimal blockages and low energy consumption. The customer reported significant improvements in production efficiency and reduced labor costs associated with manual material handling.
Designing a reasonable dry sand pneumatic conveying system requires a thorough understanding of the material properties, the system requirements, and the operational constraints. By following the key considerations outlined in this article, including proper component selection, accurate air requirement calculations, and effective maintenance strategies, industrial facilities can achieve efficient and reliable material transport. Shandong HeadPowder Engineering Co., Ltd. offers expert design and implementation services to help clients develop tailored pneumatic conveying solutions that meet their specific needs. Whether for construction, mining, or other industries, a well-designed dry sand pneumatic conveying system can provide significant benefits in terms of productivity, cost savings, and operational safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top