For coffee processing facilities, efficient and reliable handling of coffee powders is crucial to maintaining product quality and operational efficiency. The coffee powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these needs through a well-designed structure and advanced working principles. This article provides an overview of the system's components, operational mechanics, and key features that make it suitable for coffee processing applications.
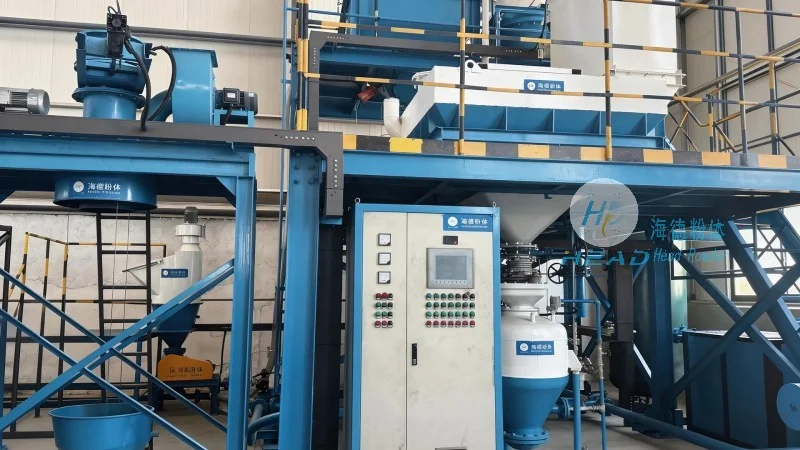
The coffee powder conveying system is engineered to handle the unique characteristics of coffee powders, such as their fine particle size, hygroscopic nature, and potential for static charge accumulation. HeadPowder's system is designed to ensure minimal product degradation while maintaining high throughput rates. The system integrates multiple components that work in tandem to achieve seamless material transport from storage to processing or packaging stages.
The system's structure comprises several critical components, each playing a vital role in the overall conveying process. These include:
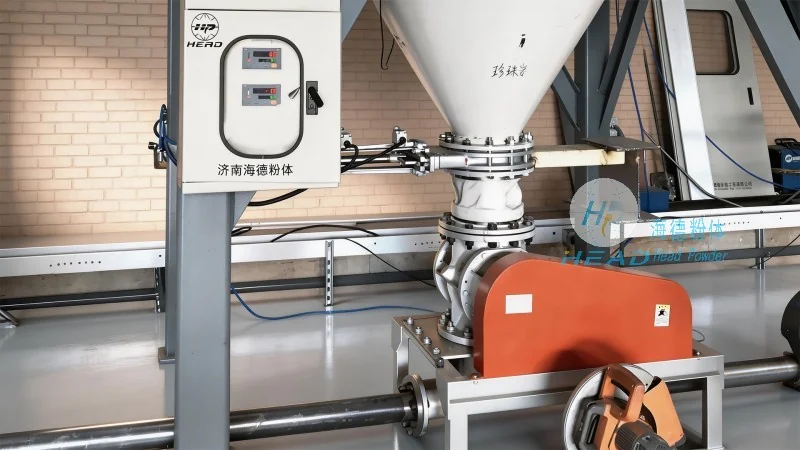
The operation of the coffee powder conveying system follows a systematic sequence of steps, leveraging both mechanical and pneumatic forces to move the material efficiently. The process begins with the coffee powder being discharged from the storage hopper into the feeding mechanism. The feeder then regulates the flow rate, ensuring a steady supply of material into the pneumatic conveying line.
Compressed air is introduced into the line, creating a flow that entrains the coffee powder particles. As the air moves through the pipes, it carries the powder along, overcoming gravitational and frictional forces. The system's design minimizes particle impact and abrasion, which are common issues in traditional mechanical conveyors. The use of a filter at the end of the line prevents dust and fine particles from escaping, maintaining a clean and safe working environment.
HeadPowder's coffee powder conveying system offers several advantages that make it an ideal choice for coffee processing facilities. These include:
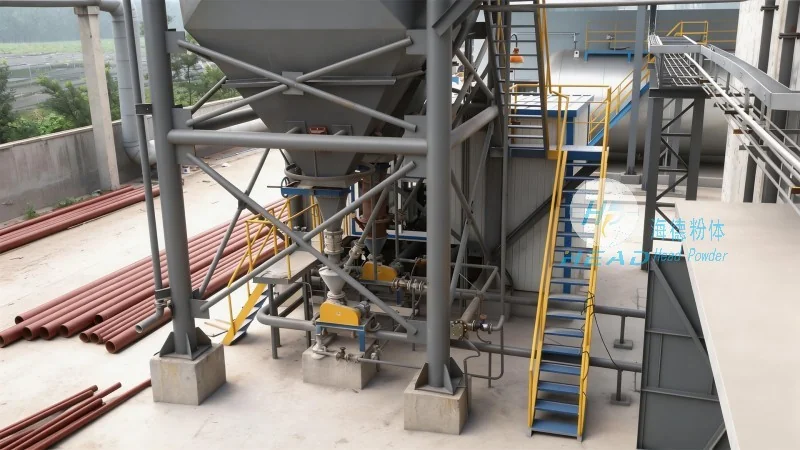
The coffee powder conveying system is widely used in various stages of coffee processing, from raw material handling to final product packaging. In the storage and transfer phase, the system efficiently moves coffee powders from storage silos to production lines. During blending, the system can distribute different coffee varieties or additives with precision. Finally, in the packaging stage, the system delivers the final product to filling machines, ensuring consistent and reliable operation.
Shandong HeadPowder Engineering Co., Ltd.'s coffee powder conveying system represents a sophisticated solution for the efficient and hygienic handling of coffee powders. By integrating advanced structural components and pneumatic conveying technology, the system addresses the unique challenges of coffee processing while maintaining high product quality and operational efficiency. For coffee processing facilities seeking to optimize their material handling processes, this system offers a reliable and effective solution.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top