For industries dealing with rice powder, efficient and reliable conveying systems are crucial for maintaining product quality and operational efficiency. This article provides an overview of rice powder conveying systems, focusing on their structural design and fundamental working principles. The systems are engineered to handle the unique properties of rice powder, such as its fine particle size, hygroscopic nature, and potential for dust generation, ensuring safe and effective material transport.
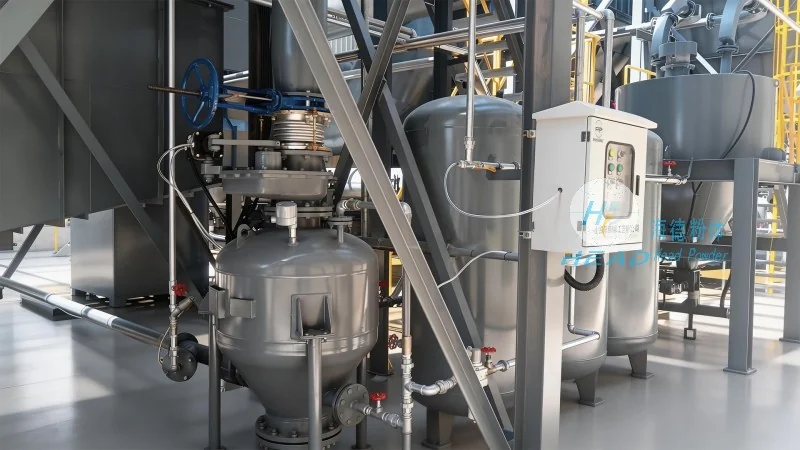
The rice powder conveying system typically consists of several key components that work in tandem to facilitate smooth material movement. The primary components include a hopper for material storage, a feeding mechanism to control the flow of powder, a conveying pipeline (often made of stainless steel or food-grade materials to prevent contamination), and a drive system to generate the necessary force for transport. The hopper is designed with a sloped bottom to minimize material bridging and ensure consistent flow. The feeding mechanism, such as a rotary valve or screw feeder, regulates the amount of powder entering the pipeline, preventing overloading and maintaining stable conveying rates. The pipeline is usually equipped with bends and elbows that are carefully designed to minimize pressure drop and prevent powder accumulation or blockages. The drive system, which may include a motor and gearbox, provides the power to move the powder through the system, with adjustable speed controls to accommodate varying production demands.
The conveying process in a rice powder system operates based on the principles of pneumatic or mechanical transport. In pneumatic conveying systems, air is used to create a flow of powder within the pipeline. The system may use positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out). The air velocity is carefully controlled to ensure that the powder particles are suspended and transported without causing excessive wear or degradation of the material. Mechanical conveying systems, on the other hand, rely on mechanical devices like screws or belts to move the powder. These systems are often more suitable for bulk material handling and can handle higher capacities. The working principle involves the rotation of the conveying element, which pushes the powder forward through the pipeline. Both pneumatic and mechanical systems are designed to maintain the integrity of the rice powder, preventing clumping, agglomeration, or contamination during transport.
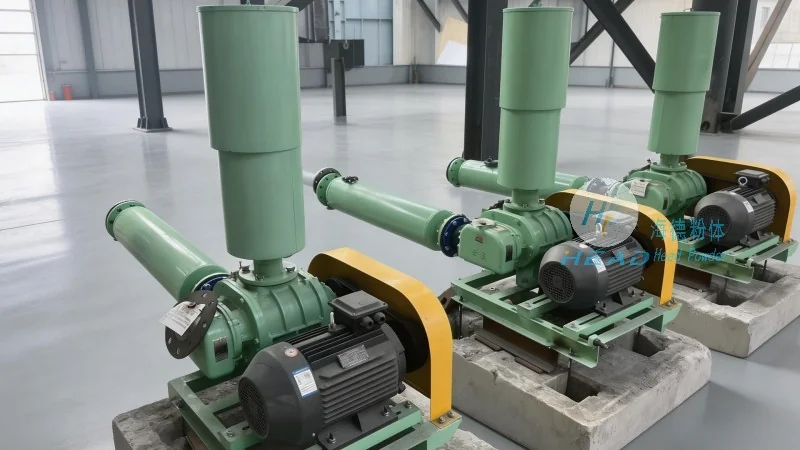
Implementing a rice powder conveying system offers several advantages for industrial applications. Firstly, it enhances operational efficiency by automating the material transport process, reducing manual labor and the risk of human error. The system’s ability to handle fine powders without clogging or blockages ensures consistent production rates and minimizes downtime. Secondly, the use of food-grade materials and sealed systems helps maintain product purity and compliance with food safety regulations. This is particularly important for rice powder, which is often used in food processing and pharmaceutical applications. Thirdly, the system’s design allows for easy integration with other processing equipment, such as mixers, classifiers, or packaging machines, creating a seamless production line. Additionally, the adjustable speed controls enable flexibility in production, allowing manufacturers to scale up or down based on demand without significant modifications to the system.
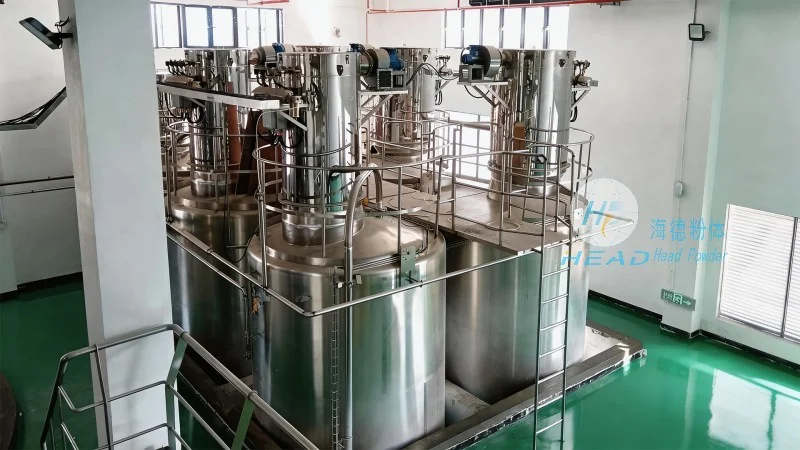
Rice powder conveying systems are widely used in various industries that process rice-based products. In the food industry, these systems are commonly employed in rice milling facilities to transport ground rice powder from storage silos to processing lines, such as for making rice flour, rice bran oil, or instant rice products. The systems ensure that the powder is delivered to the processing equipment in a controlled manner, maintaining the quality of the final product. In the pharmaceutical industry, rice powder is used as an excipient or filler in drug formulations, and the conveying system helps transport the powder to mixing and packaging equipment, ensuring accurate dosing and preventing contamination. Similarly, in the agricultural and animal feed sectors, rice powder is used as a nutrient source, and the conveying system facilitates its transport from storage to feed mixing plants. The versatility of the system makes it suitable for a range of applications, from small-scale operations to large industrial facilities.
To ensure the long-term performance and reliability of the rice powder conveying system, proper maintenance and operational considerations are essential. Regular cleaning of the hopper, pipeline, and feeding mechanisms is crucial to prevent the buildup of powder residue, which can lead to clogging or contamination. The use of appropriate cleaning agents and tools, such as brushes or compressed air, helps maintain the system’s efficiency. Additionally, monitoring the system’s performance parameters, such as pressure, flow rate, and temperature, can help identify potential issues before they escalate. Regular inspection of the drive system and conveyor components for wear and tear is also necessary to prevent breakdowns and ensure safe operation. Proper training of operators on the system’s operation and maintenance procedures is vital to maximize its lifespan and minimize downtime. By following these guidelines, manufacturers can ensure that the rice powder conveying system operates efficiently and reliably, meeting the demands of their production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top