HeadPowder, a professional enterprise based in Shandong, China, specializes in the design, manufacturing, and supply of advanced powder handling systems. This article provides an overview of the borax powder conveying systems, focusing on their structural design and operational principles to help users understand the technology behind efficient borax powder transportation.
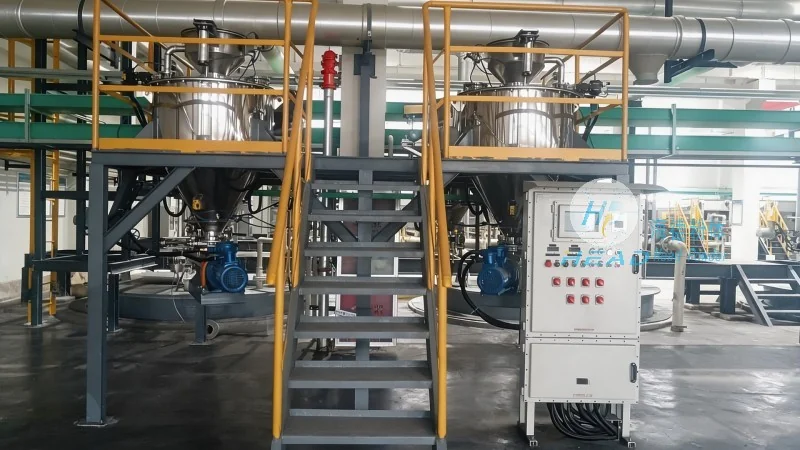
Borax powder conveying systems are critical in industrial applications where borax, a white crystalline powder with chemical formula Na₂B₄O₇·10H₂O, needs to be transported from storage to processing units. The efficiency and reliability of these systems directly impact production throughput and operational costs. HeadPowder's expertise lies in developing customized solutions that address the unique challenges associated with handling borax powder, such as its hygroscopic nature and potential for caking.
The core components of a borax powder conveying system typically include a hopper for material storage, a feeder to control the flow rate, a conveying mechanism (like a screw conveyor or pneumatic system), and a discharge unit. Each component is designed to work in harmony to ensure smooth and continuous material movement. The hopper is often equipped with a discharge gate or valve to regulate the amount of powder entering the feeder. The feeder, which may be a rotary valve or a volumetric feeder, ensures a consistent flow rate, preventing overloading or underloading of the conveying mechanism.
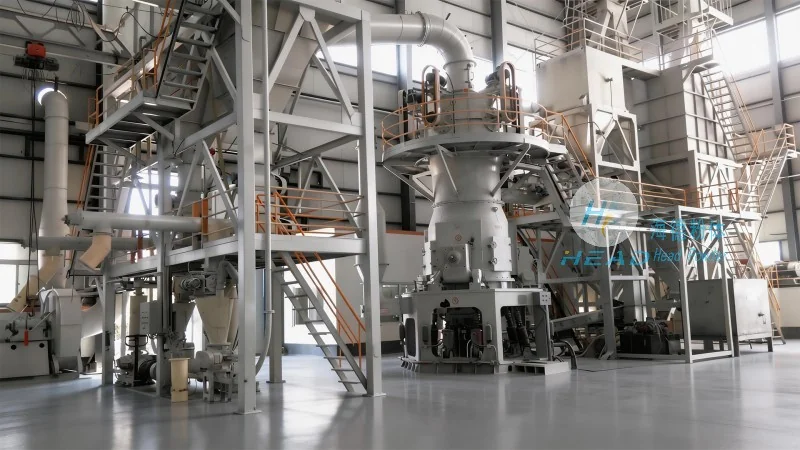
The conveying mechanism is the heart of the system. For borax powder, which is relatively fine and can be prone to dust generation, a screw conveyor is commonly used due to its ability to handle dry powders effectively. The screw, made of corrosion-resistant materials like stainless steel, rotates inside a trough, pushing the powder forward. The design of the screw, including its pitch and diameter, is optimized to minimize friction and prevent material buildup. In some applications, a pneumatic conveying system may be employed, using air pressure to transport the powder through a pipeline. This method is particularly useful for long-distance or high-volume transport but requires careful consideration of air flow rates and pressure to avoid particle degradation.
The operational principles of borax powder conveying systems revolve around maintaining a stable and controlled flow of material. The system is typically controlled by a combination of mechanical and electronic components. Sensors, such as level detectors in the hopper and flow meters in the conveying line, monitor the material levels and flow rates in real-time. These sensors send signals to the control panel, which adjusts the feeder speed or air pressure as needed to maintain optimal conditions. For example, if the hopper level drops below a certain threshold, the control system may increase the feeder speed to prevent downtime. Conversely, if the flow rate is too high, it may reduce the speed to avoid overloading the downstream equipment.
The control system also plays a crucial role in ensuring safety and preventing equipment damage. It may include features like overload protection, which shuts down the system if the conveying mechanism is overloaded, and dust suppression measures, such as using sealed hoppers and conveying lines to minimize dust emissions. These features are essential for maintaining a safe working environment and complying with industrial safety regulations.
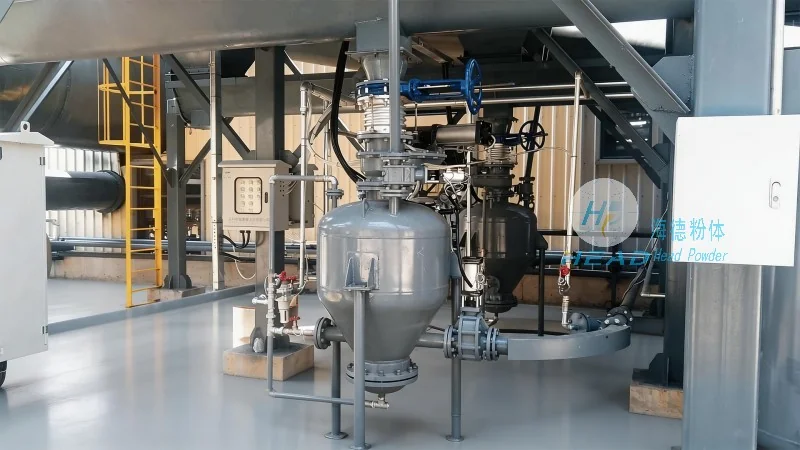
HeadPowder's borax powder conveying systems offer several advantages that make them suitable for various industrial applications. The systems are designed for high efficiency, with minimal material loss and low energy consumption. The use of corrosion-resistant materials ensures long service life, reducing maintenance costs and downtime. Additionally, the systems are highly customizable, allowing HeadPowder to tailor solutions to specific customer requirements, such as varying production capacities or unique facility layouts.
The company's expertise in powder handling technology, combined with its understanding of borax's physical properties, results in systems that are both reliable and cost-effective. By leveraging advanced engineering and quality control processes, HeadPowder ensures that its borax powder conveying systems meet the highest standards of performance and durability. This commitment to excellence has made HeadPowder a trusted partner for businesses in the chemical, pharmaceutical, and food industries, where efficient and safe powder handling is paramount.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top