Coal ash powder conveying is a critical process in the handling and transportation of coal ash, a byproduct of coal combustion. Efficient and reliable conveying systems are essential for industrial applications, ensuring safe and effective movement of this fine particulate material. This overview will explore the structural components and operational principles of coal ash powder conveying systems, highlighting the key elements that contribute to their functionality and performance.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of engineering solutions for powder handling and material transport. With a focus on innovation and precision, the company specializes in designing and manufacturing systems tailored to the unique challenges of coal ash and other fine powders. HeadPowder’s expertise lies in creating robust, efficient, and safe conveying systems that meet the demands of industrial clients, ensuring optimal performance and longevity in demanding environments. The company’s headquarters is located in Shandong, China, where it leverages local resources and industry knowledge to deliver high-quality products and services.
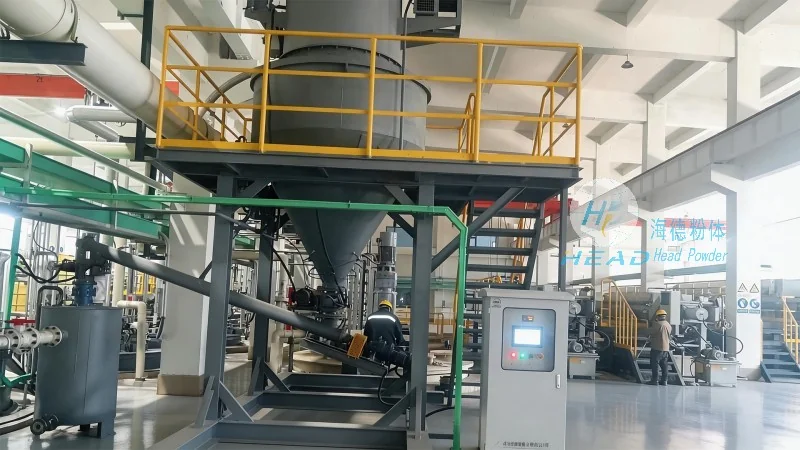
The coal ash powder conveying system consists of several critical components that work in tandem to facilitate the movement of the material. These components include the feed hopper, which stores and feeds the coal ash into the system; the conveyor itself, which can be pneumatic or mechanical depending on the application; and the discharge mechanism, which delivers the material to its destination. The feed hopper is designed to handle the bulk storage of coal ash, ensuring a consistent flow into the conveyor. It typically features a sloped bottom to prevent material buildup and includes a gate or valve for controlled discharge. The conveyor, whether pneumatic (air-based) or mechanical (e.g., screw or belt), is the core of the system, responsible for transporting the fine powder. Pneumatic conveying systems use compressed air to move the material through a pipeline, while mechanical systems rely on rotating components to push the powder forward. The discharge mechanism, such as a rotary valve or outlet, regulates the release of the material from the system, ensuring it is delivered to the intended location without spillage or loss.
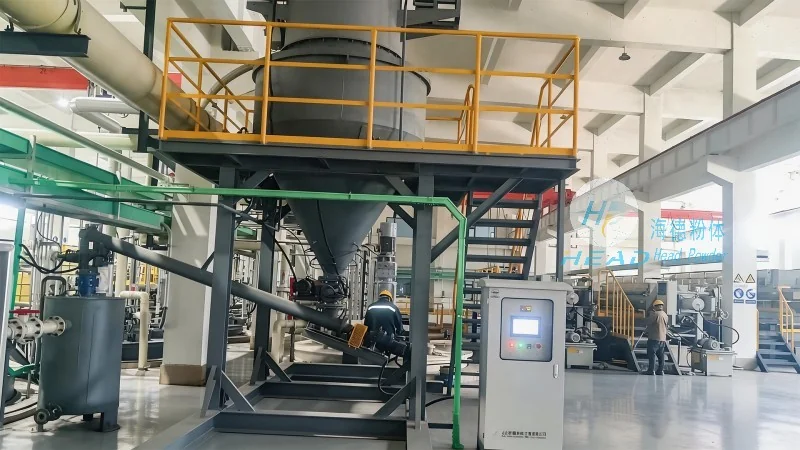
The operational principle of coal ash powder conveying systems is based on the physical properties of the material and the chosen conveying method. For pneumatic systems, the process involves creating a pressure differential between the feed and discharge points. Compressed air is introduced into the system, drawing the coal ash particles into the pipeline. The air velocity is carefully controlled to ensure the particles are suspended and transported without clogging or degradation. This method is particularly effective for fine powders like coal ash, as it minimizes particle breakage and maintains the material’s integrity. Mechanical systems, on the other hand, rely on the mechanical action of rotating components to move the material. For example, a screw conveyor uses a rotating screw to push the coal ash forward, while a belt conveyor uses a moving belt to transport the material. These systems are often preferred for bulkier or more abrasive materials, as they can handle higher capacities and provide more consistent flow. The working principle of both systems is to ensure the material is moved efficiently and safely from the source to the destination, minimizing downtime and operational costs.
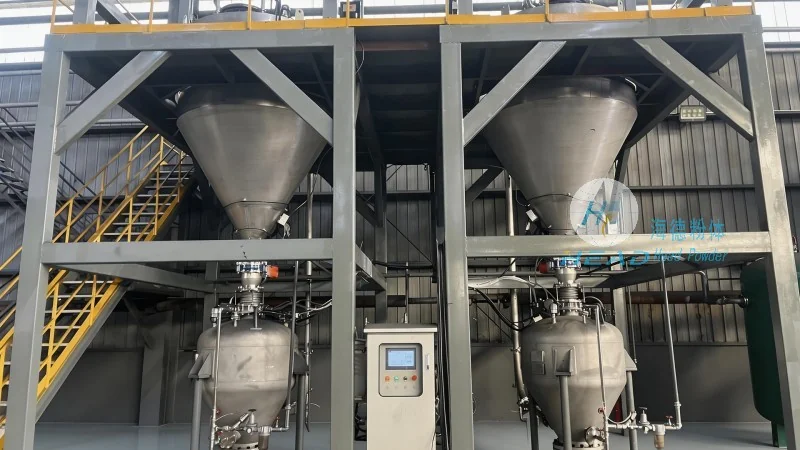
Coal ash powder conveying systems are widely used in various industrial applications, including power plants, cement manufacturing, and waste management facilities. In power plants, these systems are crucial for transporting coal ash from the boiler to storage or disposal sites, ensuring that the material is handled safely and in compliance with environmental regulations. In cement plants, coal ash is often used as a supplementary cementitious material, and efficient conveying systems are necessary to transport it to the mixing and processing areas. The benefits of using coal ash powder conveying systems include improved safety, reduced labor costs, and enhanced operational efficiency. By automating the material transport process, companies can minimize the risk of accidents and exposure to hazardous materials, while also increasing the speed and consistency of production. Additionally, these systems help to reduce the environmental impact of coal ash disposal by ensuring that the material is handled and transported in a controlled manner, preventing spills and contamination.
In conclusion, coal ash powder conveying systems play a vital role in the efficient handling and transportation of coal ash. The structural components and working principles of these systems are designed to ensure safe, reliable, and efficient operation, meeting the demands of industrial applications. HeadPowder, with its expertise in powder handling solutions, provides high-quality systems that are tailored to the unique needs of clients. By leveraging advanced engineering and local industry knowledge, HeadPowder ensures that its coal ash powder conveying systems deliver optimal performance and longevity. For industries relying on coal ash as a material, investing in a reliable conveying system is essential for maintaining operational efficiency and compliance with environmental standards. The future of coal ash handling will likely involve continued innovation in conveying technology, and companies like HeadPowder are at the forefront of developing solutions that meet these evolving needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top