HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for industrial applications. This article provides an overview of the desulfurization sodium bicarbonate pneumatic conveying system, detailing its equipment components, structural design, and operational principles.
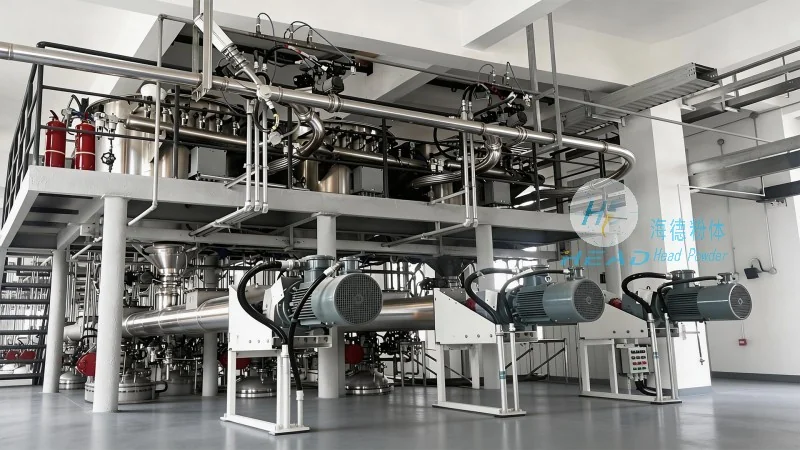
The desulfurization sodium bicarbonate pneumatic conveying system is engineered to efficiently transport sodium bicarbonate, a critical reagent in flue gas desulfurization processes, from storage to processing units. The system comprises several key components that work in tandem to ensure reliable and safe material handling. These include a storage silo, a feeder unit, a conveying pipeline network, a control system, and a dust collection system. Each component is carefully selected and integrated to meet the specific demands of the desulfurization process, ensuring optimal performance and minimal downtime.
The structural design of the pneumatic conveying system prioritizes durability, efficiency, and safety. The storage silo is constructed from high-strength materials, such as carbon steel or stainless steel, to withstand the corrosive nature of sodium bicarbonate and the environmental conditions of the industrial site. The silo is equipped with a level indicator and a discharge valve to regulate the flow of material. The feeder unit, typically a rotary valve or a screw feeder, is designed to provide a consistent and controlled feed rate, preventing blockages and ensuring smooth material flow into the conveying pipeline.
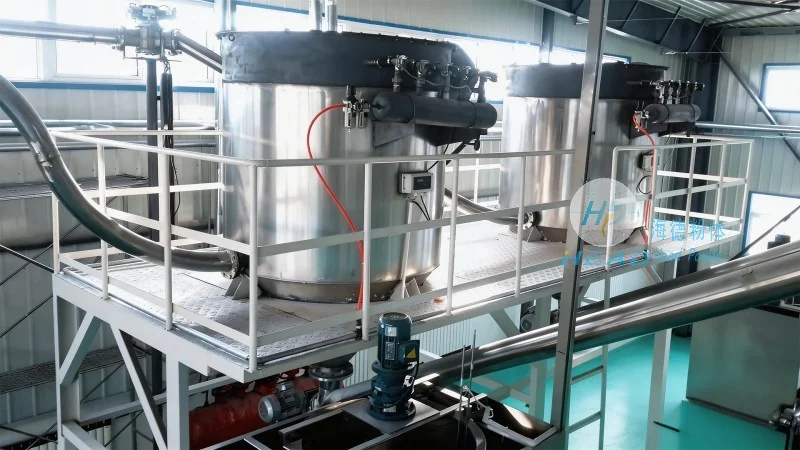
The conveying pipeline network is made of corrosion-resistant materials, such as PVC or stainless steel, to prevent degradation from the sodium bicarbonate and the presence of moisture or acidic gases. The system utilizes a positive pressure or negative pressure conveying method, depending on the specific application requirements. Positive pressure systems use a blower to force air and material through the pipeline, while negative pressure systems use a vacuum to draw material into the pipeline. The choice of method is determined by factors such as material properties, pipeline length, and system layout.
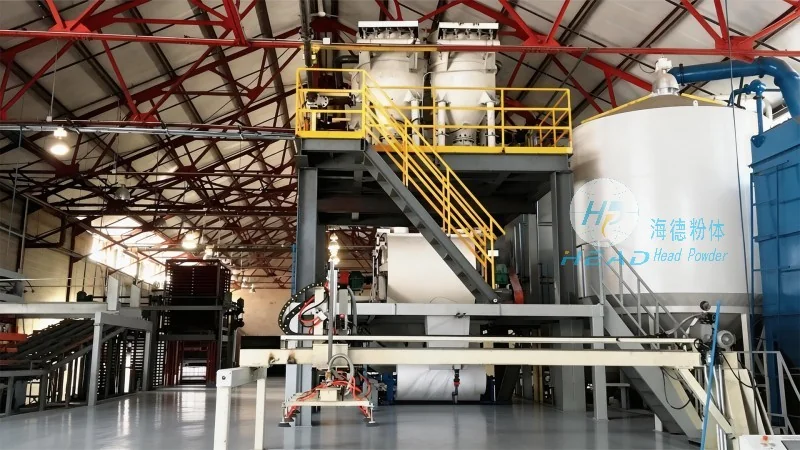
The control system of the pneumatic conveying system is a critical component that ensures the safe and efficient operation of the entire process. It includes sensors, controllers, and actuators that monitor and regulate the flow of material, air pressure, and temperature. The system is equipped with safety features, such as pressure relief valves and emergency shut-off valves, to prevent accidents and protect personnel and equipment. The control system also provides real-time data on system performance, allowing operators to make informed decisions and optimize the operation of the system.
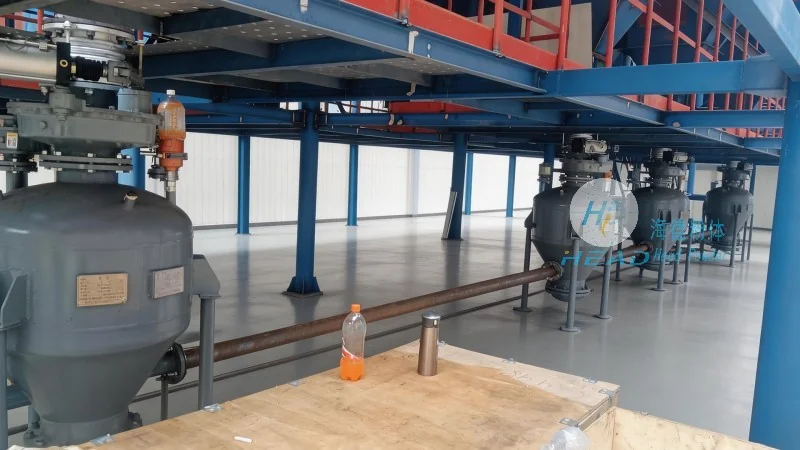
Due to the nature of the material being handled, the pneumatic conveying system is equipped with a dust collection system to ensure compliance with environmental regulations and to maintain a safe working environment. The dust collection system typically includes a cyclone separator and a baghouse filter, which remove dust particles from the air stream and collect them in a hopper for disposal. The system is designed to minimize dust emissions and to ensure that the air discharged from the system meets the required standards.
The desulfurization sodium bicarbonate pneumatic conveying system is widely used in power plants, chemical plants, and other industrial facilities that require the efficient handling of sodium bicarbonate for flue gas desulfurization. The system's ability to handle large volumes of material with minimal labor and maintenance makes it an ideal solution for these applications. By improving the efficiency of the desulfurization process, the system contributes to reduced emissions of sulfur dioxide and other pollutants, helping to protect the environment and comply with regulatory requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top