HeadPowder, an enterprise based in Shandong, China, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems tailored for the compound fertilizer industry. With a focus on innovation and precision engineering, the company has established itself as a trusted partner for clients seeking efficient and reliable solutions to handle bulk fertilizer materials. The company's commitment to quality and customer satisfaction is reflected in its state-of-the-art facilities and experienced technical team, ensuring that each system meets the specific requirements of fertilizer processing and transportation.
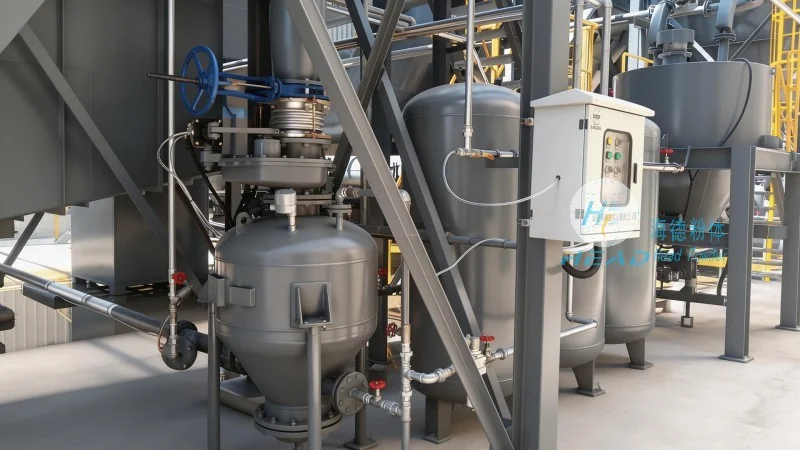
The compound fertilizer pneumatic conveying system is a comprehensive solution designed to transport bulk compound fertilizers from storage silos or production lines to processing units, packaging facilities, or storage areas. This system integrates multiple components that work in harmony to ensure smooth, efficient, and safe material handling. Key components typically include a feeding hopper, a rotary valve or screw feeder, a high-pressure air compressor, a filter system, and a network of stainless steel or corrosion-resistant pipelines. The system is engineered to handle various types of compound fertilizers, including granular, prilled, or powdered formulations, with different particle sizes, moisture contents, and bulk densities. By leveraging pneumatic technology, the system eliminates the need for mechanical conveyors, reducing wear and tear on equipment and minimizing the risk of material contamination.
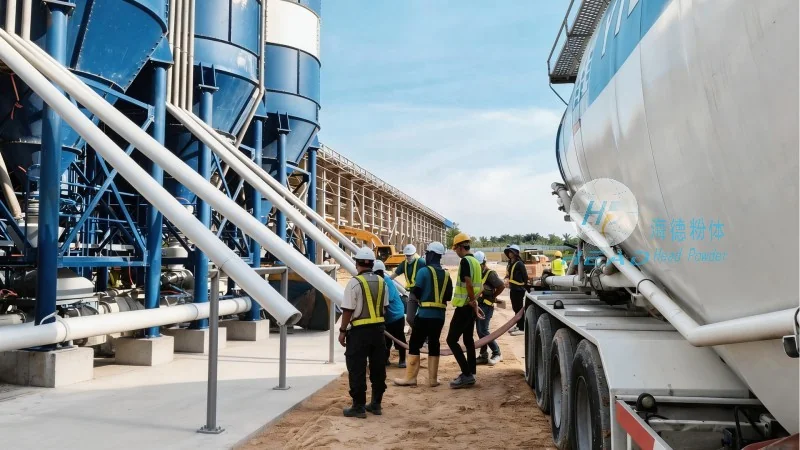
The structural design of the compound fertilizer pneumatic conveying system is optimized for durability, efficiency, and adaptability to diverse fertilizer characteristics. The feeding hopper is equipped with a heavy-duty rotary valve or screw feeder, which controls the flow rate of the fertilizer into the system. This component is critical for maintaining consistent material feed and preventing blockages. The high-pressure air compressor generates the necessary airflow to move the fertilizer particles through the pipeline. The compressor is typically equipped with a pressure regulator and a filter to ensure clean air, which is essential for preventing clogging and maintaining system performance. The pipeline network is constructed from stainless steel or other corrosion-resistant materials to withstand the chemical properties of fertilizers and resist wear from abrasive particles. The system includes a filter and dust collection unit at the receiving end to capture any fine particles and return them to the process, ensuring minimal material loss and environmental compliance. Control systems, often integrated with sensors and variable frequency drives, allow for real-time monitoring and adjustment of the conveying process, optimizing energy consumption and operational efficiency.
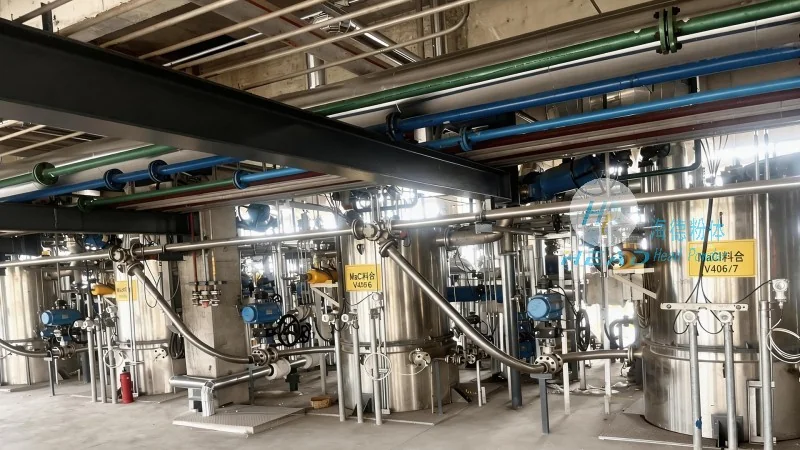
For fertilizer manufacturers, the pneumatic conveying system offers several advantages over traditional mechanical conveying methods. It reduces labor costs by automating the material handling process, minimizes material degradation due to reduced friction and impact, and improves overall production efficiency. The system's ability to handle different fertilizer types and formulations makes it versatile for various production lines. Additionally, the compact design of the equipment allows for easy integration into existing facilities, and the low maintenance requirements contribute to long-term cost savings. HeadPowder's systems are designed to meet international safety and environmental standards, ensuring compliance with regulations while providing reliable performance. By investing in a pneumatic conveying system from HeadPowder, clients can enhance their operational capabilities, improve product quality, and achieve greater productivity in the compound fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top