HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying systems tailored for the cement industry. This article provides an overview of the equipment used in cement particle pneumatic conveying systems, along with a detailed explanation of their structural principles and operational mechanisms.
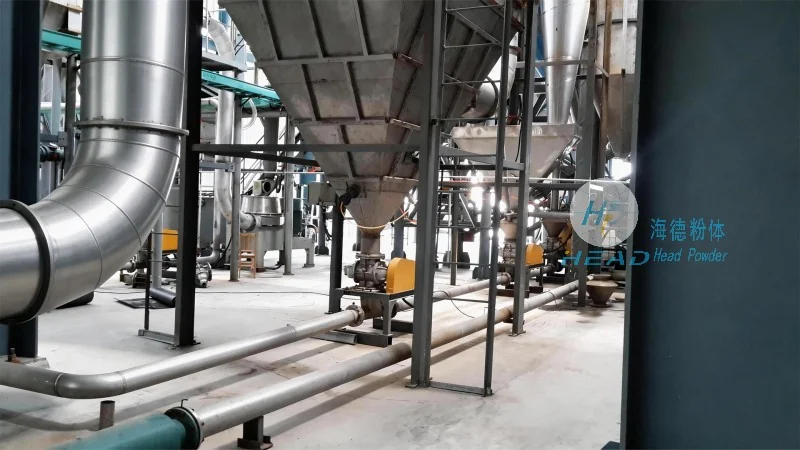
The cement particle pneumatic conveying system is a sophisticated industrial solution that enables the efficient and reliable transport of cement and other fine particulate materials. At the core of this system are several key components, each playing a crucial role in the overall conveying process. These components typically include a feeding device, a conveying pipeline, a gas supply system (air compressor or blower), a separation and collection unit, and a control system. The equipment is engineered to handle the unique challenges associated with cement, such as its high density, fine particle size, and potential for dust generation during transport.
The structural principle of a cement particle pneumatic conveying system revolves around the use of air as the conveying medium to transport solid particles. The system operates on the principle of creating a pressure differential between the inlet and outlet of the conveying pipeline. When air is introduced into the pipeline at a controlled pressure and velocity, it generates sufficient kinetic energy to lift and move the cement particles. The key structural elements include the feeding hopper, which ensures a consistent and controlled feed of cement into the system, and the conveying pipeline, which is often equipped with bends, valves, and other fittings to direct the flow and maintain system integrity.
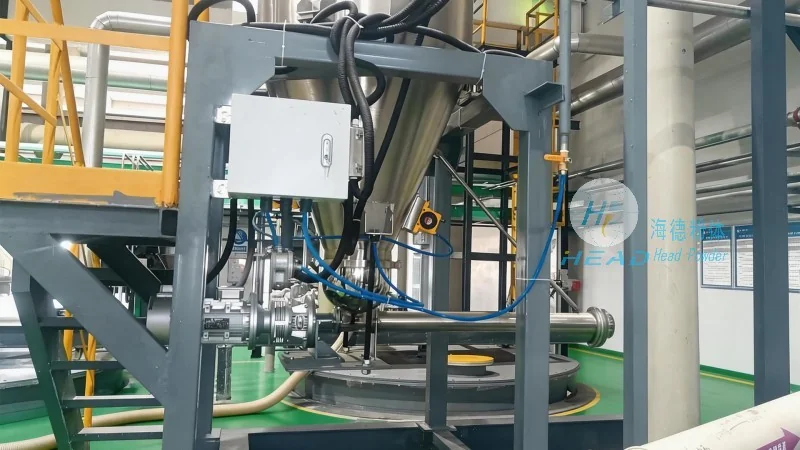
The operational mechanism of the cement particle pneumatic conveying system involves several sequential steps. First, the cement is fed from the storage silo or hopper into the feeding device, which may include a rotary valve or a screw feeder to regulate the flow rate. Next, the air compressor or blower supplies high-pressure air to the conveying pipeline. The air and cement particles are mixed in the pipeline, forming a slurry-like flow. As the mixture travels through the pipeline, it passes through various sections, including horizontal and vertical segments, bends, and control valves. The separation and collection unit at the end of the pipeline uses cyclone separators or bag filters to separate the cement particles from the air, allowing the cement to be deposited in the receiving hopper and the air to be discharged or recirculated.
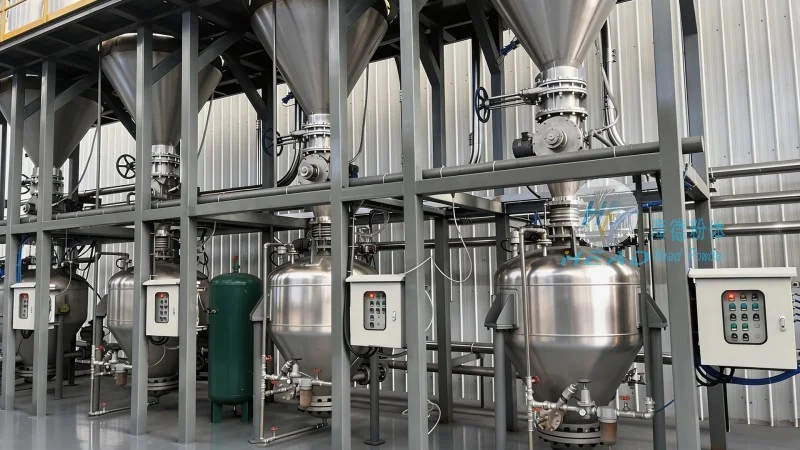
HeadPowder's cement particle pneumatic conveying systems offer several technical advantages that make them ideal for industrial applications. These include high conveying efficiency, minimal material degradation, and reduced dust emissions compared to traditional mechanical conveying methods. The systems are designed to handle large volumes of cement over long distances, making them suitable for applications such as raw material transport in cement plants, finished product distribution, and material transfer between different processing units. The robust construction and advanced control systems ensure reliable operation, even under harsh industrial conditions.
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides comprehensive solutions for cement particle pneumatic conveying systems. By integrating advanced engineering principles and high-quality components, their equipment ensures efficient, safe, and reliable transport of cement and similar fine particulate materials. The structural design and operational mechanisms of these systems are optimized to meet the specific demands of the cement industry, offering significant benefits in terms of productivity, cost-effectiveness, and environmental compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top