HeadPowder, officially known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier based in Shandong, China. The company specializes in the design, development, and production of advanced bulk material handling equipment, with a particular focus on pneumatic conveying systems for industrial applications.
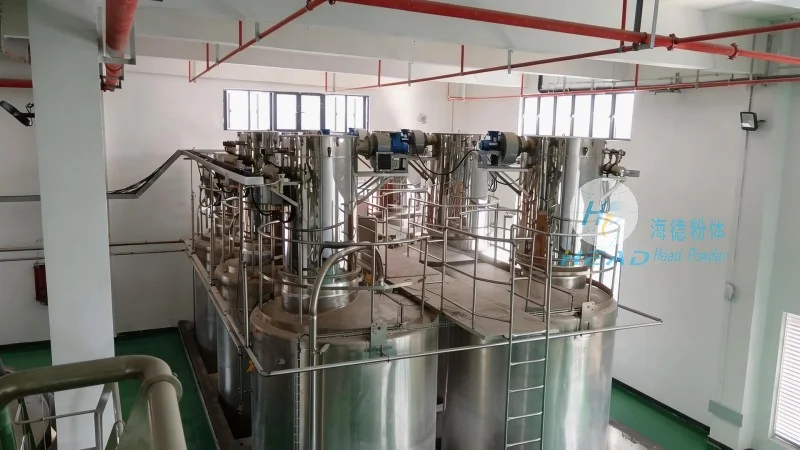
Bulk hopper pneumatic conveying systems are essential components in modern industrial material handling processes. These systems are engineered to efficiently transport bulk materials from storage hoppers or silos to processing units, packaging lines, or other destinations within a facility. The primary function of such systems is to move powders, granules, and other particulate materials in a controlled and reliable manner, minimizing material loss and ensuring consistent flow rates.
The core of a pneumatic conveying system lies in its ability to use air or other gases to transport materials. The system typically consists of several key components, including a hopper or silo for material storage, a conveying line (often equipped with bends and straight sections), a blower or compressor to generate the necessary air pressure, and a control system to regulate the flow. The structural design of these components is critical to the system's performance and efficiency.
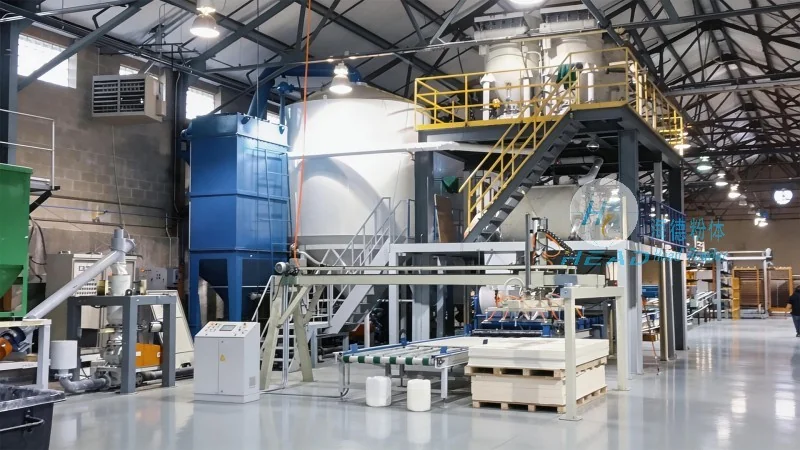
Material hoppers are designed to store bulk materials and provide a consistent feed to the conveying line. They are often equipped with level sensors and discharge valves to control the material flow. The conveying line is constructed from materials that are resistant to abrasion and corrosion, ensuring long-term durability. The blower or compressor generates the air pressure required to move the material through the line. The control system manages the air flow, pressure, and material feed, optimizing the conveying process.
The working principle of a pneumatic conveying system involves the creation of a pressure differential between the inlet and outlet of the conveying line. When the blower or compressor operates, it forces air into the line, creating a high-pressure environment at the inlet. As the material is introduced into the line, it is entrained by the air and carried along the line to the discharge point. The air then releases the material at the destination, where it is collected in a receiving hopper or container. This process is continuous and can be adjusted to handle varying material types and flow rates.
Bulk hopper pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced material handling costs, improved safety by eliminating manual handling, and increased flexibility in material transport. The systems are also capable of handling a wide range of materials, from fine powders to coarse granules, without causing segregation or degradation. Additionally, the enclosed design of the system minimizes dust emissions and environmental impact, making it a preferred choice for industries where dust control is critical.
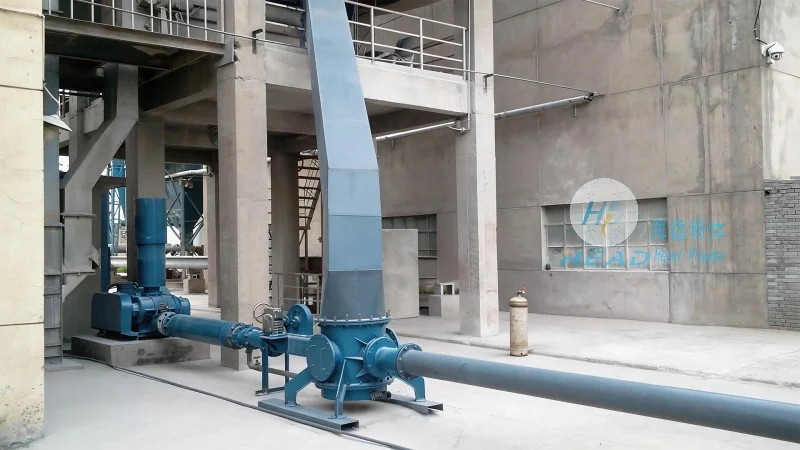
Pneumatic conveying systems are widely used in various industrial sectors, including food and beverage processing, pharmaceutical manufacturing, chemical processing, and mining. In food processing, these systems are used to transport ingredients such as flour, sugar, and spices from storage to production lines. In pharmaceuticals, they are employed to handle powders and granules while maintaining strict hygiene standards. In chemical plants, they are used to transport raw materials and finished products, ensuring safe and efficient material transfer. The versatility of pneumatic conveying systems makes them suitable for a wide array of applications where reliable and efficient material handling is essential.
HeadPowder's bulk hopper pneumatic conveying systems represent a sophisticated solution for modern industrial material handling needs. By combining advanced structural design with efficient pneumatic principles, these systems provide reliable, cost-effective, and environmentally friendly material transport solutions. As a leading manufacturer in the field, HeadPowder continues to innovate and improve its products to meet the evolving demands of industrial applications, ensuring that its customers benefit from the latest technological advancements in bulk material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top