HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design and implementation of pneumatic conveying systems for various industrial applications. This article provides an overview of the principles and structural components involved in the pneumatic conveying of glucose powder, a critical component in the food and pharmaceutical industries.
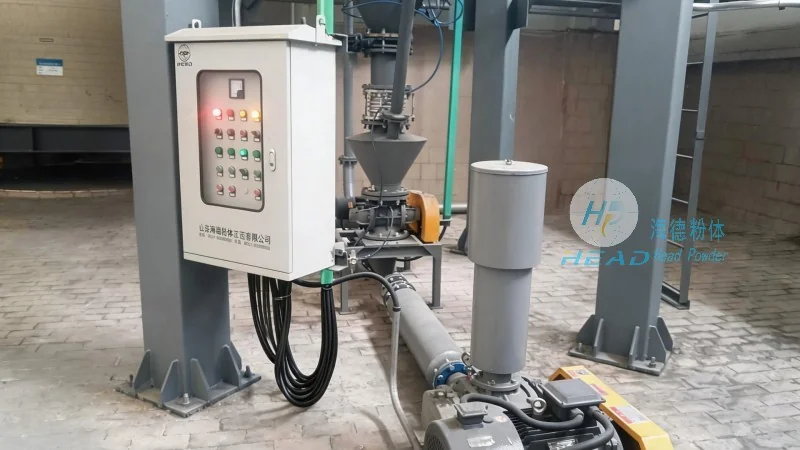
Pneumatic conveying is a widely adopted technique for transporting bulk materials like glucose powder through a pipeline using a stream of air or other gas. This method offers several advantages over traditional mechanical conveying systems, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are sensitive to moisture or contamination. The process involves the creation of a low-pressure or high-pressure air stream within a pipeline, which draws the powder particles into the flow and transports them to the destination point.
A typical pneumatic conveying system for glucose powder consists of several key components that work in tandem to ensure efficient and reliable material transport. These components include the material feed hopper, the air supply system, the conveying pipeline, the control valves, and the discharge equipment. Each component plays a crucial role in the overall operation of the system.
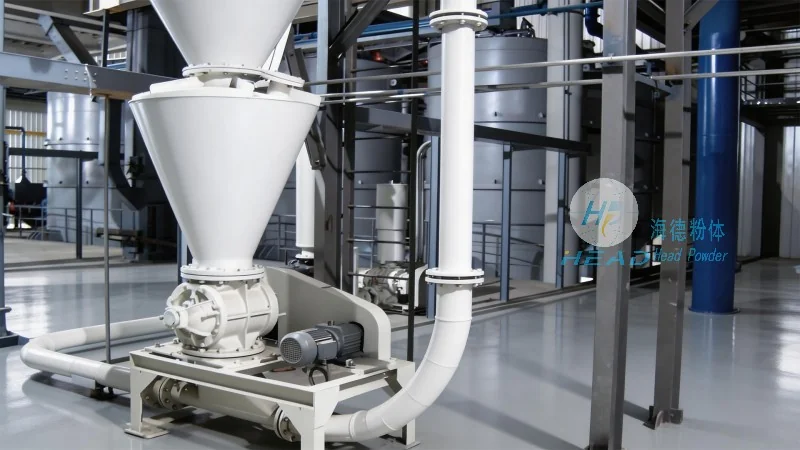
The material feed hopper is the initial component where the glucose powder is stored before being conveyed. It is designed to hold a sufficient quantity of the powder to maintain a continuous flow to the system. The feeder, which can be a rotary valve or a screw feeder, regulates the flow of powder from the hopper into the conveying pipeline. Proper design of the hopper and feeder is essential to prevent material bridging or clogging, which can disrupt the conveying process.
The air supply system is responsible for providing the necessary air or gas to create the conveying stream. This system typically includes a blower or compressor, a filter to remove contaminants from the air, and a pressure regulator to maintain consistent pressure levels. The pressure within the system can be either positive (pressure conveying) or negative (vacuum conveying), depending on the specific requirements of the application. For glucose powder, which is often sensitive to moisture, a positive pressure system is commonly used to prevent moisture absorption from the air.
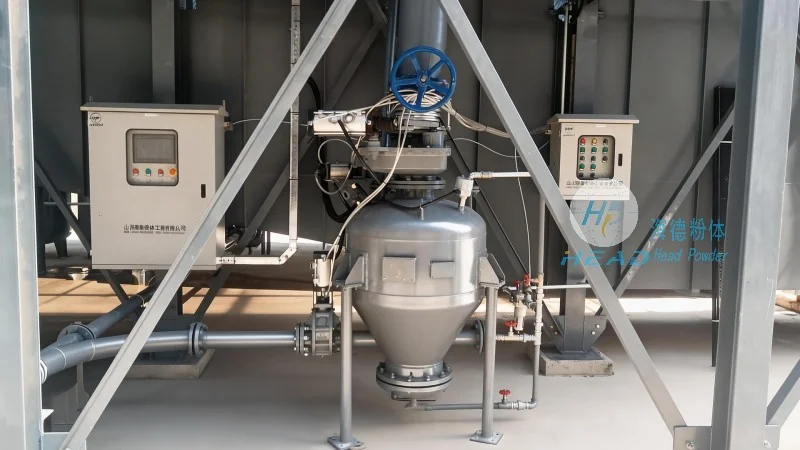
The conveying pipeline is the main channel through which the glucose powder is transported. It is usually made of stainless steel or other corrosion-resistant materials to ensure durability and to prevent contamination of the powder. The pipeline design, including the diameter and length, is critical to maintaining the appropriate air-to-powder ratio and to avoiding excessive pressure drops or particle separation. Flow control devices, such as orifice plates and flow meters, are used to monitor and adjust the air flow rate, ensuring optimal conveying efficiency.
Control valves are used to regulate the flow of air and powder within the system, allowing for precise control over the conveying process. These valves can be automated to respond to changes in material feed or pressure, ensuring consistent operation. The discharge equipment, located at the end of the pipeline, is responsible for releasing the glucose powder into the receiving container or processing unit. This component must be designed to prevent material buildup and to ensure a clean and efficient discharge.
Implementing a pneumatic conveying system for glucose powder offers numerous benefits for industrial operations. These advantages include improved product quality by minimizing exposure to external contaminants, enhanced safety by reducing the need for manual handling of powders, and increased operational efficiency through reduced downtime and maintenance. Additionally, the system can be easily integrated with other processing equipment, allowing for a seamless flow of materials throughout the production line.
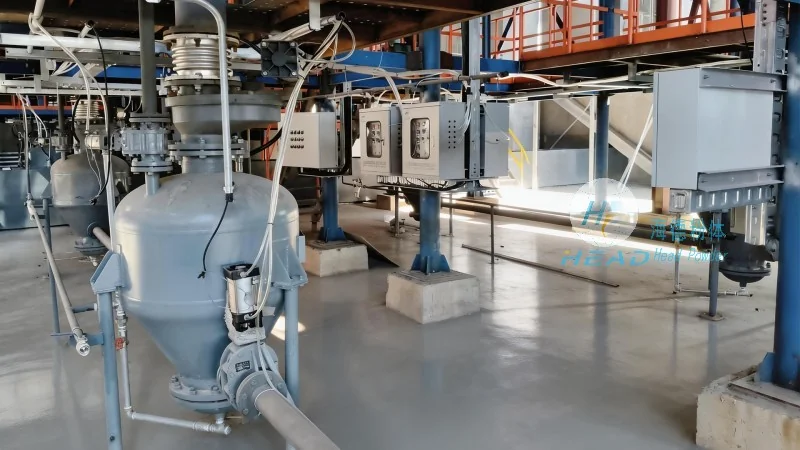
Glucose powder is a vital ingredient in various food products, including beverages, baked goods, and pharmaceutical formulations. The pneumatic conveying systems designed by HeadPowder are specifically tailored to meet the stringent requirements of these industries, including compliance with food safety regulations and the ability to handle materials with high purity standards. These systems are widely used in factories that produce glucose-based products, ensuring that the powder is transported efficiently and without compromising its quality.
In conclusion, the pneumatic conveying of glucose powder is a sophisticated and efficient method for transporting bulk materials in industrial settings. The structural components and operational principles of such systems, as detailed above, are crucial to achieving optimal performance and reliability. With its expertise in powder handling technology, Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for the pneumatic conveying of glucose powder, helping businesses in the food and pharmaceutical sectors to enhance their production processes and maintain high standards of quality and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top