HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic transport systems for industrial applications. This article provides an overview of the air-driven limestone calcination gas transport system, detailing its structural components and operational principles to help professionals in the field understand its functionality and benefits.
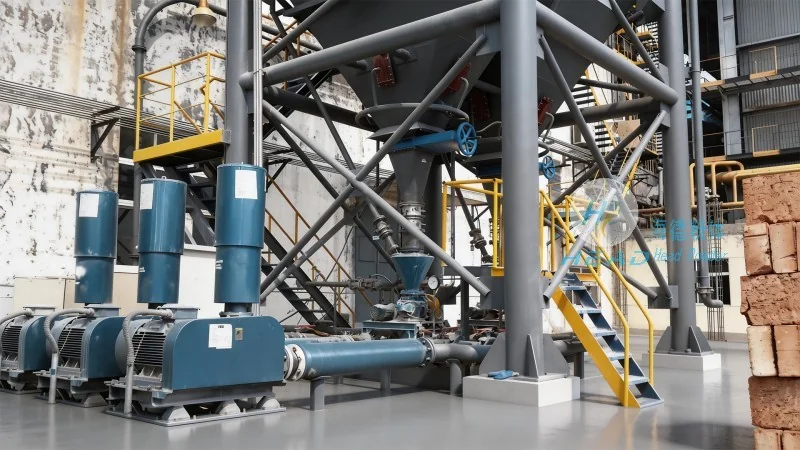
The air-driven limestone calcination pneumatic transport system is a sophisticated piece of industrial equipment engineered to efficiently move calcined limestone from storage or processing areas to the points of use. At its core, the system comprises several key components that work in concert to ensure reliable and efficient material handling. These include a material feeder, a transport pipeline, a control valve system, and a dust collection unit. Each component is strategically designed to handle the specific demands of calcined limestone, a material known for its fine particle size and potential for dust generation during transport.
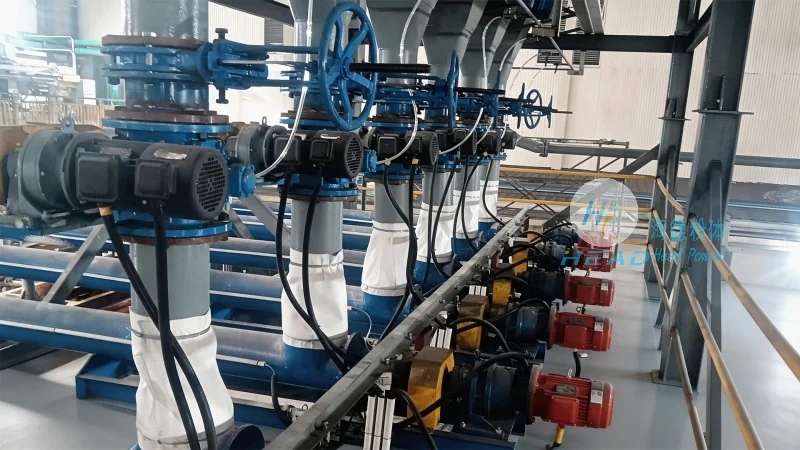
The system operates on the principle of air pressure to move the calcined limestone particles through the pipeline. There are two primary modes of operation: positive pressure and negative pressure (or suction). In the positive pressure system, compressed air is introduced into the pipeline, creating a pressure differential that propels the material forward. The material feeder, typically a rotary valve or a screw feeder, continuously supplies the limestone into the pipeline, while the control valve system regulates the air flow and material feed rate to maintain optimal transport conditions. The negative pressure system, on the other hand, uses a vacuum to draw the material through the pipeline, which is often preferred in applications where the material needs to be transported over longer distances or through complex piping networks.
HeadPowder's air-driven limestone calcination pneumatic transport system offers several technical advantages that make it a preferred choice for industrial operations. One of the key benefits is its high efficiency in material handling, as it eliminates the need for mechanical conveyors and reduces the risk of material degradation or contamination. The system also provides excellent control over the transport process, allowing for precise adjustment of flow rates and pressure levels to match the specific requirements of the application. Additionally, the design minimizes dust emissions and noise, contributing to a safer and more environmentally friendly working environment. These advantages make the system suitable for a wide range of applications, including in cement production, chemical processing, and other industries where calcined limestone is a critical raw material.
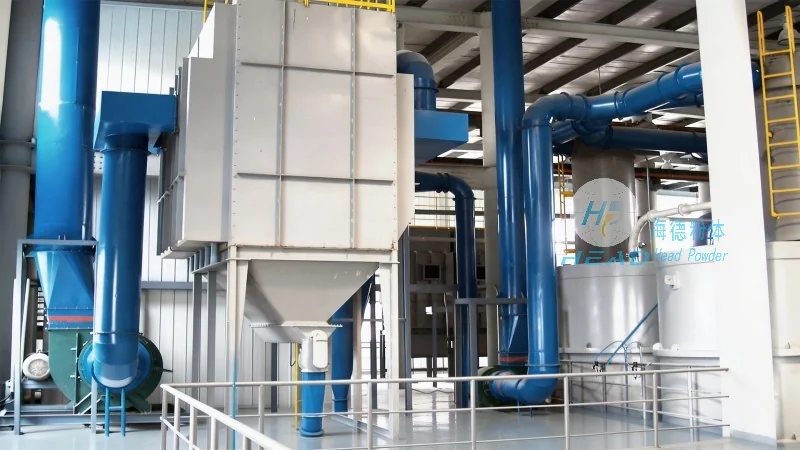
HeadPowder Engineering Co., Ltd. is a professional engineering company headquartered in Shandong, China. With years of experience in the design and manufacturing of industrial pneumatic transport systems, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's commitment to quality, innovation, and customer satisfaction has enabled it to serve a diverse clientele across various industries, providing tailored solutions that meet their unique operational needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top