HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for handling sodium bicarbonate and other bulk materials. This article provides a detailed overview of the operation process and working principle of such equipment, highlighting key components, operational steps, and the technical advantages that ensure efficient material transport in industrial settings.
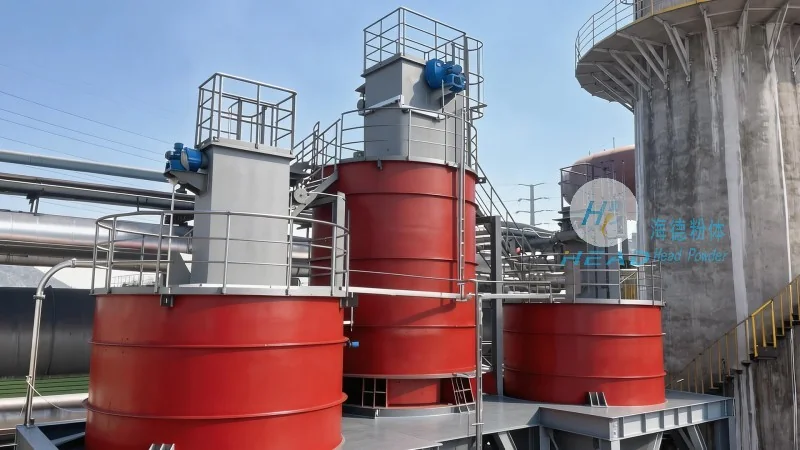
Pneumatic conveying equipment is a critical component in modern industrial processes, enabling the safe and efficient transportation of bulk materials like sodium bicarbonate from storage to processing units. Unlike traditional mechanical conveyors, these systems utilize air or gas as the medium to move materials, offering advantages such as reduced contamination, lower maintenance requirements, and the ability to handle materials with varying properties. HeadPowder's expertise in this field ensures that their systems are optimized for the unique characteristics of sodium bicarbonate, including its fine particle size and potential for dust generation.
The pneumatic conveying system for sodium bicarbonate typically consists of several essential components that work in concert to achieve reliable material transport. These include a hopper or storage silo for material storage, a feeder to control the flow rate, a conveying line (often equipped with bends and filters), a receiver or discharge hopper, and a blower or air compressor to generate the necessary air pressure. Each component plays a vital role in maintaining the system's efficiency and preventing material degradation or blockages.
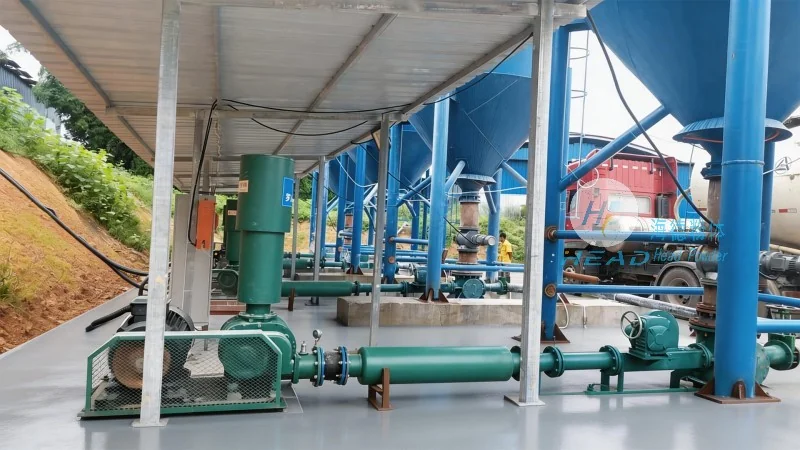
The operation process of the sodium bicarbonate pneumatic conveying system begins with material loading into the storage hopper. The feeder then regulates the flow of material into the conveying line, ensuring a consistent feed rate. Simultaneously, the blower generates high-pressure air that is introduced into the conveying line, creating a flow that propels the sodium bicarbonate particles forward. As the material travels through the system, it passes through various sections, including bends and filters, which help maintain the material's quality and prevent system blockages. The material is then discharged into the receiver hopper at the destination point, completing the transport cycle.
The core working principle of the pneumatic conveying system relies on the principle of fluidization and drag flow. In the conveying line, the high-pressure air creates a flow that lifts and transports the sodium bicarbonate particles. The air velocity is maintained at a level sufficient to overcome the gravitational force acting on the particles, ensuring continuous movement. The system operates under either positive pressure (where air is forced into the conveying line) or negative pressure (where air is drawn out), depending on the specific design and application requirements. HeadPowder's systems are engineered to optimize air pressure and flow rates, minimizing energy consumption while maximizing material throughput.
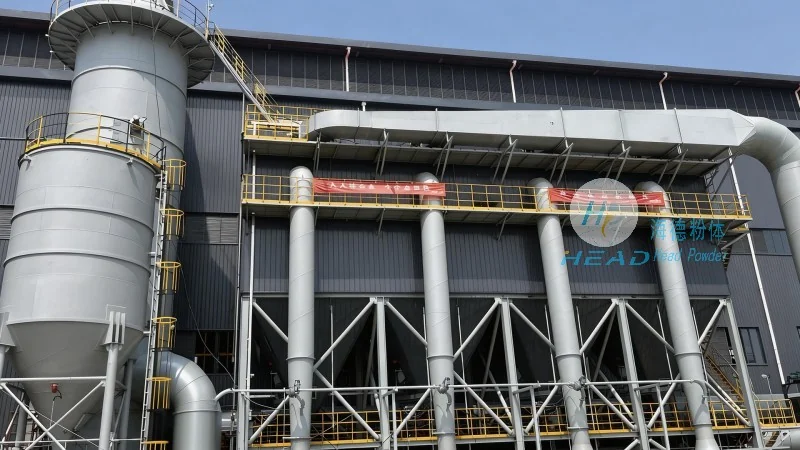
Implementing a pneumatic conveying system for sodium bicarbonate offers several significant advantages over traditional methods. First, it provides a dust-free and hygienic environment, which is crucial for maintaining product quality and compliance with industry standards. Second, the system reduces the risk of material contamination, as it eliminates direct human contact and mechanical wear. Third, it offers flexibility in terms of layout, allowing for horizontal, vertical, or inclined transport paths without the need for complex mechanical components. Additionally, the system is compact and requires less floor space compared to traditional conveyors, making it suitable for facilities with limited space. HeadPowder's systems are designed to maximize these benefits, ensuring long-term operational efficiency and cost savings for their clients.
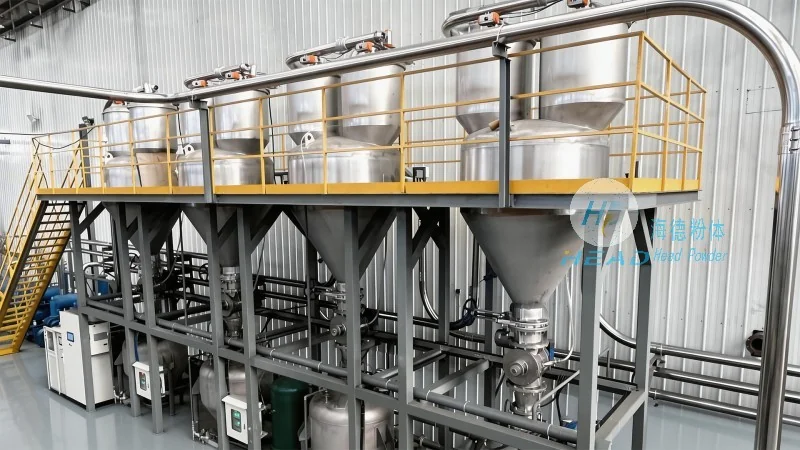
To ensure the reliable and long-term operation of the pneumatic conveying system, regular maintenance and proper operational practices are essential. HeadPowder recommends routine checks of the blower and air compressor to maintain optimal performance, as well as inspections of the conveying line and filters to prevent blockages. The feeder should be adjusted periodically to maintain consistent material flow, and the system should be cleaned regularly to remove any accumulated dust or debris. Proper training of operators on the system's controls and safety procedures is also critical to prevent accidents and ensure smooth operation. By adhering to these maintenance and operational guidelines, users can maximize the system's lifespan and minimize downtime.
HeadPowder's pneumatic conveying equipment for sodium bicarbonate represents a sophisticated solution for efficient and reliable material transport in industrial applications. By understanding the operation process and working principle of these systems, users can appreciate the technical advancements that enable seamless material handling. With their expertise in engineering and manufacturing, HeadPowder continues to provide high-quality systems that meet the evolving needs of the industry, ensuring that sodium bicarbonate and other bulk materials are transported safely and efficiently. The combination of advanced design, robust components, and professional maintenance support makes these systems a valuable investment for any facility requiring reliable bulk material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top