HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced cement powder pneumatic conveying systems. These systems are crucial for efficient and reliable transportation of cement and other fine powders in industrial settings. This article provides a detailed overview of the operation process and working principles of such systems, highlighting their importance in modern material handling.
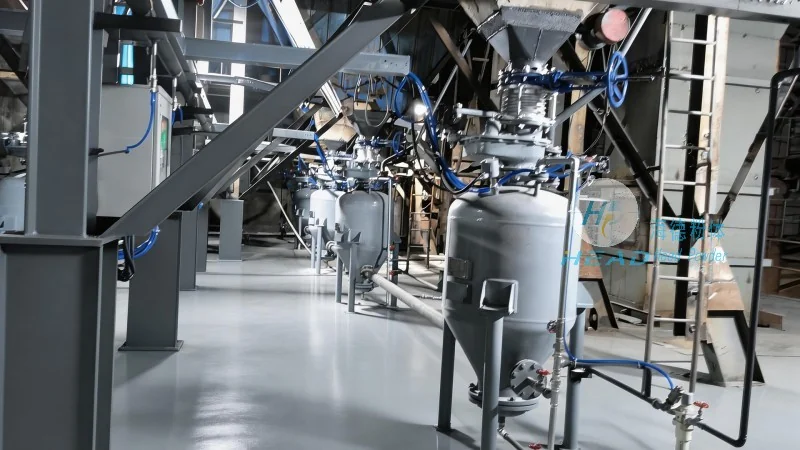
Pneumatic conveying systems utilize air or gas to transport bulk materials like cement powder through a network of pipes. This method offers several advantages over traditional mechanical conveying, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are difficult to transport by other means. The core components of a typical cement powder pneumatic conveying system include a hopper for material storage, a conveyor line with appropriate pipe diameters, a blower or compressor to generate the necessary air pressure, and a control system to regulate the flow of both material and air.
The fundamental principle behind pneumatic conveying is the creation of a pressure differential that propels the cement powder through the system. In a positive pressure system, the blower forces air into the conveyor line, carrying the powder particles along with it. The air velocity must be sufficient to overcome the gravitational force acting on the powder and to prevent particle separation or settling. Conversely, in a negative pressure (or vacuum) system, a vacuum pump draws air and powder from the material source, pulling the material through the pipeline. Both systems rely on the interaction between air flow and particle size, density, and moisture content to ensure stable and efficient transport.
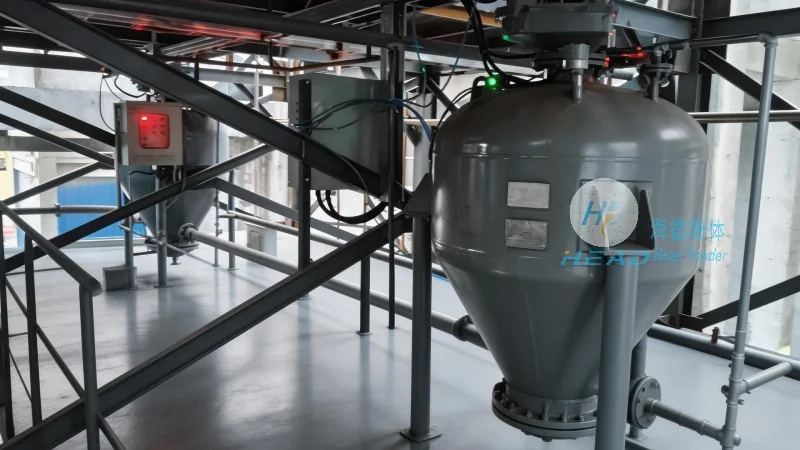
The operation of a cement powder pneumatic conveying system involves several key steps, each designed to ensure optimal performance and material handling efficiency. The process typically begins with the loading of cement powder into the hopper. The hopper is equipped with a feeder, such as a rotary valve or a screw feeder, which controls the flow rate of the material into the conveyor line. As the feeder opens, the cement powder falls into the pipe, where it is entrained by the high-velocity air stream generated by the blower. The air and powder mixture travels through the pipeline to the discharge point, which may be a storage silo, a processing unit, or another destination. At the discharge point, a cyclone separator or a filter is often used to separate the powder from the air, allowing the air to be recirculated or released, and the powder to be collected in the designated container.
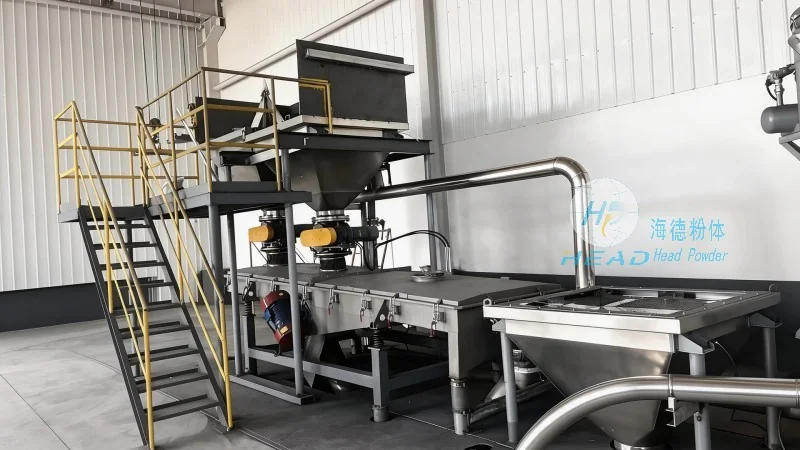
Several critical components work in tandem to ensure the smooth operation of cement powder pneumatic conveying systems. The hopper serves as the primary storage vessel, providing a consistent supply of material to the feeder. The feeder is responsible for controlling the material flow rate, preventing overloading or underloading of the conveyor line. The blower or compressor generates the necessary air pressure and flow rate, with the selection of equipment depending on the system's capacity and the characteristics of the cement powder. The conveyor line, typically made of stainless steel or other corrosion-resistant materials, must be sized appropriately to handle the air and powder mixture without excessive pressure drop or particle degradation. The control system, often integrated with sensors and automation, monitors the system's performance, adjusts the air flow and material feed, and alerts operators to any abnormalities or maintenance needs.
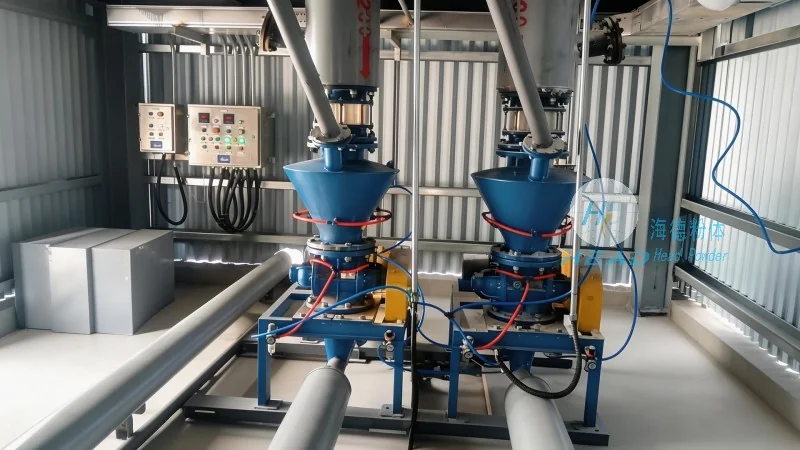
Cement powder pneumatic conveying systems offer numerous benefits in industrial applications, particularly in the cement, construction, and chemical industries. These systems are highly efficient, capable of transporting large volumes of material over long distances with minimal energy consumption. They are also flexible, allowing for changes in the system layout or material handling requirements without major modifications. Additionally, pneumatic conveying systems are suitable for handling materials with varying particle sizes and moisture content, making them versatile for different cement production and processing needs. The systems are widely used in cement plants for transporting raw materials, finished cement products, and additives, as well as in construction sites for delivering cement to mixing equipment.
To ensure the longevity and reliability of cement powder pneumatic conveying systems, regular maintenance and adherence to best practices are essential. Operators should follow a preventive maintenance schedule that includes inspecting and cleaning the hopper, feeder, and conveyor line to prevent material buildup and blockages. The blower and compressor should be checked for proper operation, with filters and lubrication maintained as recommended by the manufacturer. Monitoring the system's pressure and flow rates can help identify potential issues early, such as clogs or air leaks, which can be addressed before they cause system failure. Proper training of personnel on the operation and maintenance of the system is also crucial to ensure safe and efficient performance. By following these best practices, companies can maximize the lifespan of their pneumatic conveying systems and minimize downtime, leading to improved productivity and cost savings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top