Carbon black powder material pneumatic conveying systems represent a sophisticated technology designed to efficiently transport carbon black powder from one location to another through the use of compressed air or other gas streams. The core principle of these systems involves creating a flow of gas that lifts and propels the powder particles through a pipeline network. This method offers significant advantages over traditional mechanical conveying methods, such as reduced equipment wear, lower maintenance costs, and the ability to handle fine powders without the risk of clogging or particle degradation.
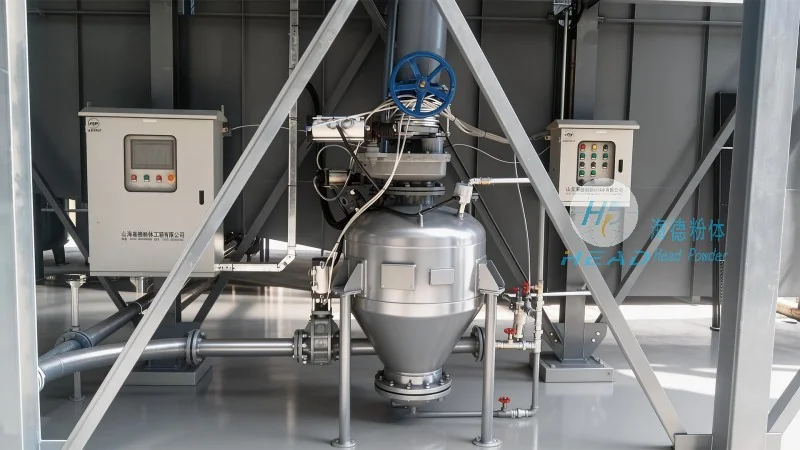
The fundamental operation of a carbon black powder pneumatic conveying system is based on the principle of fluidization and suspension. Compressed air is introduced into a hopper or feeder where the carbon black powder is stored. The air flow generates a pressure differential that lifts the powder particles, creating a dense phase or dilute phase conveying system depending on the system design and operational parameters. In dense phase conveying, the air-to-powder ratio is low, resulting in a slower, more controlled flow that minimizes particle impact and degradation. Dilute phase systems, on the other hand, use a higher air-to-powder ratio, enabling faster transport over longer distances. The choice between these two modes depends on factors such as the powder's properties, the required conveying distance, and the desired product quality.
Carbon black powder pneumatic conveying systems typically consist of several critical components that work in concert to ensure efficient operation. These include a hopper or feeder for storing the powder, a compressor or air source to generate the necessary pressure, a pipeline network for transporting the powder, and a receiver or discharge unit at the destination. The hopper is designed to maintain a consistent powder level and may include a rotary valve or feeder to control the flow rate. The compressor provides the driving force, with options ranging from rotary lobe compressors to centrifugal compressors, depending on the system's capacity and pressure requirements. The pipeline network is constructed from materials resistant to the abrasive nature of carbon black, such as stainless steel or special coatings, to prevent corrosion and wear. The receiver at the end of the system collects the conveyed powder and may include a dust collection system to ensure environmental compliance.
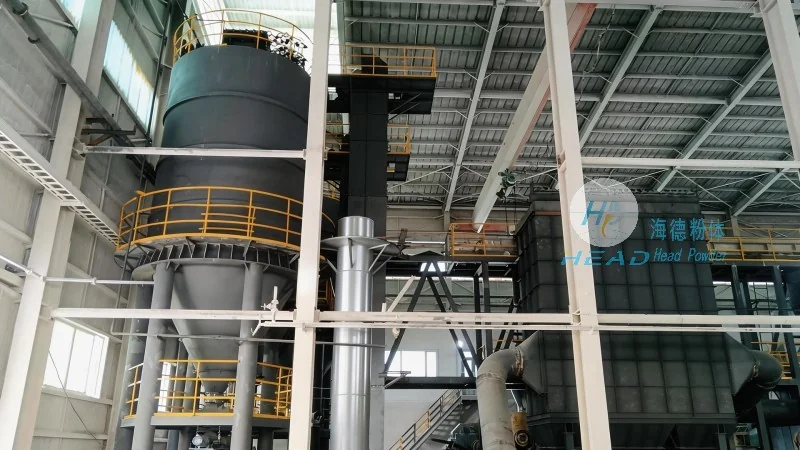
The working scene characteristics of carbon black powder pneumatic conveying systems are tailored to meet the specific needs of various industrial applications. These systems are commonly used in the rubber, plastic, and pigment industries, where carbon black is a key additive. The primary advantages in these applications include the ability to handle fine powders without agglomeration, the reduction of dust exposure for operators, and the flexibility to transport materials over varying distances and elevations. For example, in a rubber manufacturing plant, a pneumatic conveying system can transport carbon black from a storage silo to a mixing machine, ensuring a consistent and controlled feed rate. In the plastic industry, these systems are used to deliver carbon black to extrusion lines, where the material is incorporated into polymer blends. The working scene characteristics also include the ability to integrate with existing production lines, minimizing downtime and operational disruptions. Additionally, the systems are designed to be compact and space-efficient, making them suitable for installations in both new and existing facilities.
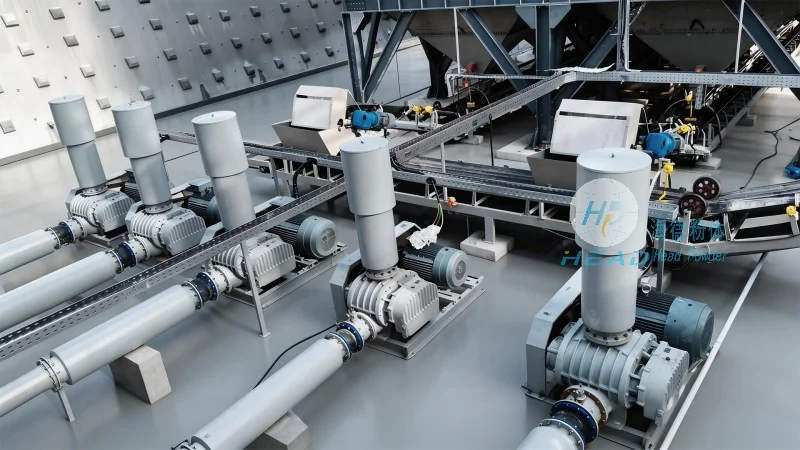
When evaluating carbon black powder pneumatic conveying systems for industrial applications, several key advantages and considerations must be taken into account. The primary benefits include high efficiency in material transport, with the ability to move large volumes of powder over long distances with minimal energy consumption compared to mechanical systems. The systems also offer improved product quality by reducing particle degradation and maintaining consistent particle size distribution. From an operational perspective, pneumatic conveying systems are relatively simple to install and maintain, with fewer moving parts compared to mechanical conveyors. However, there are also considerations such as the need for proper air filtration to prevent dust accumulation in the system and the potential for pressure drops in long pipelines, which may require additional compressor capacity or intermediate booster units. The cost of the system, including the initial investment and ongoing maintenance, is another factor to consider, as it can vary significantly based on the system's capacity and the specific requirements of the application.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of carbon black powder material pneumatic conveying systems. With its headquarters located in Shandong, China, the company specializes in designing, manufacturing, and installing customized conveying solutions tailored to the unique needs of various industries. Headpowder's expertise lies in understanding the specific properties of carbon black powders and translating that knowledge into efficient and reliable conveying systems. The company's products are known for their durability, efficiency, and adherence to industry standards, making them a trusted choice for businesses in the rubber, plastic, and pigment sectors. By leveraging advanced engineering and manufacturing capabilities, headpowder ensures that its pneumatic conveying systems meet the highest quality and performance expectations, providing long-term value to its customers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top