Bicarbonate of soda, also known as sodium bicarbonate, is a widely used chemical in various industries. The efficient and reliable transportation of this material from one location to another is crucial for maintaining production efficiency. Pneumatic conveying systems offer a solution that combines simplicity with effectiveness, making them an ideal choice for handling bicarbonate of soda. This article explores the fundamental principles behind these systems and highlights key application scenarios where they excel.
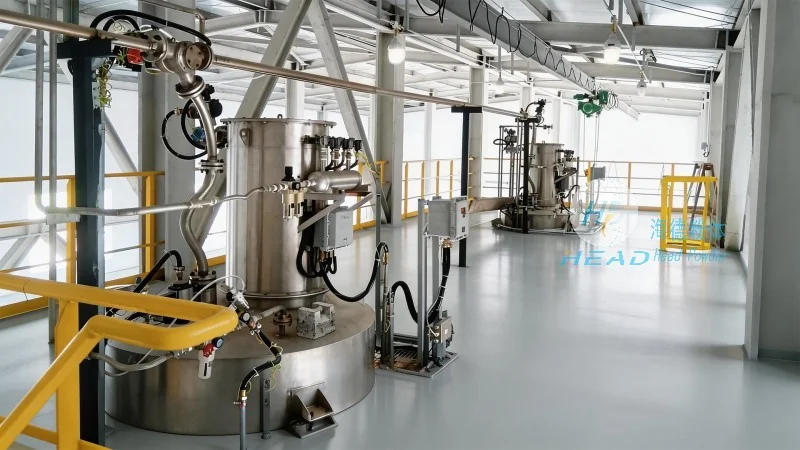
The operation of a pneumatic conveying system for bicarbonate of soda relies on the principle of using air or gas to transport solid particles. The system typically consists of a hopper, a conveyor line, and a receiver. The material is fed into the hopper, and then air is introduced to create a flow that carries the particles through the pipeline. The pressure differential between the hopper and the receiver drives the material forward. This method eliminates the need for mechanical components like belts or screws, reducing maintenance requirements and increasing safety. The system can be either positive pressure (where air is blown into the system) or negative pressure (where air is drawn out), depending on the specific requirements of the application. For bicarbonate of soda, which is a relatively light and non-abrasive material, both types of systems can be effective, but positive pressure is often preferred due to its ability to handle longer distances and more complex layouts.
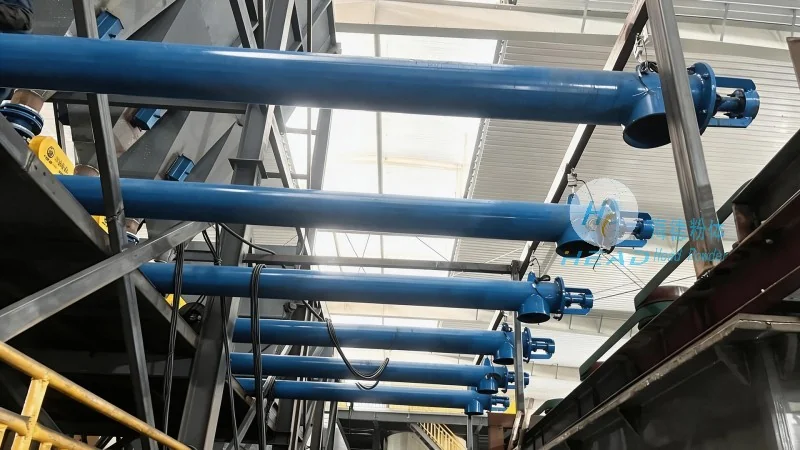
Several critical components make up a pneumatic conveying system for bicarbonate of soda. The hopper serves as the storage and feeding unit, ensuring a consistent supply of material. The conveyor line, which can be made of metal or plastic, transports the material from the hopper to the receiver. The receiver collects the material and may include a filter to remove any air or dust. A rotary valve or feeder controls the flow of material from the hopper into the conveyor line, preventing backflow and maintaining a steady rate. The air compressor or vacuum pump provides the necessary pressure or suction to move the material. For bicarbonate of soda, which is a dry, free-flowing powder, the components are designed to handle low to moderate particle sizes, typically ranging from 10 to 200 microns. The system's design must also consider the material's density and flow characteristics to ensure optimal performance.
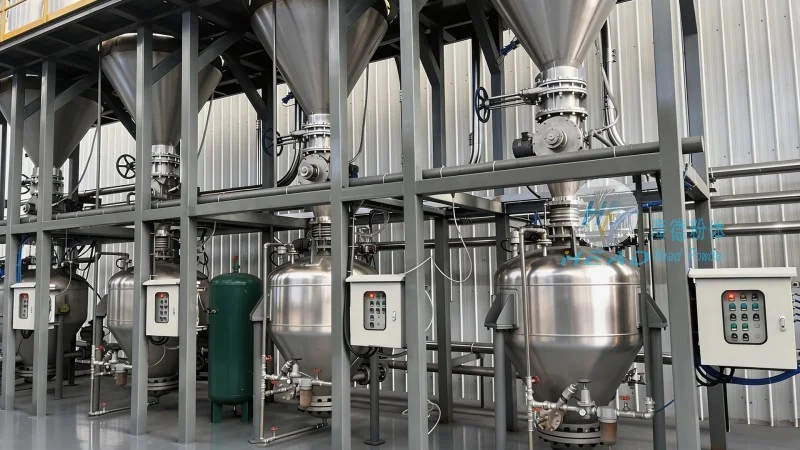
Pneumatic conveying systems for bicarbonate of soda are widely used in various industrial settings. One common application is in food and beverage processing, where the material is used as a leavening agent or pH adjuster. The system allows for the safe and hygienic transfer of the material from storage to production lines, minimizing contamination risks. In pharmaceutical manufacturing, bicarbonate of soda is used as an excipient or buffering agent, and the pneumatic system ensures precise dosing and handling. Another key application is in chemical processing, where the material is used in reactions or as a neutralizer. The system's ability to handle large volumes efficiently makes it suitable for bulk handling operations. Operational advantages of these systems include reduced labor costs due to automated material transfer, improved safety by eliminating manual handling of powders, and increased production speed through continuous operation. The systems are also flexible, allowing for easy integration into existing production lines and modifications to accommodate changes in production volume or material type.
When designing a pneumatic conveying system for bicarbonate of soda, several factors must be considered to ensure optimal performance and longevity. The system's capacity must match the production requirements, taking into account the material's flow rate and the desired transfer speed. The pipeline diameter and length are critical, as they affect the pressure drop and the system's efficiency. The choice between positive and negative pressure depends on the distance to be covered and the presence of obstacles or changes in elevation. For longer distances or complex layouts, positive pressure systems with larger pipelines and more powerful compressors are often required. Maintenance is another important consideration. Regular cleaning of the hopper, conveyor line, and receiver is necessary to prevent clogging and material buildup. The air filter and compressor must be checked and maintained to ensure consistent air quality and pressure. For bicarbonate of soda, which is non-corrosive, the system components can be made of standard materials like stainless steel or plastic, reducing the need for specialized coatings or materials. However, in high-temperature or high-humidity environments, additional measures may be needed to prevent moisture absorption or material degradation.
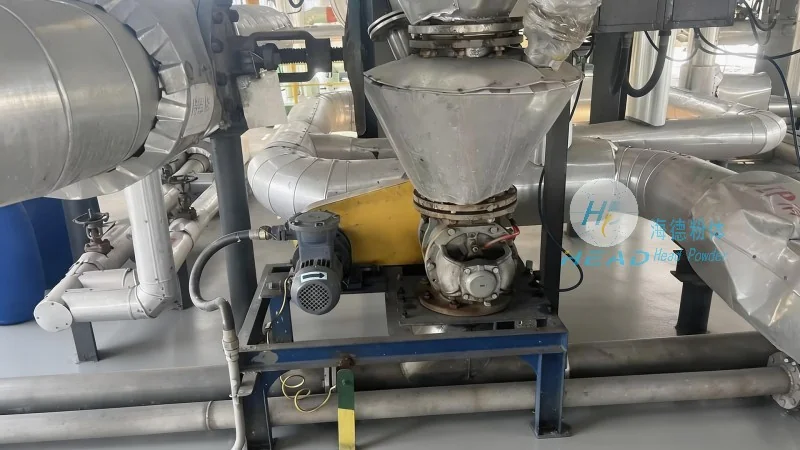
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, has successfully implemented pneumatic conveying systems for bicarbonate of soda in various clients' facilities. One notable project involved a food processing plant that needed to transfer large quantities of bicarbonate of soda from storage to production lines. The system designed by HeadPowder used a positive pressure configuration with a 100mm diameter pipeline and a 20HP air compressor. The hopper had a capacity of 5 tons, and the system was able to achieve a transfer rate of 2 tons per hour, meeting the plant's production demands. The system's design included a rotary valve and a filter to ensure consistent material flow and air quality. The client reported significant improvements in production efficiency and safety, with reduced labor costs and minimal material loss. Another project involved a pharmaceutical manufacturer that required precise dosing of bicarbonate of soda in a batch process. The system designed by HeadPowder used a negative pressure configuration with a 50mm diameter pipeline and a vacuum pump. The hopper had a capacity of 1 ton, and the system was able to achieve a transfer rate of 0.5 tons per hour with high accuracy. The client praised the system's reliability and ease of integration into their existing production line. These case studies demonstrate the effectiveness of pneumatic conveying systems for bicarbonate of soda and the expertise of Shandong HeadPowder Engineering Co., Ltd. in designing and implementing such systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top