Pneumatic conveying has emerged as a critical technology in the pharmaceutical industry for the efficient and hygienic handling of granular materials. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing advanced pneumatic conveying solutions tailored to the unique demands of pharmaceutical production. This article explores the fundamental principles behind pneumatic conveying and highlights key application scenarios where such systems excel in ensuring product integrity and operational efficiency.
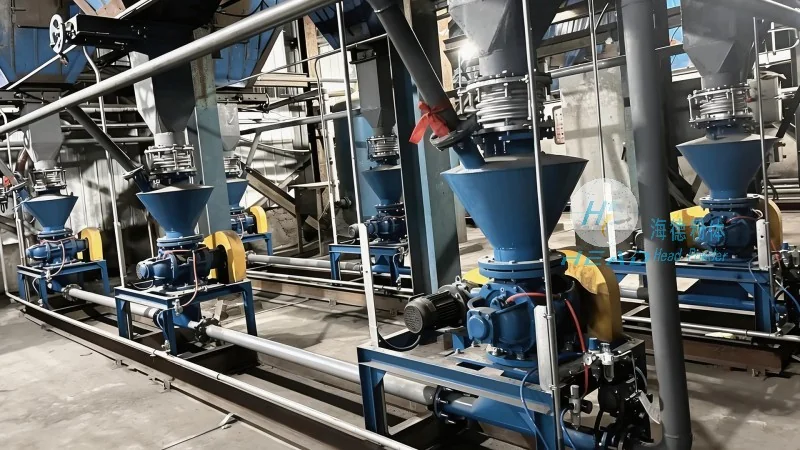
The fundamental principle of pneumatic conveying involves the use of a gas stream, typically air or a controlled inert gas, to transport solid particles through a pipeline. This method relies on the interaction between the gas flow and the particles, creating a drag force that propels the material forward. In pharmaceutical applications, the system must adhere to stringent standards for cleanliness, containment, and product safety. Shandong HeadPowder Engineering Co., Ltd. employs state-of-the-art designs that incorporate features such as positive pressure or negative pressure operation, depending on the specific material characteristics and process requirements. The choice between these modes significantly impacts system performance, including particle velocity, pressure drop, and overall energy consumption.
A pneumatic conveying system for pharmaceutical granular materials typically consists of several critical components, each playing a vital role in ensuring reliable operation. These include the material feed hopper, which ensures a consistent and controlled feed rate; the conveying line, which may be made from stainless steel or other food-grade materials to prevent contamination; and the separation or discharge equipment, such as cyclones or filters, that separates the conveyed material from the air stream. The system design also considers factors like particle size distribution, moisture content, and dust generation, as these variables directly affect the system's efficiency and maintenance needs. Shandong HeadPowder Engineering Co., Ltd. utilizes advanced computational fluid dynamics (CFD) and material testing to optimize component sizing and system layout, ensuring minimal pressure losses and maximum material throughput.
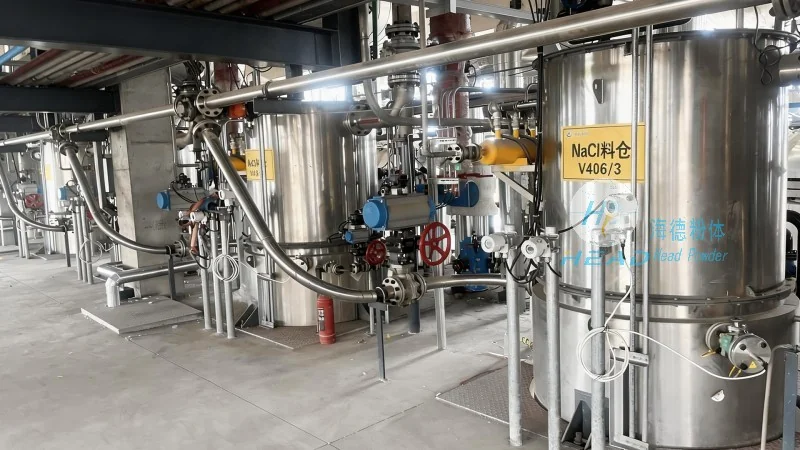
Pneumatic conveying systems are widely utilized across various stages of pharmaceutical manufacturing, from raw material handling to finished product packaging. One primary application is the transport of active pharmaceutical ingredients (APIs) and excipients from bulk storage to processing lines. This process requires precise control to prevent cross-contamination and maintain product purity. Shandong HeadPowder Engineering Co., Ltd.'s systems are engineered to handle sensitive materials with minimal exposure to air, reducing the risk of oxidation or degradation. Another key scenario involves the conveying of finished dosage forms, such as tablets or capsules, from packaging lines to storage or shipping areas. Here, the system must maintain a sterile environment and ensure that the product remains intact during transport. Additionally, pneumatic conveying is employed in the transfer of bulk powders for quality control testing, where accurate sampling and analysis are critical for regulatory compliance.
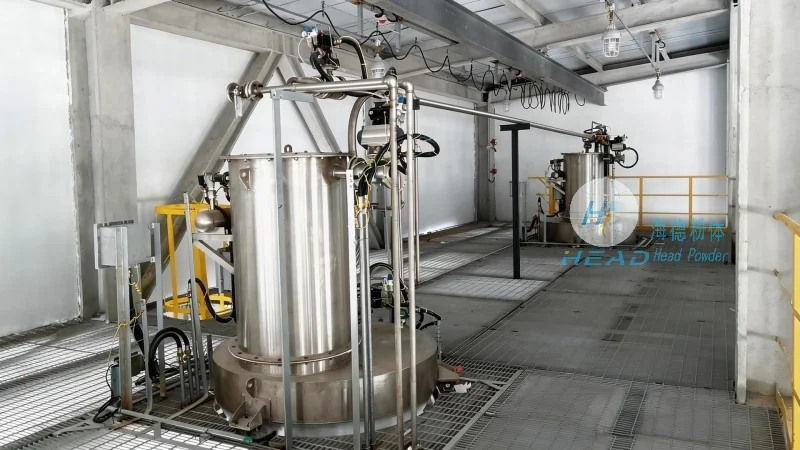
Implementing pneumatic conveying for pharmaceutical granular materials offers several advantages, including improved process control, reduced labor costs, and enhanced safety compared to manual handling. The enclosed system design minimizes dust exposure, which is crucial for maintaining a cleanroom environment. Furthermore, the system allows for flexible material handling, enabling the transfer of materials between different locations within a facility without the need for extensive reconfiguration. However, challenges such as particle agglomeration, system blockages, and the need for regular maintenance remain. Shandong HeadPowder Engineering Co., Ltd. addresses these challenges through robust system design, including features like pulse-jet cleaning for cyclones and automated blockage detection systems. The company also provides comprehensive maintenance and support services to ensure long-term system reliability.
In conclusion, pneumatic conveying systems represent a sophisticated and essential technology for the efficient handling of pharmaceutical granular materials. Shandong HeadPowder Engineering Co., Ltd. leverages its expertise to develop customized solutions that meet the stringent requirements of the pharmaceutical industry, ensuring product quality, safety, and operational efficiency. As the industry continues to evolve, advancements in system design and material handling technology will likely further enhance the capabilities of pneumatic conveying, making it an increasingly vital component of modern pharmaceutical manufacturing processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top