Pneumatic conveying technology plays a crucial role in modern industrial operations, particularly in the management of dust and fine powders. As a professional manufacturer based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. (headpowder) specializes in developing and implementing advanced dust collection and gas-solid conveying solutions. These systems are essential for efficiently transporting bulk materials while maintaining environmental compliance and operational efficiency. This article provides an in-depth analysis of negative and positive pressure pneumatic conveying systems, exploring their principles, applications, and benefits.
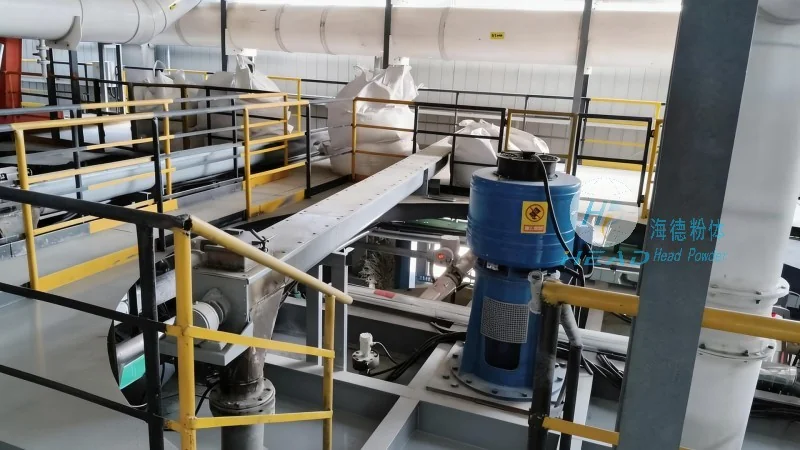
Pneumatic conveying systems are categorized into two primary types based on the pressure differential within the pipeline: negative pressure (vacuum) systems and positive pressure systems. The choice between these systems depends on the specific material characteristics, transport distance, and operational requirements of the application.
Negative pressure systems operate by creating a vacuum in the conveying pipeline. This vacuum draws material from the source (such as a dust collector or hopper) into the pipeline using the pressure difference between the source and the pipeline. The material is then transported to the destination (e.g., a storage silo or processing unit) by maintaining the vacuum. This method is often referred to as "suction" or "vacuum" conveying.
Positive pressure systems, on the other hand, use compressed air to push material through the pipeline. The pipeline is pressurized above atmospheric pressure, and the material is carried by the air stream as it moves from the source to the destination. This approach is commonly known as "pressure" or "blow" conveying.
Negative pressure conveying systems are particularly well-suited for applications that demand gentle material handling and low noise levels. The vacuum environment minimizes the risk of dust leakage and ensures that fine powders are transported without clogging or degradation. This makes negative pressure systems ideal for handling sensitive materials, such as pharmaceutical powders or food products, where contamination and particle damage must be avoided.
One of the primary advantages of negative pressure systems is their energy efficiency. By operating at lower pressures, these systems consume less energy compared to positive pressure systems, leading to reduced operational costs. Additionally, the quiet operation of negative pressure systems is beneficial in environments where noise control is a priority, such as in residential or urban industrial settings.
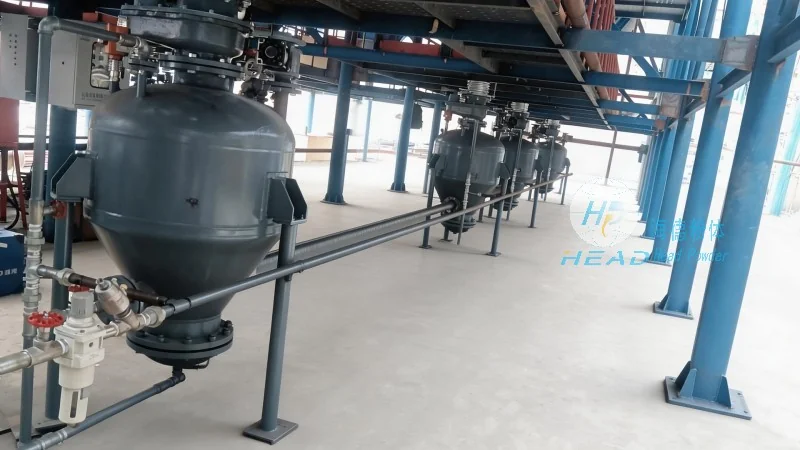
Another key benefit is the ability to handle long-distance transport with minimal pressure drop. Negative pressure systems can effectively convey materials over distances of several hundred meters without significant loss of vacuum, making them suitable for large-scale dust collection and material recovery applications.
In dust collection systems, negative pressure conveying is widely used to transport collected dust from filtration units back to storage silos or processing facilities. This process, known as "material recovery," ensures that valuable raw materials are not lost to the environment and are instead recycled back into the production cycle. For example, in cement plants, negative pressure systems are used to convey fly ash or cement clinker from baghouse filters to storage silos, improving material utilization and reducing waste.
The gentle handling of materials in negative pressure systems also reduces the risk of agglomeration or degradation, which can occur with high-pressure positive systems. This is particularly important for materials that are prone to clumping, such as powders with high moisture content or those that are sensitive to mechanical stress.
Positive pressure pneumatic conveying systems are designed for high-volume, high-speed material transport over longer distances. These systems use compressed air to create a pressure differential that propels material through the pipeline. The primary advantage of positive pressure systems is their ability to handle a wide range of materials, including abrasive, high-density, or sticky powders, without the risk of clogging.
One of the main benefits of positive pressure systems is their flexibility in material handling. The pressurized pipeline allows for multiple delivery points, enabling the distribution of material to several destinations from a single source. This is particularly useful in large-scale industrial operations where materials need to be transported to multiple processing units or storage locations.
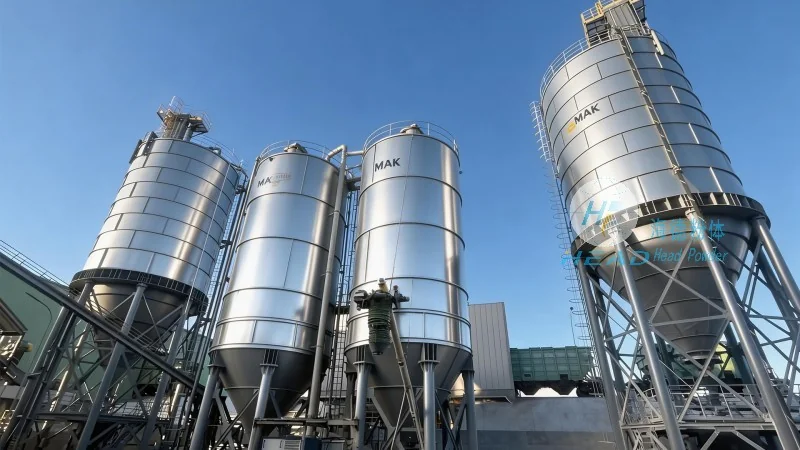
Positive pressure systems also offer better control over material flow rates and pressure. By adjusting the air pressure and flow rate, operators can precisely control the speed and volume of material transport, ensuring consistent performance and preventing overloading of downstream equipment.
Positive pressure systems are commonly used in industries such as chemical manufacturing, food processing, and pharmaceuticals for transporting raw materials to production lines. For instance, in chemical plants, positive pressure systems are used to convey powders like calcium carbonate or silica to reactors, where they are used as raw materials in the production of coatings or plastics.
In food processing, positive pressure systems are employed to transport ingredients like flour, sugar, or spices to mixing and packaging units. The gentle and efficient transport of these materials ensures that product quality is maintained, and the risk of contamination is minimized.
Another application is in the transportation of abrasive materials, such as sand or metal powders, which require high-pressure air to prevent clogging and ensure reliable operation. Positive pressure systems are also suitable for long-distance transport, as they can maintain sufficient pressure to move materials over distances of several kilometers without significant pressure loss.
When selecting between negative and positive pressure pneumatic conveying systems, several factors must be considered. The choice depends on the material properties, transport distance, required throughput, and operational environment. Negative pressure systems are generally preferred for applications that require low noise, gentle handling, and energy efficiency, especially for fine or sensitive powders. Positive pressure systems are more suitable for high-volume, long-distance transport of abrasive or high-density materials, where flexibility and control are critical.
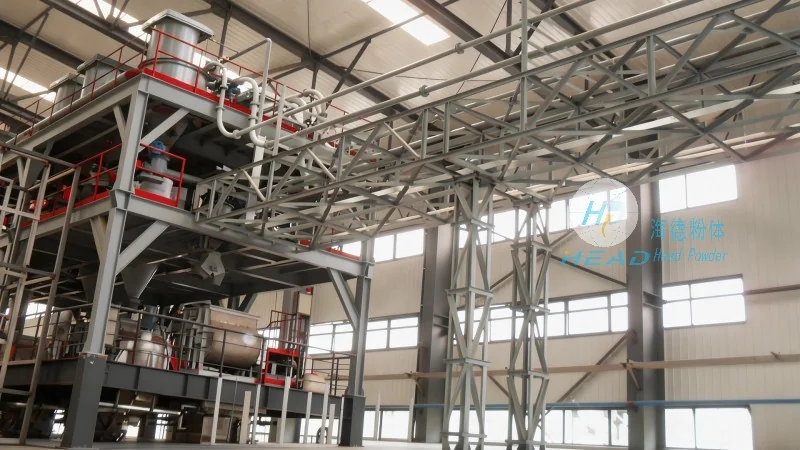
Both systems have their unique advantages and limitations. Negative pressure systems are more energy-efficient and quieter but may have limitations in handling high-volume or abrasive materials. Positive pressure systems offer greater flexibility and can handle a wider range of materials but may require higher energy input and more robust equipment to prevent clogging.
Successful implementation of pneumatic conveying systems requires careful consideration of design, material selection, and maintenance. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions that include system design, installation, and after-sales support to ensure optimal performance and longevity.
Regular maintenance is essential to prevent blockages and ensure consistent operation. This includes inspecting pipelines for leaks or damage, cleaning filters and cyclones, and maintaining air compressors and vacuum pumps. Proper maintenance not only extends the lifespan of the equipment but also reduces downtime and operational costs.
The company's expertise in dust collection and pneumatic conveying allows them to tailor solutions to specific client needs, ensuring that the chosen system meets the operational requirements and delivers long-term benefits.
Pneumatic conveying technology, whether negative or positive pressure, is a critical component of modern industrial operations. The ability to efficiently transport dust and powders while maintaining environmental compliance and operational efficiency has made these systems indispensable in various industries. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide advanced solutions that address the evolving needs of industrial material handling, contributing to improved productivity and sustainability in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top