High-alumina fly ash, a byproduct of coal combustion, is widely used in construction and industrial applications due to its beneficial properties. Efficient handling and transportation of this fine powder are crucial for optimizing production processes. Pneumatic conveying systems offer a reliable solution for transporting high-alumina fly ash, ensuring minimal dust generation and operational efficiency. This article explores the principles behind high-alumina fly ash pneumatic conveying lines and highlights the key working scene characteristics that make them suitable for various industrial applications.
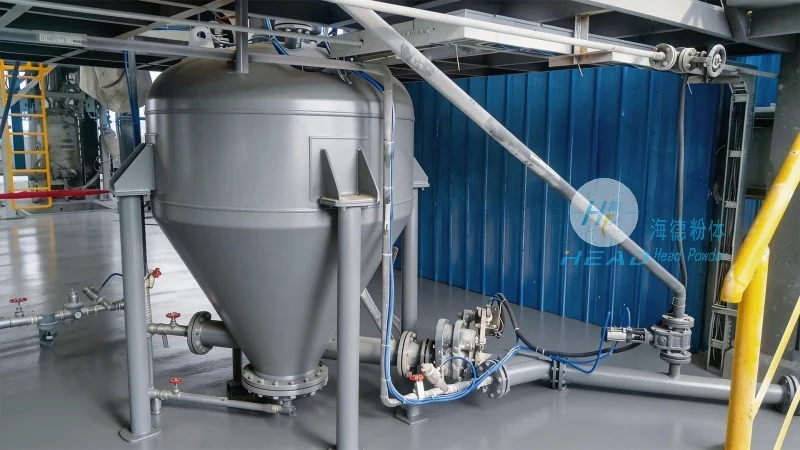
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in engineering solutions for powder handling and material transportation. With a strong focus on innovation and quality, HeadPowder provides customized pneumatic conveying systems tailored to the specific needs of clients in the construction, power generation, and industrial sectors. The company’s headquarters is located in Shandong, China, where it leverages advanced technology and expertise to deliver efficient and reliable solutions for high-alumina fly ash handling.
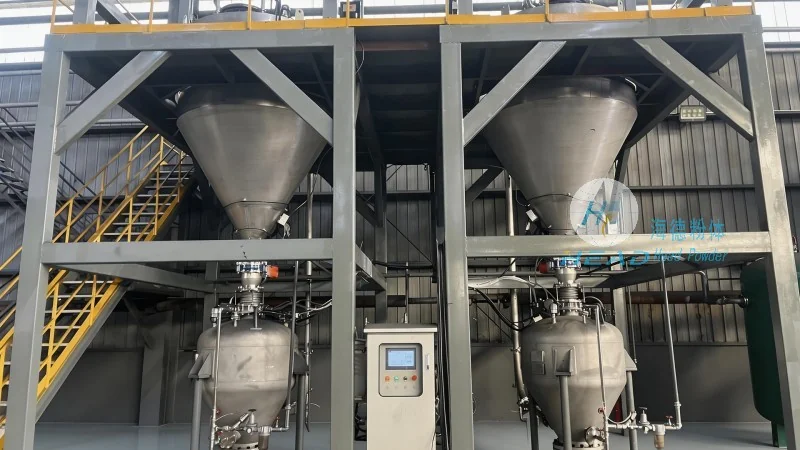
Pneumatic conveying systems operate by using air or gas to transport bulk materials through a pipeline. For high-alumina fly ash, which is a fine powder with a high density and potential for dust formation, the system design must address several key factors to ensure optimal performance. The primary principle involves creating a pressure differential between the inlet and outlet of the conveying line. This is achieved by either using a positive pressure system (where air is blown into the line) or a negative pressure system (where air is drawn out). The choice of system depends on the distance, material characteristics, and operational requirements. High-alumina fly ash, with its abrasive nature and potential for caking, requires specialized equipment such as rotary valves, filters, and cyclones to maintain consistent flow and prevent blockages. The conveying line typically includes components like feeders, pipelines, and receivers, all designed to handle the specific properties of the fly ash. The air velocity in the pipeline is carefully controlled to ensure that the material is transported without excessive wear or degradation. By understanding the physical properties of high-alumina fly ash—such as particle size distribution, moisture content, and density—the system can be optimized to achieve efficient and reliable transportation. The principle also involves maintaining proper air-to-material ratios to prevent segregation and ensure uniform flow throughout the conveying process.
The working scene characteristics of high-alumina fly ash pneumatic conveying lines are tailored to the specific demands of industrial environments. These systems are designed to operate in settings where dust control and material integrity are paramount. One key characteristic is the ability to handle large volumes of fly ash over long distances, often from storage silos to processing facilities or from power plants to construction sites. The systems are typically installed in enclosed environments to minimize environmental impact and comply with regulatory standards. The working scene also includes considerations for maintenance and operational flexibility. Regular maintenance, such as cleaning filters and checking for wear in components, is essential to ensure the system’s longevity and performance. The flexibility of the system allows for adjustments in flow rates and pressure to accommodate varying production demands. Another important characteristic is the integration with other industrial equipment, such as mixers, grinders, or storage tanks. This integration ensures a seamless workflow, from material extraction to final use. The working scene may also involve multiple conveying lines operating simultaneously, allowing for the distribution of fly ash to different locations within a facility. The systems are designed to be robust and durable, capable of withstanding the harsh conditions associated with high-alumina fly ash, including its abrasive nature and potential for moisture absorption. Overall, the working scene characteristics highlight the adaptability and efficiency of high-alumina fly ash pneumatic conveying lines in meeting the diverse needs of industrial applications.
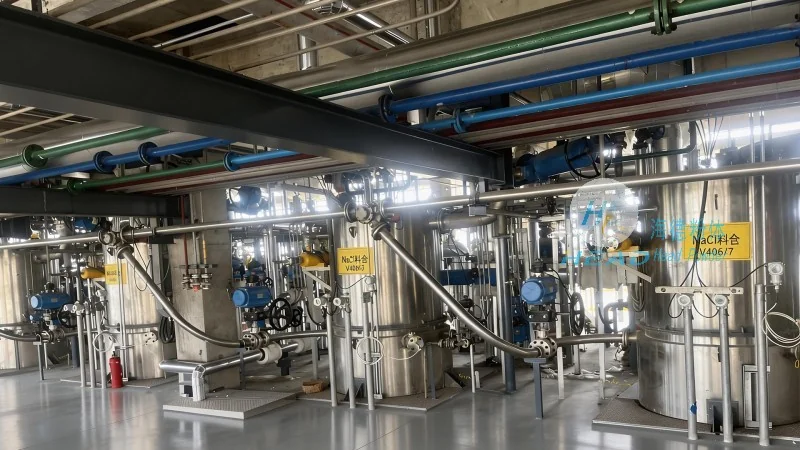
High-alumina fly ash pneumatic conveying lines offer several benefits that make them a preferred choice for industrial applications. The primary benefit is the reduction of dust exposure, which enhances workplace safety and compliance with environmental regulations. By transporting the material in a closed system, the risk of airborne dust is minimized, protecting both personnel and the environment. Another significant benefit is the improvement in operational efficiency. Pneumatic conveying systems can transport high-alumina fly ash at high speeds, reducing the time and labor required for material handling. This leads to increased productivity and cost savings for the end-user. The systems also contribute to better material quality by preventing segregation and maintaining consistent particle size distribution. This is particularly important for applications where the fly ash is used in concrete production or as a raw material in other industrial processes. The adaptability of the system allows it to be used in various settings, from small-scale construction projects to large-scale power plant operations. The key applications include transporting fly ash from storage silos to concrete mixing plants, from power generation facilities to recycling centers, and from industrial sites to construction sites for road or building construction. The systems are also suitable for handling other fine powders with similar properties, making them versatile solutions for material transportation needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top