Denitrizer powder pneumatic conveying systems are critical components in industrial processes that require the efficient transport of powdered denitrizing agents. These systems utilize air or other gas streams to move the powder from one location to another, ensuring safe and reliable operation in various industrial applications. The following sections detail the operation process and working principle of such systems, highlighting key components and their functions. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these systems, providing customized solutions for industrial clients.
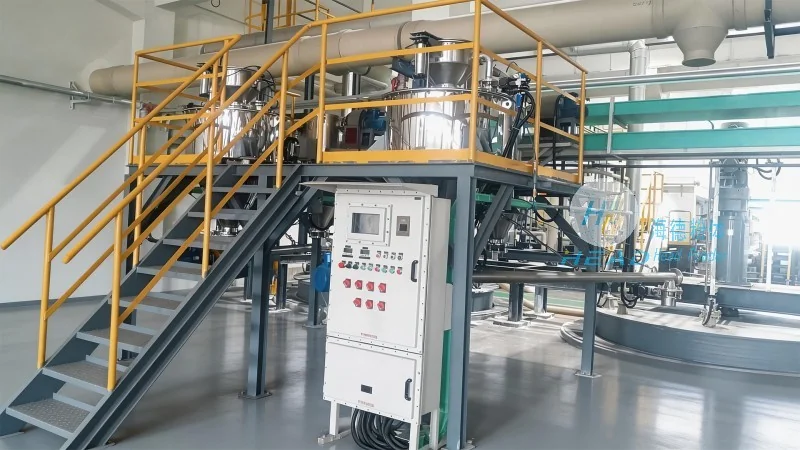
Denitrizer powder pneumatic conveying systems are designed to handle the transportation of denitrizing agents, which are essential in reducing nitrogen oxides (NOx) emissions from industrial sources. The systems are engineered to maintain the integrity of the powder, prevent caking or agglomeration, and ensure consistent flow rates. The primary goal is to provide a reliable method for moving these powders over distances, often in challenging environments where traditional mechanical conveyors may not be suitable.
The denitrizer powder pneumatic conveying system typically consists of several key components, each playing a crucial role in the overall operation. These components include the hopper or storage silo, the conveying line (often with a pipeline), the air or gas source (such as a blower or compressor), and the control system. Each component works in tandem to ensure efficient and safe powder transport.
The working principle of a denitrizer powder pneumatic conveying system is based on the use of air or gas to create a flow that carries the powder particles. The process can be categorized into two main types: dilute phase and dense phase conveying. Dilute phase systems use lower air velocities and higher air-to-powder ratios, while dense phase systems use higher air velocities and lower ratios, resulting in a more controlled and gentle transport.
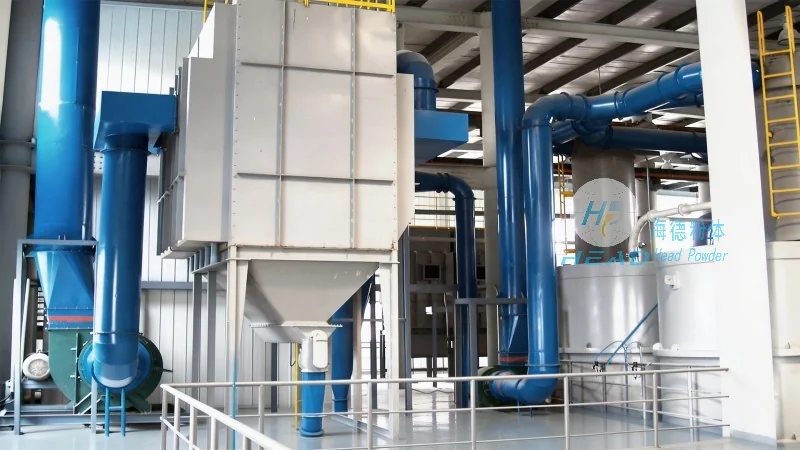
In the operation, the powder is drawn from the hopper into the conveying line by the air stream. The air and powder mixture travels through the pipeline, with the air providing the necessary momentum to move the particles. At the destination, the powder is separated from the air, often through a cyclone separator or a filter, and collected in a receiving hopper or silo. The air is then filtered and discharged back into the environment, ensuring compliance with environmental regulations.
The operation process of a denitrizer powder pneumatic conveying system involves several steps to ensure smooth and efficient transport. The process begins with the loading of the denitrizer powder into the storage hopper. The control system then activates the air source, which starts the flow of air through the conveying line. As the air flows, it draws the powder from the hopper and transports it to the destination. The system continuously monitors the flow rate and pressure, adjusting the air supply as needed to maintain optimal performance. When the destination is reached, the powder is discharged and collected, and the air is filtered and recycled. The entire process is automated, with the control system ensuring that the system operates within safe and efficient parameters.
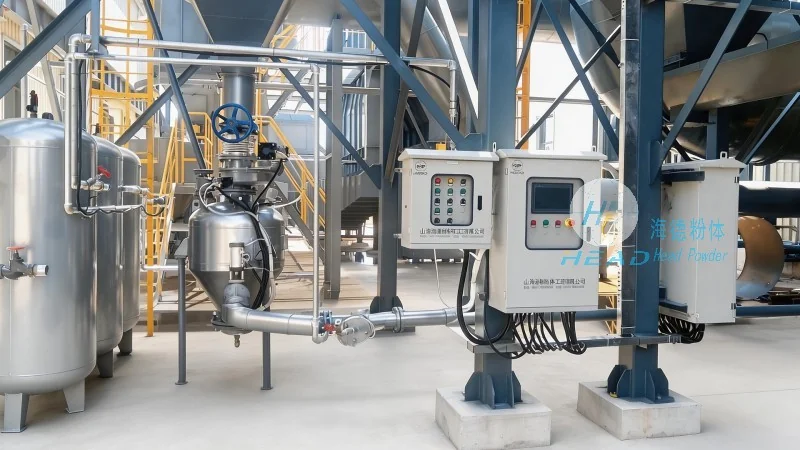
Denitrizer powder pneumatic conveying systems offer several advantages over traditional mechanical conveyors. These include the ability to handle fine powders without caking or agglomeration, reduced risk of dust contamination, and the ability to transport powders over long distances without the need for multiple transfer points. Additionally, the systems are compact and can be installed in tight spaces, making them suitable for various industrial settings. The use of air as the conveying medium also allows for gentle handling of the powder, preserving its quality and preventing degradation.
Denitrizer powder pneumatic conveying systems are widely used in industries that require the transport of denitrizing agents, including power generation, chemical manufacturing, and industrial boiler operations. These systems are essential in applications where NOx reduction is critical, such as in coal-fired power plants and industrial facilities that use combustion processes. The systems are designed to meet the specific requirements of each application, ensuring efficient and reliable operation.
Maintenance of denitrizer powder pneumatic conveying systems is crucial to ensure long-term performance and safety. Regular inspection of components such as the hopper, conveying line, and air source is necessary to prevent issues such as clogging or corrosion. The control system should be checked regularly to ensure it is functioning correctly and providing accurate monitoring of the process. Safety considerations include proper ventilation to remove dust and fumes, and the use of explosion-proof equipment in areas where there is a risk of dust accumulation. Proper training of operators is also essential to ensure safe and efficient operation of the system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top