HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. Among their core offerings is the negative pressure dilute phase powder pneumatic conveying line, a technology that efficiently transports fine powders and granular materials over long distances with minimal energy consumption and high reliability. This article delves into the fundamental principles behind this system, its operational characteristics, and the diverse industrial applications where it excels.
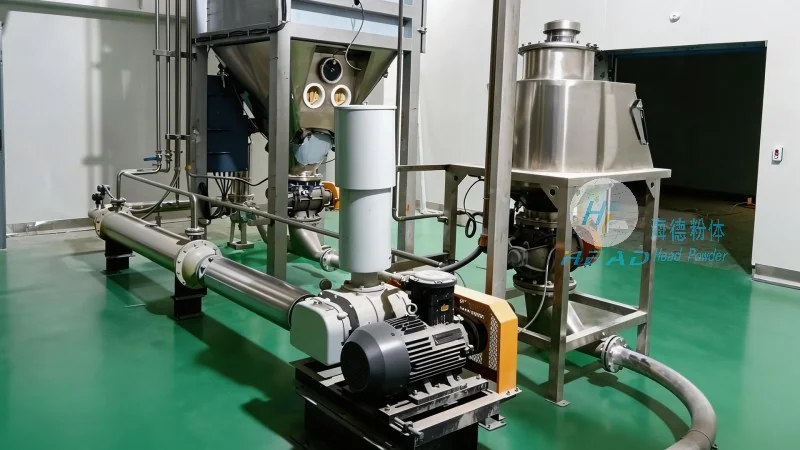
The negative pressure dilute phase powder pneumatic conveying system operates on the principle of creating a vacuum or negative pressure in the conveying line to draw material from the source and transport it to the destination. Unlike positive pressure systems that force air through the material, this method uses suction to move the material, which is particularly effective for handling fine powders that are prone to dust and caking. The system typically consists of a vacuum pump, a material feed hopper, a conveying line, and a discharge receiver. The vacuum pump generates the necessary suction force, while the feed hopper ensures a consistent flow of material into the line. The conveying line, often made of stainless steel or other corrosion-resistant materials, maintains the negative pressure throughout the system, preventing material leakage and ensuring a clean transfer process.
One of the primary advantages of the negative pressure dilute phase system is its ability to handle fine powders with high efficiency and minimal degradation. The dilute phase operation ensures that the material is suspended in the air stream at a low concentration, reducing the risk of blockages and ensuring smooth flow. This method is particularly suitable for materials that are sensitive to moisture or temperature changes, as the system maintains a stable environment during transport. Additionally, the negative pressure design minimizes dust emissions compared to positive pressure systems, making it more environmentally friendly and safer for operators. The system also offers flexibility in terms of layout, as it can be configured to follow complex routes and accommodate multiple transfer points without significant modifications.
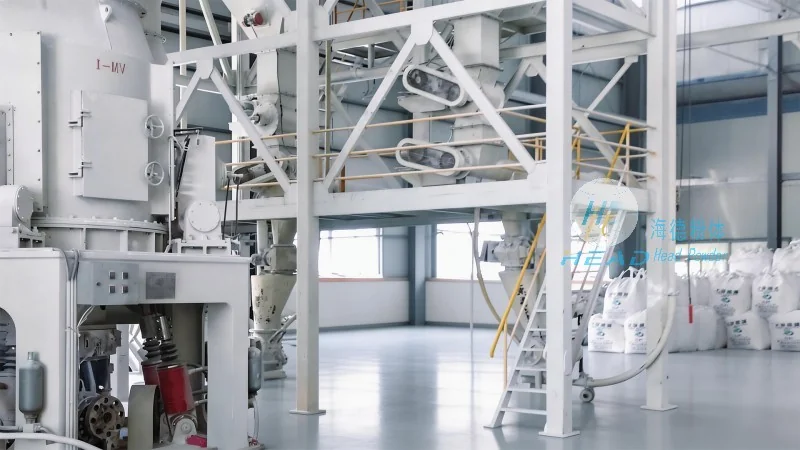
The negative pressure dilute phase powder pneumatic conveying line is widely used in various industrial sectors where the transport of fine powders is critical. In the chemical industry, it is commonly employed to transfer raw materials such as powders, granules, and slurries between processing units, ensuring a continuous and clean production flow. The food and pharmaceutical industries also benefit from this technology, as it maintains strict hygiene standards and prevents cross-contamination during material transfer. In the mining sector, the system is used to transport ore powders from processing plants to storage facilities or for further processing. The system's ability to handle abrasive materials without causing wear and tear on the equipment makes it ideal for applications in the cement and construction industries as well. Furthermore, in the agricultural sector, it can be used to transport fertilizers, seeds, and other agricultural products, enhancing efficiency in farming operations.
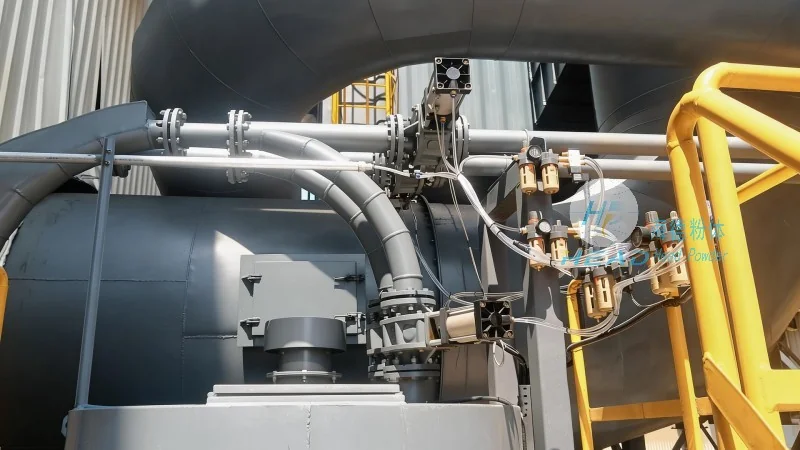
While the negative pressure dilute phase system offers numerous benefits, proper operation and maintenance are essential to ensure optimal performance and longevity. Regular inspection of the vacuum pump and conveying line for leaks is crucial, as even small leaks can compromise the system's efficiency and increase energy consumption. The feed hopper and discharge receiver should be cleaned regularly to prevent material buildup and ensure consistent flow. Additionally, the system's filters and cyclones should be maintained to prevent clogging and maintain the quality of the conveyed material. HeadPowder provides comprehensive maintenance services and technical support to ensure that their systems operate at peak efficiency, minimizing downtime and maximizing productivity for their clients.
HeadPowder's negative pressure dilute phase powder pneumatic conveying line represents a sophisticated solution for the efficient and reliable transport of fine powders and granular materials. By leveraging the principles of negative pressure and dilute phase operation, this system offers superior performance, environmental benefits, and flexibility for a wide range of industrial applications. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide high-quality engineering solutions that meet the evolving needs of the industry, ensuring that their clients achieve optimal material handling efficiency and cost-effectiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top