When it comes to efficiently handling and transporting rice husk, air-flow conveying systems offer a reliable and efficient solution. These systems utilize the principle of pneumatic transport, where material is moved through a pipeline using compressed air or other gas streams. For industries dealing with rice husk, understanding the key air-flow conveying structures is crucial for optimizing processing and material handling operations.
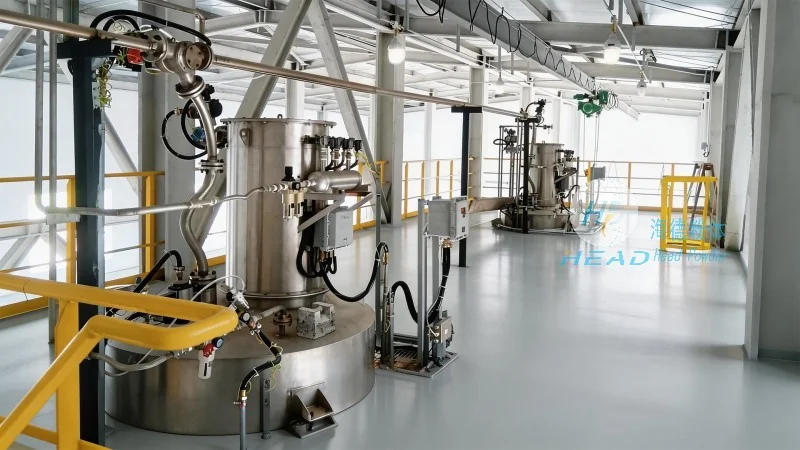
The core components of an air-flow conveying system for rice husk typically include the hopper, feeder, pipeline, and discharge device. The hopper serves as the storage and feeding unit, ensuring a consistent flow of rice husk into the system. The feeder, often a rotary valve or screw feeder, regulates the material flow rate to match the conveying requirements. The pipeline, usually made of stainless steel or other corrosion-resistant materials, carries the rice husk and air mixture. The discharge device, such as a rotary valve or a cyclone separator, separates the material from the air at the end of the pipeline.
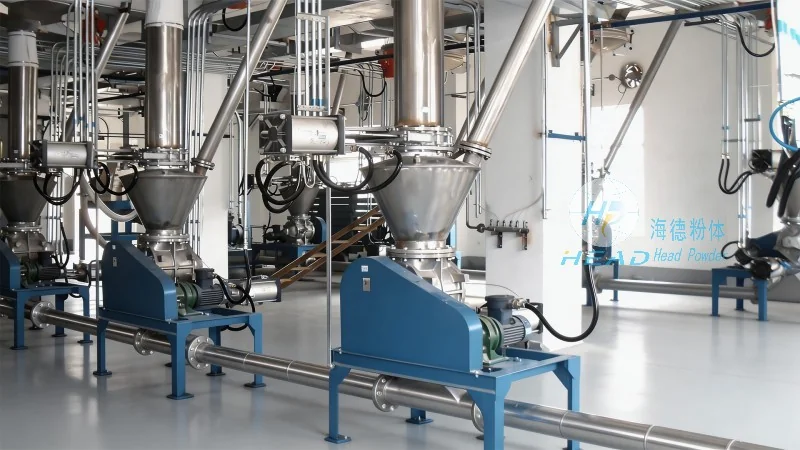
There are several types of air-flow conveying structures commonly used for rice husk, each with its own advantages and applications. The most common types include the positive pressure system, where compressed air is used to push the material through the pipeline, and the negative pressure system, where a vacuum is created to pull the material. Another type is the mixed flow system, which combines both positive and negative pressure elements for more flexible operation. Each type of system is designed to handle different particle sizes and flow rates of rice husk, ensuring optimal performance in various industrial settings.
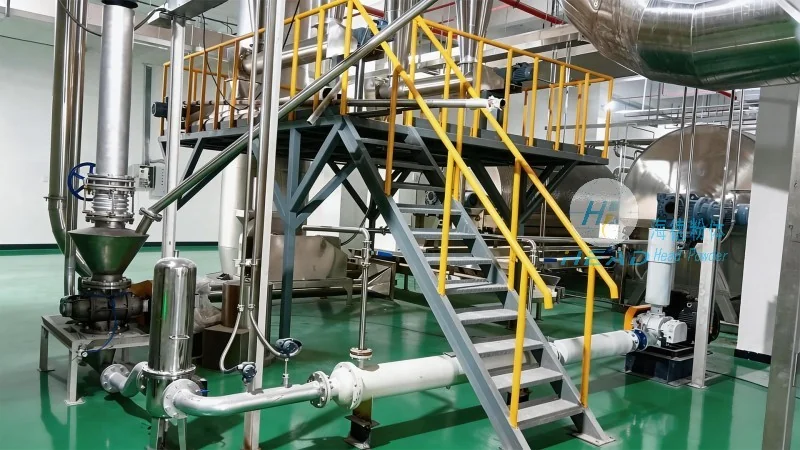
Implementing air-flow conveying structures for rice husk offers numerous benefits. Firstly, these systems provide a dust-free and hygienic environment, which is essential for food processing industries. Secondly, they offer high efficiency in material transport, with minimal material loss and low maintenance requirements. Additionally, air-flow conveying systems are capable of handling large volumes of rice husk, making them suitable for high-capacity processing plants. The flexibility of these systems allows for easy integration with existing processing lines, reducing downtime and increasing overall productivity.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in designing and manufacturing customized air-flow conveying structures tailored to the specific needs of rice husk processing facilities. The company’s expertise lies in understanding the unique challenges of handling rice husk, such as its lightweight and abrasive nature, and developing solutions that address these issues effectively. With a focus on quality and durability, HeadPowder provides systems that are built to withstand the demands of continuous operation in industrial environments. The company’s team of engineers works closely with clients to assess their requirements, from material flow rates to pipeline lengths, and designs a system that maximizes efficiency and minimizes operational costs.
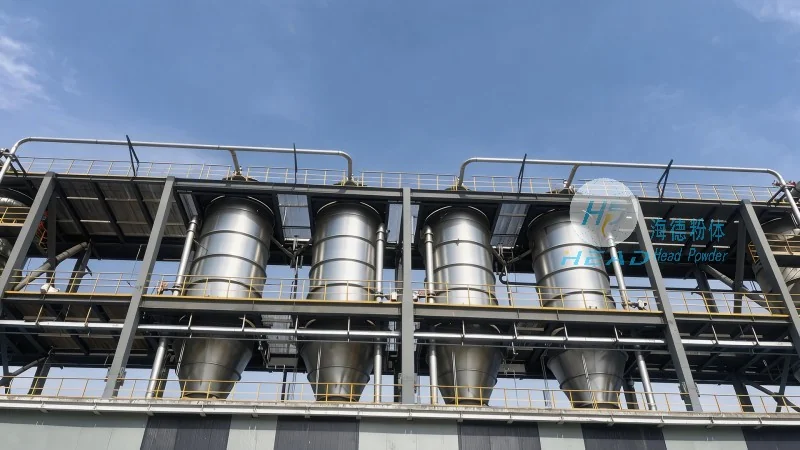
For industries seeking reliable and efficient air-flow conveying solutions for rice husk, Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner. By leveraging their expertise in pneumatic transport systems, the company offers customized solutions that enhance productivity and ensure compliance with industry standards. With a commitment to quality and customer satisfaction, HeadPowder continues to provide innovative solutions for the rice husk processing industry. For more information or to discuss your specific conveying needs, please contact the company at their address in Shandong, China.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top