HeadPowder, a leading provider of industrial dust collection solutions, specializes in advanced material conveying systems designed to enhance efficiency and safety in dust collection operations. The equipment is engineered to handle various bulk materials, ensuring reliable transport from dust collection points to processing or storage areas. This section explores the fundamental principles behind these systems and highlights key working scene characteristics that make them indispensable in modern industrial applications, all while adhering to the high standards set by Shandong HeadPowder Engineering Co., Ltd. based in China.
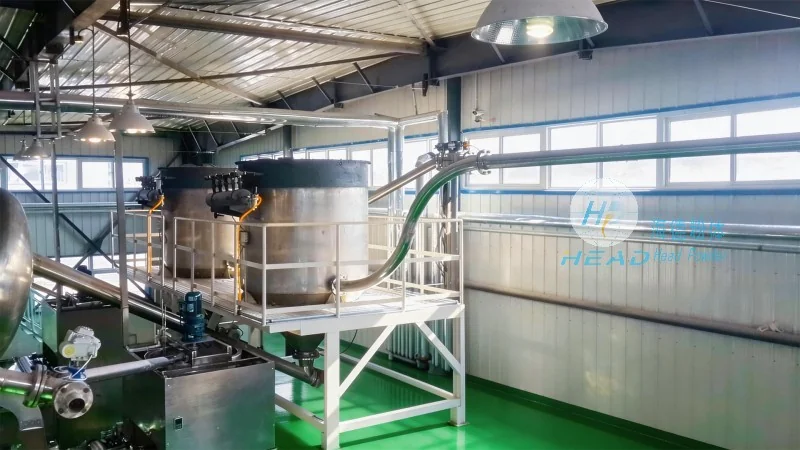
The core principle of material conveying equipment for dust collection stations revolves around the efficient transfer of bulk materials while maintaining air quality and operational safety. These systems typically integrate with dust collection units to capture particulate matter and then transport the collected material through a sealed or controlled environment. The equipment employs various mechanisms such as screw conveyors, belt conveyors, or pneumatic systems to move materials without exposing personnel to dust or contaminants. The design emphasizes minimal air leakage and consistent material flow, which are critical for maintaining the effectiveness of dust control measures. By integrating with dust collection systems, the conveying equipment ensures that the entire process—from collection to transport—remains enclosed and controlled, reducing the risk of dust dispersion and improving overall workplace safety.
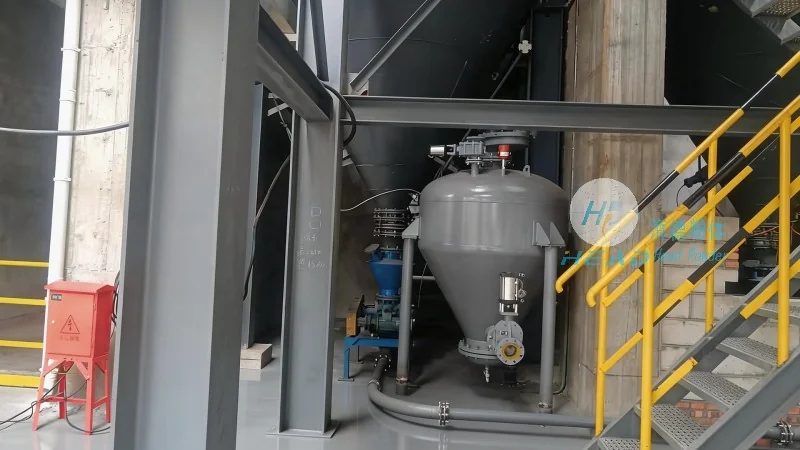
The working scene characteristics of material conveying equipment for dust collection stations are tailored to meet the specific demands of industrial environments. These systems are often deployed in settings where large volumes of bulk materials are processed, such as in mining, manufacturing, or construction industries. The equipment is designed to operate in harsh conditions, including high temperatures, dust-laden atmospheres, and heavy loads, ensuring durability and reliability. Key characteristics include: seamless integration with dust collection units, which allows for a continuous flow of material without interruptions; flexible conveying options, such as adjustable speed and direction controls, to accommodate different material types and processing requirements; and robust construction, with corrosion-resistant materials and protective enclosures to withstand the rigors of industrial use. Additionally, the equipment is engineered to minimize maintenance requirements, reducing downtime and operational costs. The working scenes typically involve automated or semi-automated processes, where the conveying system works in tandem with other industrial machinery to streamline material handling and improve overall productivity.
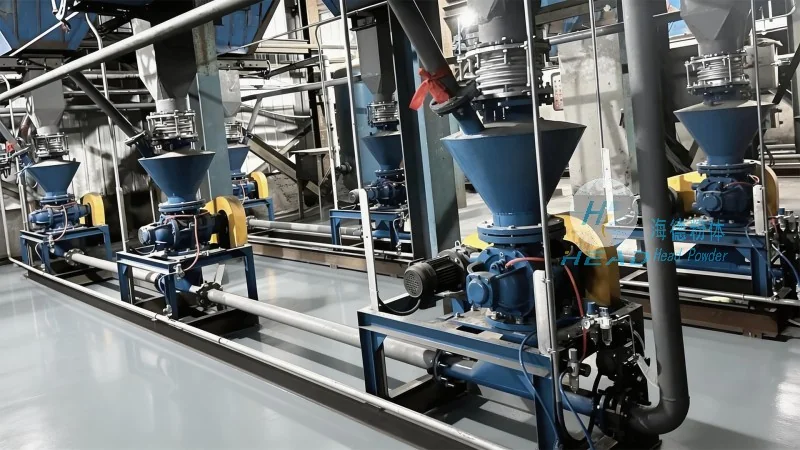
Material conveying equipment for dust collection stations is widely used in various application scenarios across different industries. For instance, in mining operations, the equipment efficiently transports ore or rock from dust collection points to processing facilities, ensuring that the material is handled safely and without exposing workers to harmful dust. In manufacturing plants, it is used to move raw materials or finished products through dust collection systems, maintaining a clean and controlled environment. The operational benefits of these systems are significant, including: enhanced workplace safety by reducing dust exposure; improved air quality by preventing dust dispersion into the environment; and increased efficiency through automated material handling. The equipment also contributes to cost savings by minimizing material loss and reducing the need for manual handling, which can be hazardous and time-consuming. Furthermore, the systems are designed to be scalable, allowing them to adapt to changing production needs and growing operational demands. This flexibility makes them suitable for both small-scale and large-scale industrial applications.
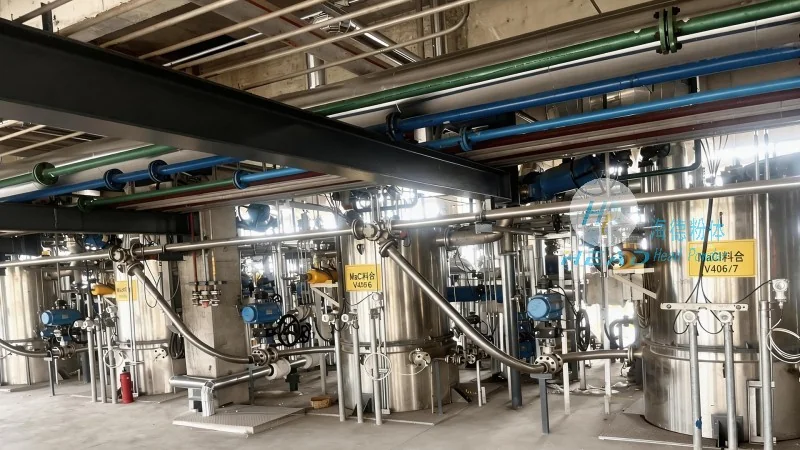
The technical specifications and design considerations of material conveying equipment for dust collection stations are critical to their performance and reliability. The equipment is typically designed with components that can withstand high temperatures, abrasive materials, and corrosive environments. For example, screw conveyors may use stainless steel or high-strength polymers to resist wear and corrosion, while belt conveyors employ durable rubber or synthetic materials to handle heavy loads. The design also incorporates features such as sealed housings and dust-tight connections to prevent air leakage and maintain the integrity of the dust collection system. The control systems are often equipped with sensors and monitoring devices to track material flow, detect blockages, and adjust operational parameters in real-time. This ensures that the system operates optimally and alerts operators to any issues that may affect performance. Additionally, the equipment is designed for easy maintenance, with accessible components and modular designs that allow for quick repairs and replacements. The technical specifications may vary based on the specific application, but all systems are engineered to meet industry standards for safety and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top