Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and integration of advanced material handling solutions, including automatic weighing material conveying systems. These systems are engineered to enhance efficiency and accuracy in various industrial applications by combining precise weighing technology with reliable material transport mechanisms.
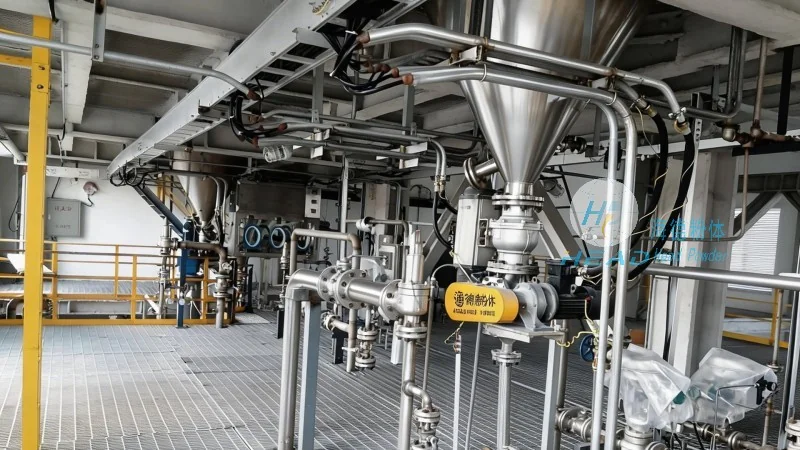
Automatic weighing material conveying systems are sophisticated equipment designed to transport bulk materials while simultaneously measuring their weight. The core components typically include a conveyor mechanism, load cells for weight measurement, control systems, and integration with other industrial processes. Such systems are crucial in industries where material handling and weight accuracy are paramount, such as pharmaceuticals, food processing, chemicals, and mining.
The fundamental principle of these systems revolves around the integration of weighing technology with material transport. The conveyor transports the material through a path where load cells are strategically placed to capture the weight data. The load cells convert the mechanical force of the material into electrical signals, which are then processed by a control unit to provide real-time weight measurements. This process ensures that the material is weighed as it moves, eliminating the need for separate weighing stations and reducing handling time. The control system may also incorporate features like data logging, alarm settings for weight deviations, and integration with other equipment for automated decision-making.
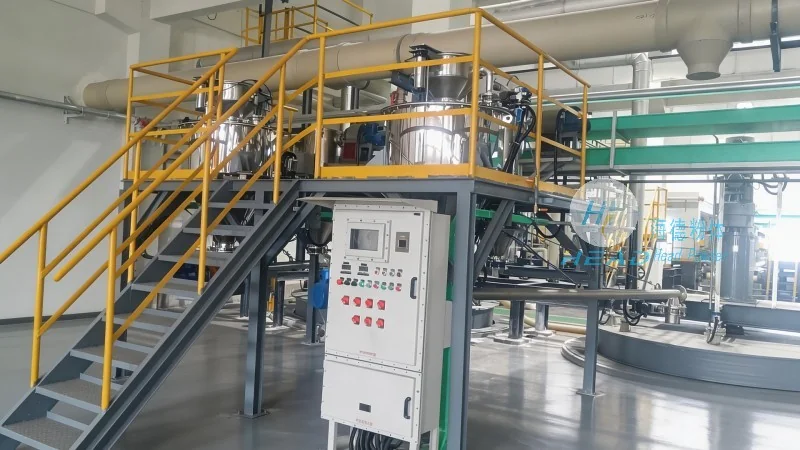
The working scene characteristics of automatic weighing material conveying systems are tailored to meet the demands of specific industrial environments. These systems are designed to operate in environments with varying material types, flow rates, and environmental conditions. For instance, in pharmaceutical manufacturing, the systems must adhere to stringent hygiene standards, often featuring stainless steel construction and easy-to-clean surfaces. In food processing plants, the equipment is built to handle food-grade materials, with sealed components to prevent contamination. The flexibility of these systems allows them to adapt to different production line configurations, whether in a continuous or batch processing mode. Additionally, the systems are engineered for durability and low maintenance, ensuring consistent performance over extended operational periods.
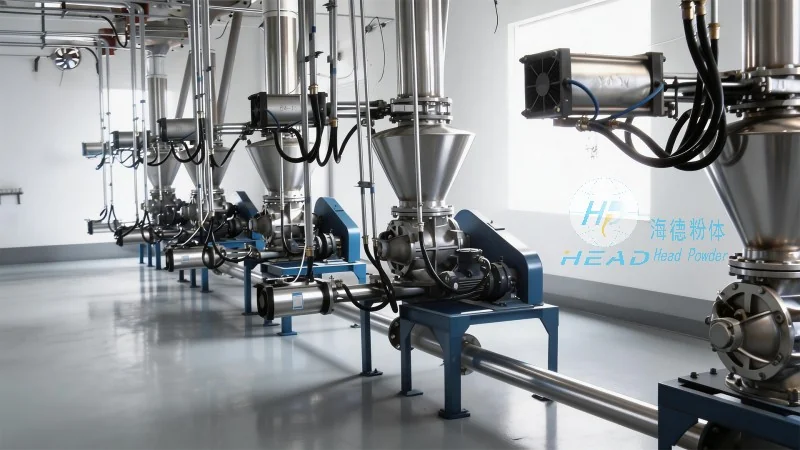
Automatic weighing material conveying systems find widespread application across multiple industries, significantly improving operational efficiency and product quality. In the chemical industry, these systems help in the precise measurement of raw materials, reducing waste and ensuring compliance with regulatory standards. In the mining sector, they are used to transport and weigh ore, facilitating better inventory management and process optimization. The systems also contribute to cost reduction by minimizing manual handling errors and increasing throughput. Furthermore, the integration of weighing and conveying capabilities streamlines production workflows, enabling manufacturers to achieve higher productivity and better resource utilization.
Recent advancements in technology have further enhanced the capabilities of automatic weighing material conveying systems. The adoption of digital load cells and advanced control software has improved measurement accuracy and response time. The integration of IoT (Internet of Things) technologies allows for remote monitoring and predictive maintenance, reducing downtime and maintenance costs. Additionally, the use of automation and artificial intelligence in these systems enables smarter decision-making, such as adjusting conveyor speed based on real-time weight data or detecting anomalies in material flow. As industries continue to evolve, the demand for more intelligent and adaptive material handling solutions is expected to grow, driving further innovation in automatic weighing material conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top