HeadPowder, a leading provider in the material handling industry, specializes in the design and manufacturing of efficient stone material conveying systems. This article delves into the fundamental principles behind these systems and highlights their key working scene characteristics, offering insights into their practical applications and operational benefits.
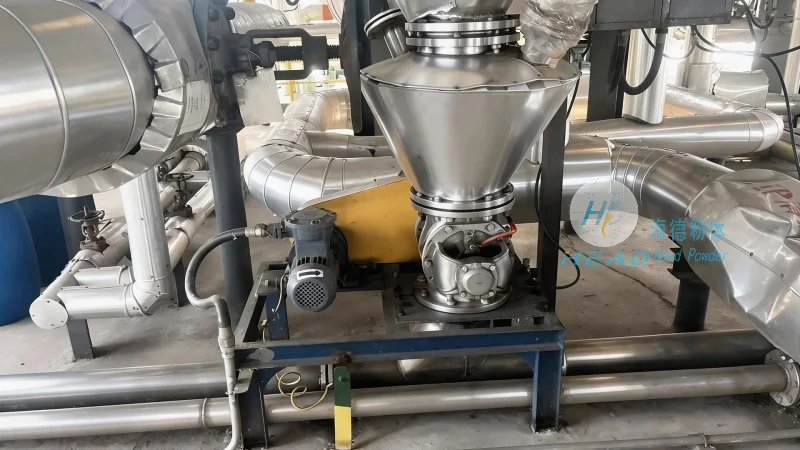
Stone material conveying lines are essential equipment used in various industrial sectors, particularly in the construction, mining, and aggregate processing industries. These systems are engineered to transport bulk materials such as crushed stone, gravel, and sand from one location to another with precision and reliability. The core function of a stone material conveying line is to move these materials through a series of components, including feeders, conveyors, and control mechanisms, ensuring smooth and continuous operation. HeadPowder, as a reputable manufacturer based in Shandong, China, has developed advanced solutions tailored to meet the diverse needs of clients in these industries.
The operation of a stone material conveying line is based on mechanical principles that facilitate the movement of bulk materials. Typically, these systems utilize gravity, belt tension, or motor-driven mechanisms to transport materials. The process begins with the material being fed into the system, often through a hopper or feeder, which regulates the flow rate. From there, the material is transferred onto a conveyor belt or other transport medium, which moves it along the designated path. The design of the conveying line, including the type of conveyor (e.g., belt, screw, or chain), is selected based on the material characteristics, such as size, weight, and abrasiveness. For instance, belt conveyors are commonly used for transporting larger stone pieces due to their high load capacity and durability, while screw conveyors are suitable for finer materials like sand or gravel. The control system, which may include sensors and variable speed drives, ensures that the conveying process is optimized for efficiency and safety. HeadPowder’s expertise lies in integrating these components into a cohesive system that maximizes performance while minimizing downtime.
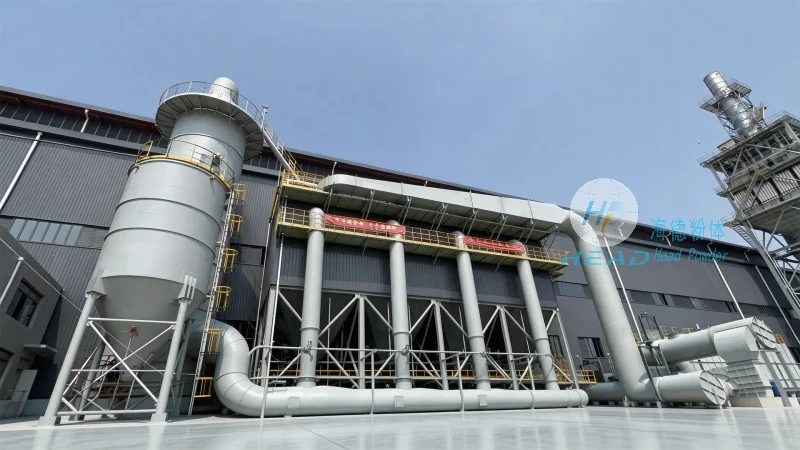
The working scene characteristics of stone material conveying lines are influenced by several factors, including the environment, material properties, and operational requirements. In industrial settings, these systems are often deployed in environments with high dust levels or extreme temperatures, requiring robust construction and effective dust control measures. The design of the conveying line must account for these conditions to ensure long-term reliability. For example, in mining operations, where materials are extracted from underground, the conveying line may need to handle wet or contaminated stone, necessitating the use of specialized materials and sealing techniques. In construction sites, the conveying line may be used to transport aggregates to different parts of the site, requiring flexibility in terms of layout and adaptability to changing work conditions. HeadPowder’s solutions are designed to address these diverse working scene characteristics, providing customized systems that meet the specific needs of each application. The company’s focus on durability and efficiency ensures that their conveying lines can withstand harsh conditions while maintaining optimal performance.
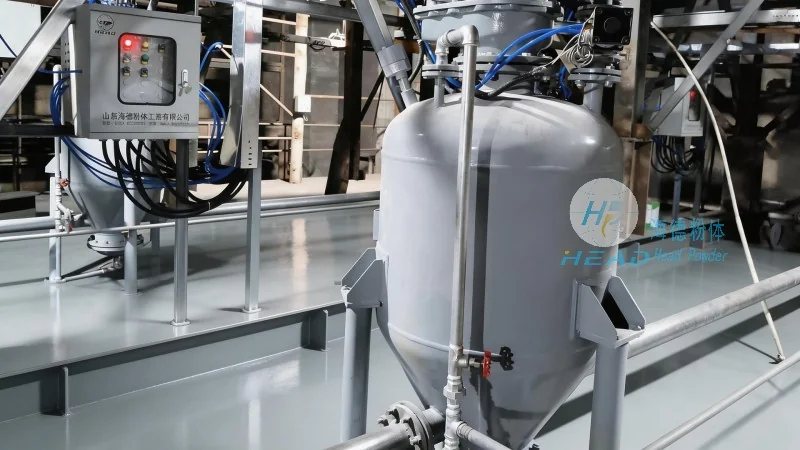
Stone material conveying lines offer several key features and benefits that make them indispensable in industrial operations. One of the primary advantages is their ability to handle large volumes of material with minimal labor requirements. This automation reduces operational costs and improves productivity, allowing businesses to scale their operations efficiently. Additionally, these systems provide consistent material flow, which is crucial for maintaining production schedules and meeting quality standards. The modular design of many stone material conveying lines allows for easy integration with existing equipment and facilitates maintenance, as components can be replaced or upgraded without disrupting the entire system. HeadPowder’s products are known for their high efficiency, durability, and low maintenance requirements, contributing to their widespread adoption in the industry. The company’s commitment to innovation ensures that their conveying lines incorporate the latest technologies, such as advanced control systems and energy-efficient motors, further enhancing their performance and reducing operational costs.
In conclusion, stone material conveying lines are critical components in the material handling processes of various industries. The principles of operation, combined with the working scene characteristics, determine the effectiveness and efficiency of these systems. HeadPowder, with its expertise and commitment to quality, provides reliable and customized solutions that meet the diverse needs of clients. By understanding the fundamental principles and characteristics of these systems, businesses can make informed decisions when selecting and implementing stone material conveying lines, ultimately enhancing their operational performance and productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top