Desulfurization and dust removal processes in industrial facilities generate large volumes of ash and dust that require efficient and reliable material handling solutions. The material conveying lines designed for this application play a crucial role in transporting these byproducts from the collection points to disposal or recycling facilities. This article explores the fundamental principles behind these conveying systems and highlights the key characteristics of their working environments.
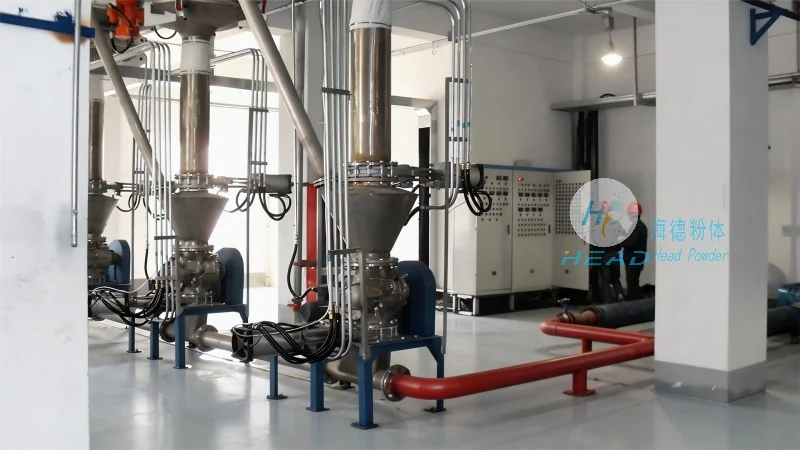
The core principle of desulfurization and dust removal ash material conveying lines is to transport fine particulate materials, such as fly ash from flue gas desulfurization (FGD) systems, using mechanical or pneumatic methods. These systems typically consist of components like hoppers, feeders, conveyors (e.g., belt conveyors, screw conveyors, or pneumatic pipelines), and control systems. The operation involves the controlled feeding of ash from the collection hopper into the conveyor, which then transports it to the discharge point. The design ensures minimal material loss, proper air sealing to prevent dust emissions, and compliance with environmental regulations. The conveying process is often automated, with sensors and control panels monitoring flow rates, pressure, and other critical parameters to maintain optimal performance.
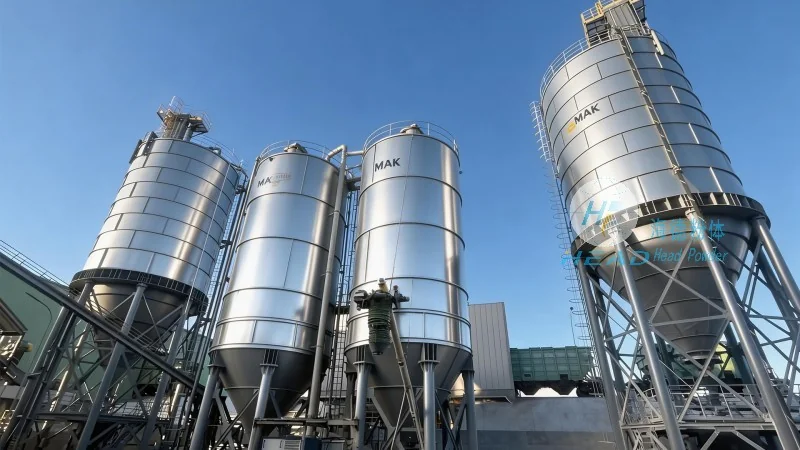
The working environment for desulfurization and dust removal ash material conveying lines is characterized by several unique factors that influence system design and operation. First, the material being handled is often fine and abrasive, which can cause wear on conveyor components and require specialized materials for construction. Second, the systems operate in industrial settings where space constraints and integration with existing plant infrastructure are common considerations. Third, environmental regulations mandate strict control over dust emissions, necessitating enclosed or sealed conveyor designs with effective dust collection and filtration systems. Additionally, the conveying lines may need to handle varying material loads and moisture content, which affects the selection of conveyor type and maintenance requirements. The working scene also includes considerations for safety, as the material can be hazardous if not handled properly, and for energy efficiency, as the operation of these systems contributes to the overall cost of ash management.
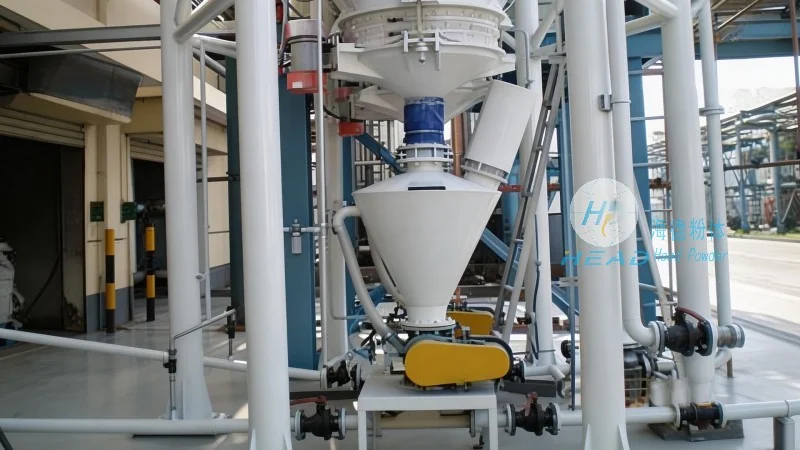
Several critical components make up a typical desulfurization and dust removal ash material conveying line. The hopper serves as the collection point, where ash accumulates from the desulfurization process. The feeder, often a rotary valve or a belt feeder, regulates the flow of ash from the hopper into the conveyor, ensuring a consistent feed rate. The conveyor itself, whether a belt conveyor with idlers and pulleys, a screw conveyor for vertical or horizontal transport, or a pneumatic system using air pressure to move material through pipelines, is the primary transport mechanism. The control system, including sensors for level, pressure, and flow, and a control panel for operation, monitors and adjusts the system to maintain optimal performance. The dust collection and sealing system, which may include filters, fans, and airlocks, prevents dust emissions and maintains a safe working environment. Each component is designed to withstand the abrasive nature of the ash and operate reliably under continuous industrial conditions.
Desulfurization and dust removal ash material conveying lines are used in various industrial applications, including power plants, cement factories, and waste-to-energy facilities. In power plants, these systems transport fly ash from the FGD system to storage silos or disposal sites, ensuring that the ash is handled safely and efficiently. In cement factories, the conveying lines move ash from the kiln or preheater system to the clinker production process, where it can be used as a supplementary cementitious material. The efficiency of these systems is crucial for the overall operation of the plant, as downtime or inefficiencies can lead to increased costs and environmental compliance issues. The design of the conveying line, including the selection of conveyor type and the layout of components, is tailored to the specific application to maximize throughput and minimize energy consumption. Regular maintenance and monitoring are essential to ensure the system operates at peak efficiency and meets all regulatory requirements.
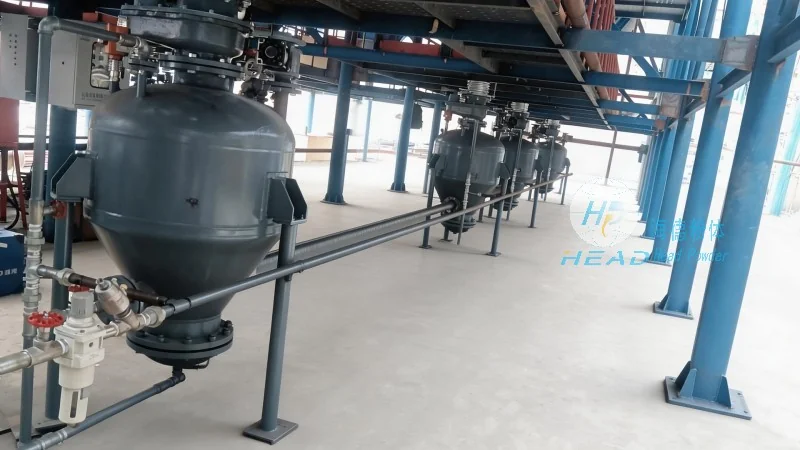
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of industrial material handling equipment, specializing in solutions for desulfurization and dust removal ash management. With a focus on innovation and quality, the company designs and manufactures conveying lines that meet the highest standards of performance and reliability. Headpowder's products are used in various industrial sectors, providing efficient and environmentally friendly solutions for ash handling. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to developing advanced material handling systems. By combining expertise in mechanical design, material science, and industrial automation, headpowder delivers customized solutions that address the unique challenges of each application. The company's commitment to customer satisfaction and environmental responsibility has established it as a trusted partner in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top