Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading enterprise in industrial automation solutions based in Shandong, China. The company specializes in the design, development, and deployment of advanced material handling systems, including intelligent unpacking and conveying technologies. This article explores the core principles and operational characteristics of intelligent unpacking material conveying systems, highlighting their role in enhancing efficiency and productivity across diverse industrial applications.
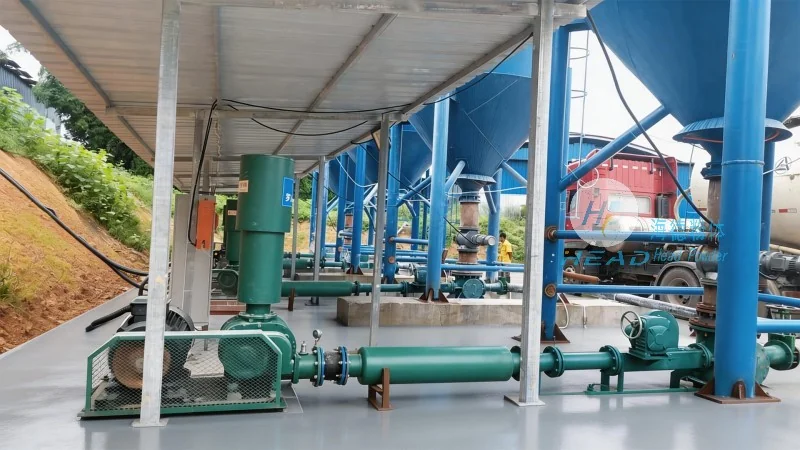
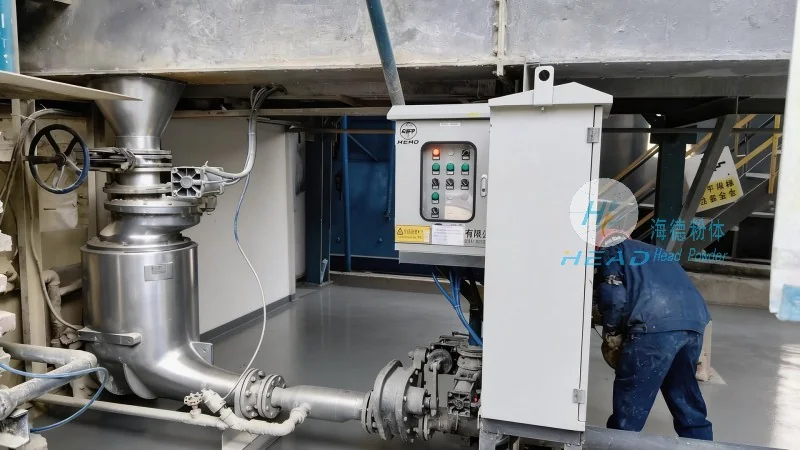
The intelligent unpacking material conveying system operates on a sophisticated technological framework that integrates robotics, sensor technology, and artificial intelligence. At its core, the system employs machine vision and image recognition algorithms to identify and classify packaged items as they move along the conveyor. This visual data is processed in real-time, enabling the system to determine the appropriate handling method for each item—whether it requires opening, sorting, or direct transfer to the next stage of production. The system integrates automated robotic arms or specialized grippers equipped with force sensors and tactile feedback to handle items gently and accurately, minimizing damage to sensitive materials. Additionally, the system incorporates a network of sensors, including laser scanners and proximity detectors, to monitor the position and movement of items throughout the conveying process. These sensors provide critical data for the control system, which adjusts the speed and direction of the conveyor and robotic actions to maintain optimal flow and prevent bottlenecks. The integration of machine learning algorithms allows the system to learn from past operations, improving its performance over time and adapting to new or changing material types without manual reconfiguration.
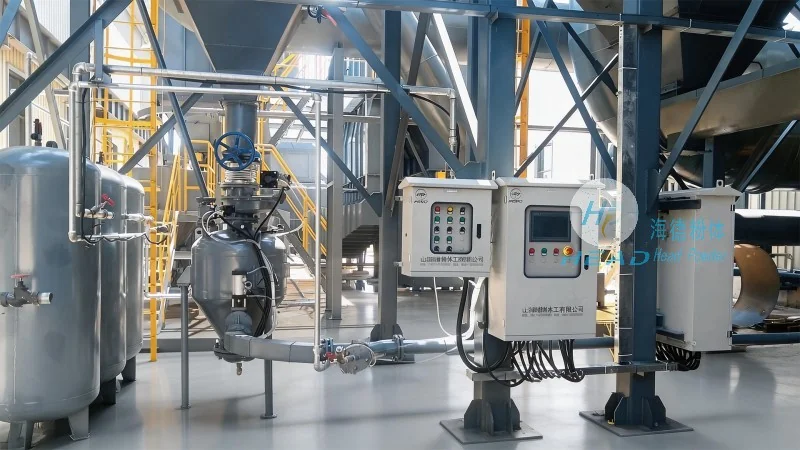
The intelligent unpacking material conveying system is designed to address the challenges of manual material handling in modern industrial settings. Its primary operational scenarios include high-volume manufacturing plants, where it automates the flow of raw materials from receiving to processing, and distribution centers, where it streamlines the unpacking and sorting of incoming goods for order fulfillment. The system's modular design enables seamless integration with existing conveyor networks and automation infrastructure, reducing installation time and costs. In manufacturing environments, the system enhances productivity by reducing labor requirements and minimizing human error, allowing production lines to operate at higher speeds with consistent accuracy. The system's adaptability is further demonstrated in its ability to handle diverse packaging types—such as boxes, bags, and containers—as well as irregularly shaped items, through flexible gripper designs and adjustable processing parameters. Safety is a key feature, with built-in collision detection and emergency stop mechanisms that protect both personnel and equipment during operation. The real-time monitoring capabilities provide operators with visibility into the entire conveying process, enabling quick identification and resolution of issues to maintain continuous operation. Overall, the intelligent unpacking material conveying system represents a significant advancement in industrial automation, offering a reliable and efficient solution for material handling needs.
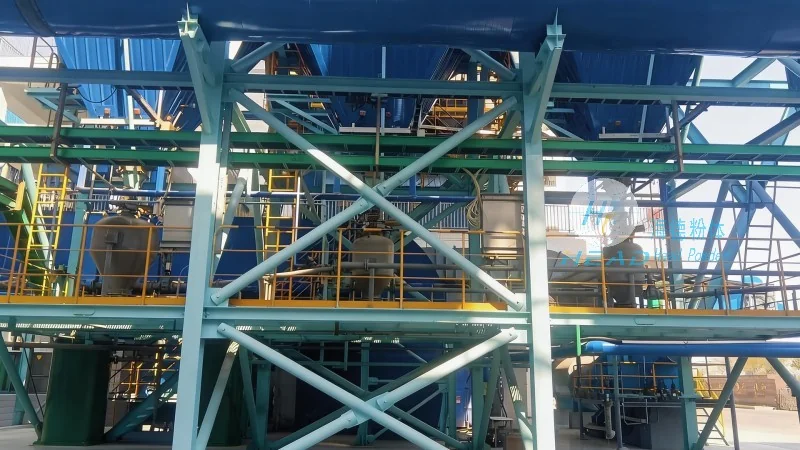
The implementation of intelligent unpacking material conveying systems brings numerous benefits to industrial operations. By automating the unpacking and conveying process, companies can reduce labor costs and minimize the risk of human error, which is particularly critical in industries like pharmaceuticals, electronics, and food processing where precision and consistency are paramount. The system's ability to handle high volumes of materials with consistent accuracy improves overall throughput and reduces downtime caused by material jams or misdirected items. Additionally, the system's adaptability allows it to be reconfigured for different production runs or product changes, providing flexibility in dynamic manufacturing environments. In distribution centers, the system accelerates order processing by quickly sorting and routing items to their respective destinations, enhancing customer satisfaction and operational efficiency. The integration of advanced technologies, such as AI and machine vision, ensures that the system can evolve with technological advancements, maintaining its relevance and effectiveness over time. For companies seeking to optimize their material handling processes and enhance productivity, the intelligent unpacking material conveying system from Shandong HeadPowder Engineering Co., Ltd. offers a robust and reliable solution.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top