HeadPowder, a leading provider in the material handling industry, specializes in vacuum suction systems designed to efficiently transport bulk materials over long distances. This article delves into the fundamental principles of these systems and highlights their key working scene characteristics, offering insights into how they enhance operational efficiency in various industrial applications.
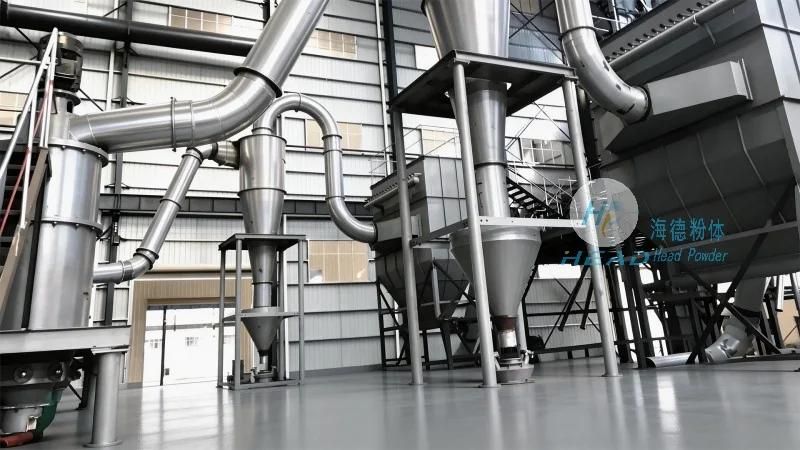
The vacuum suction system operates on the principle of creating a pressure differential between the material source and the receiving point. By generating a negative pressure (vacuum) at the material inlet, the system draws particles or bulk materials into the suction pipe. This process relies on the pressure difference to move materials without the need for mechanical conveyors or positive pressure systems. The system typically includes a vacuum pump, suction nozzles, and a pipeline network that connects the material source to the destination. The vacuum pump maintains the necessary pressure gradient, ensuring continuous material flow. The design allows for flexible and low-cost installation, as it does not require complex infrastructure like traditional belt conveyors or screw conveyors.
1. **Low Noise and Vibration Operation**: Vacuum suction systems operate with minimal noise and vibration, making them suitable for environments where noise control is critical, such as food processing facilities or pharmaceutical plants. The absence of moving parts like belts or gears reduces operational noise, contributing to a safer and more comfortable working environment.
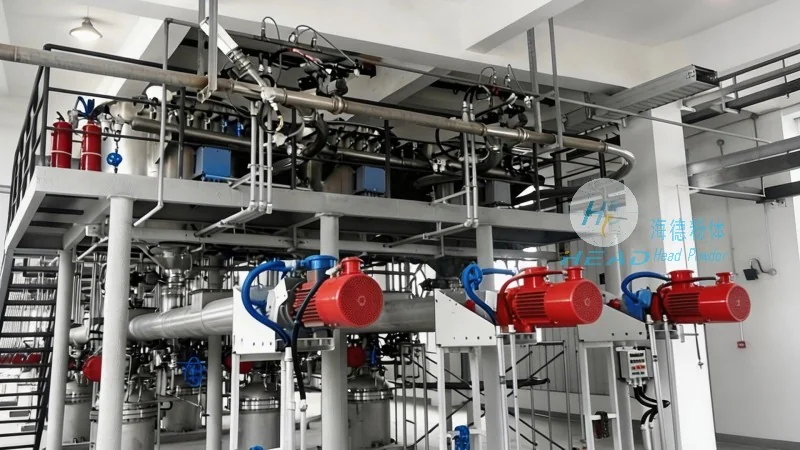
2. **Flexible Material Handling**: These systems are highly adaptable to various materials, including powders, granules, and small particles. The flexible suction nozzles can be positioned to access hard-to-reach areas, allowing for efficient collection from silos, hoppers, or even outdoor stockpiles. This flexibility is particularly valuable in applications where material sources are irregular or change frequently.
3. **Reduced Downtime and Maintenance**: Unlike mechanical conveyors that may experience downtime due to belt wear or blockages, vacuum suction systems have fewer moving parts and are less prone to clogs. The self-cleaning design of the suction nozzles minimizes maintenance requirements, leading to lower operational costs and increased system reliability. This makes them ideal for continuous production lines where downtime is costly.
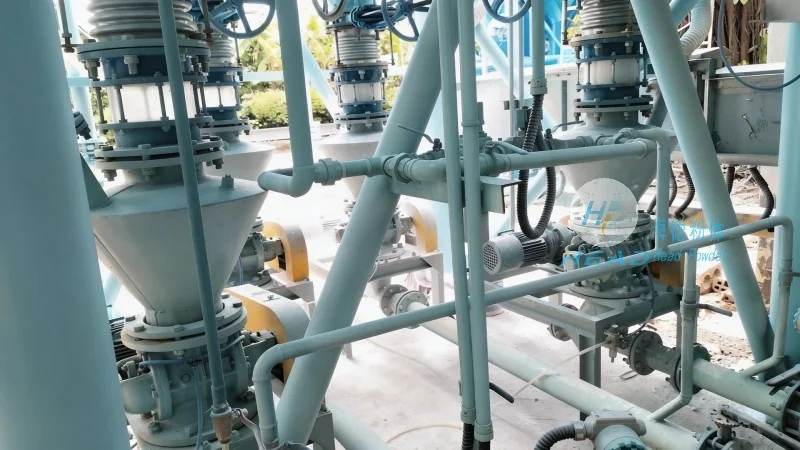
4. **Environmental Benefits**: By eliminating the need for dust containment systems or enclosed conveyors, vacuum suction systems contribute to a cleaner working environment. The negative pressure ensures that dust and particles are contained within the system, reducing air pollution and improving indoor air quality. This is especially beneficial in industries where air quality regulations are stringent.
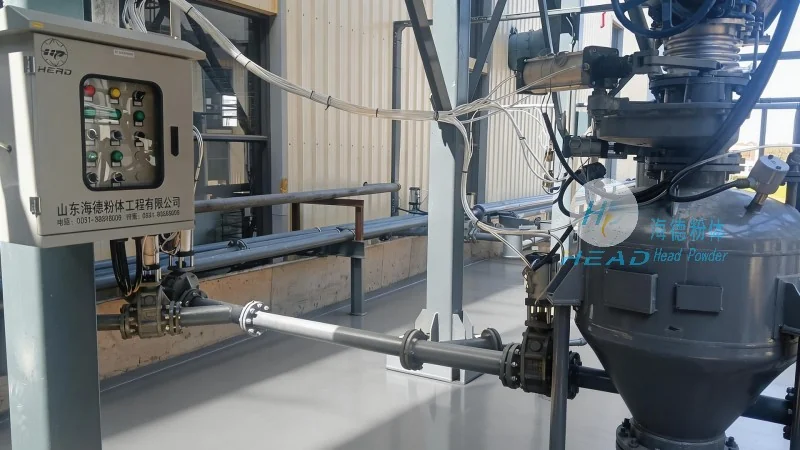
HeadPowder's vacuum suction systems are widely used in diverse industrial sectors, including food processing, pharmaceutical manufacturing, chemical processing, and mining. In food processing plants, they are employed to transport flour, sugar, and other dry ingredients from storage silos to production lines, ensuring hygienic and efficient material flow. In pharmaceutical facilities, the systems are used to handle active pharmaceutical ingredients (APIs) and excipients, maintaining strict contamination control and compliance with GMP (Good Manufacturing Practice) standards. The chemical industry utilizes these systems for transporting powders like pigments, catalysts, and reagents, where precise dosing and minimal material loss are critical. In mining operations, vacuum suction systems are effective for transporting ore dust and tailings, reducing the risk of dust-related health issues and improving workplace safety.
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to innovate in vacuum suction material handling technology, providing reliable and efficient solutions for modern industrial needs. The principles of pressure differential and flexible design make these systems a superior choice for applications requiring low noise, minimal maintenance, and environmental compliance. By understanding the core principles and working scene characteristics, industries can optimize their material handling processes, enhancing productivity and operational safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top