Understanding the principles and operational characteristics of cement particle material conveying is crucial for optimizing industrial processes in construction and manufacturing sectors. This article explores the fundamental mechanisms behind cement particle transport systems, alongside key features of their application environments. The information presented is tailored to assist professionals seeking to enhance efficiency and reliability in material handling operations, with a focus on the specific needs of cement and similar granular materials.
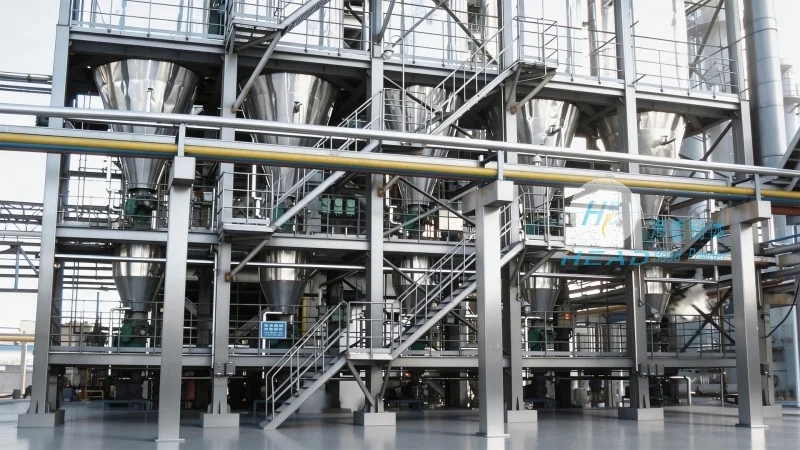
Cement particle material conveying systems are engineered to transport bulk cement and other granular materials from storage silos or production sites to processing or packaging areas. These systems are integral to the supply chain of cement manufacturing, ensuring a continuous and efficient flow of material. The design of such systems typically involves a combination of mechanical components, such as hoppers, feeders, and conveyor belts or pipes, which work in tandem to move the material through the system. The primary goal is to maintain material integrity, minimize dust generation, and achieve consistent flow rates, all of which are critical for downstream processes like mixing and packaging.
The fundamental principles of cement particle material conveying revolve around the mechanics of bulk material movement. Key factors include the material's density, particle size distribution, and flow properties, which influence how the material behaves under the action of gravity, pressure, or mechanical force. In many systems, a combination of gravity and mechanical assistance is used to move the material. For instance, vertical conveyors may employ screw or auger mechanisms to lift the material, while horizontal systems often utilize belt conveyors or pneumatic pipelines. The selection of the conveying method depends on factors like the distance to be covered, the volume of material to be moved, and the need to maintain material quality. The principle of minimizing friction and ensuring a smooth transition between components is also vital to prevent material degradation or blockages.
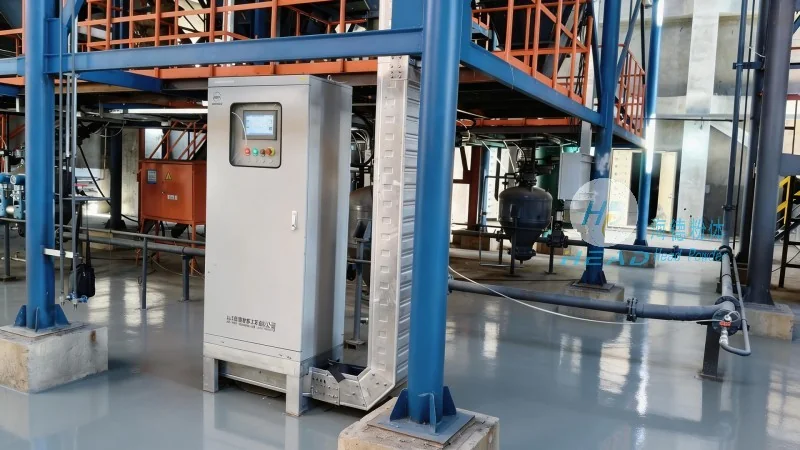
The operational scenes where cement particle material conveying systems are deployed exhibit distinct characteristics that impact system design and performance. Industrial plants, such as cement production facilities or large-scale construction sites, are typical environments. These settings often involve high-volume material handling, requiring robust and durable equipment capable of withstanding heavy usage and harsh conditions. The working environment may include exposure to dust, moisture, and temperature variations, which necessitates the use of materials and designs that are resistant to corrosion and wear. Additionally, the need for safety and compliance with industrial standards is paramount, as these systems handle large quantities of material that could pose risks if not managed properly.
Several key features define the operational environments where cement particle conveying systems operate. Firstly, the scale of operations is significant, with systems often designed to handle thousands of tons of material per day. This requires high-capacity components, such as large hoppers and wide conveyor belts, to ensure efficient throughput. Secondly, the need for reliability and minimal downtime is critical, as any interruption in material flow can disrupt production schedules. Therefore, redundancy and maintenance-friendly designs are common features. Thirdly, the integration with other industrial processes is essential. Cement particle conveyors are often part of a larger production line that includes mixing, grinding, and packaging, requiring seamless coordination between different stages. Finally, environmental considerations play a role, as modern systems are designed to minimize dust emissions and comply with environmental regulations, contributing to a safer and more sustainable operation.
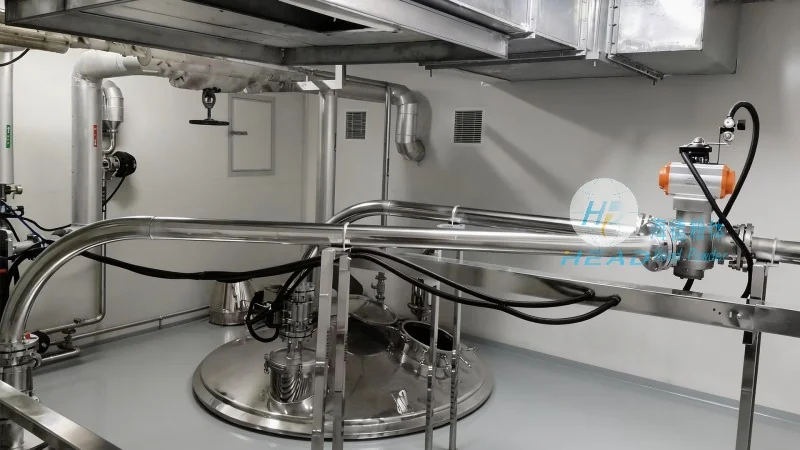
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized material handling solutions, including cement particle conveying systems. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner in the construction and manufacturing industries. HeadPowder's expertise lies in designing and manufacturing customized conveying systems that meet the unique requirements of clients, from small-scale operations to large industrial plants. The company's commitment to quality, innovation, and customer satisfaction has earned it a reputation for delivering reliable and efficient solutions that enhance operational performance and reduce costs.
In summary, cement particle material conveying systems are essential components of modern industrial operations, with their principles and operational characteristics tailored to the specific demands of cement and similar granular materials. The working scenes where these systems are deployed require robust, reliable, and efficient equipment, designed to handle high volumes while maintaining material quality and safety standards. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these solutions, leveraging advanced engineering and manufacturing capabilities to meet the evolving needs of the industry. By understanding the principles and characteristics of cement particle conveying, businesses can optimize their material handling processes, improve productivity, and ensure long-term operational success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top